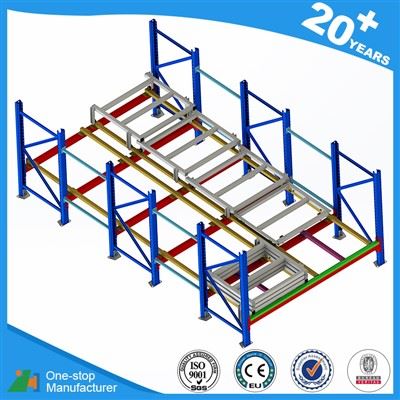
Heavy-Duty Push Back Rack Systems for High-Density Pallet Storage
PrimeBay Heavy Duty Racking Co., Ltd. is a premier manufacturer of custom-engineered push back rack systems. Designed for medium-SKU operations, our push back pallet racking delivers high-density storage while eliminating the need for forklifts to enter storage bays. With storage depth options ranging from 2 to 6 pallets deep, PrimeBay push back racking combines structural rigidity, operational safety, and fast pallet turnover for modern warehousing, cold storage, logistics, and industrial distribution centers worldwide.
Engineered Push Back Racking Products
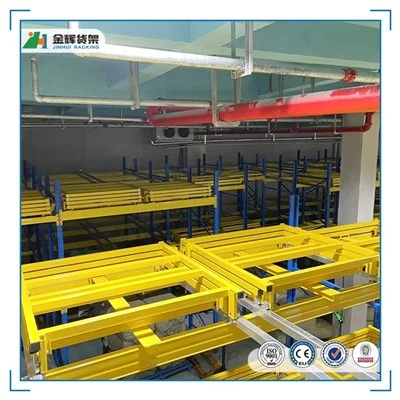
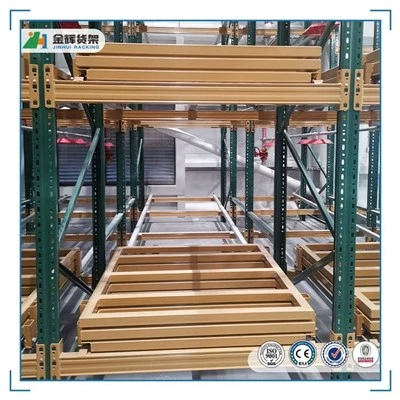
How Push Back Racking Operates
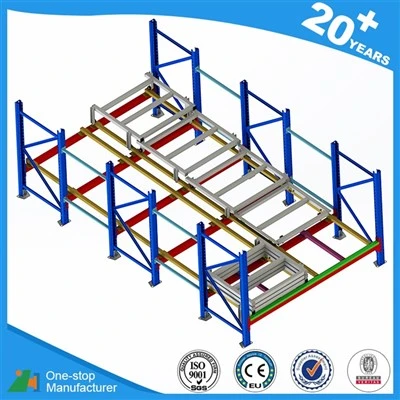
Push back racking utilizes nested steel carts riding on inclined structural rails installed inside structural racking bays. The operating mechanism follows a straightforward gravity-assisted sequence:
- Loading Process: The first pallet is placed on the top nested cart by a standard forklift. When the second pallet is inserted, it gently pushes the first cart back, exposing the second cart beneath. This process continues up to 6 pallets deep.
- Unloading Process (LIFO): When the front pallet is retrieved, gravity gently glides the remaining pallets forward to the picking position at the aisle face, ensuring immediate accessibility.
Technical Specifications & Parameters
Every system manufactured by PrimeBay Heavy Duty Racking Co., Ltd. is engineered to comply with ISO 9001, CE, and FEM structural design standards.
| Technical Item | Specification Parameter |
|---|---|
| System Type | High-Density Push Back Pallet Rack (Gravity-Cart System) |
| Material Grade | Certified Structural Q235B & Q355B High Tensile Steel |
| Storage Depth | 2, 3, 4, 5, or 6 Pallets Deep per Lane |
| Unit Load Capacity | 500 kg to 2,000 kg per pallet position |
| Inventory Principle | LIFO (Last-In, First-Out) |
| Surface Finish | Electrostatic Powder Coating (Epoxy Polyester Finish) |
| Color Options | Customized RAL Colors (RAL 5015 Blue, RAL 2004 Orange, etc.) |
| Certifications | CE Certified, ISO 9001:2015, ISO 14001:2015, TUV Certified |
| Warranty Coverage | 10-Year Structural Integrity Warranty |
Key Advantages for Warehouse Operators
Maximize Storage Density
Increases pallet storage capacity by up to 75% compared to conventional selective pallet racking by reducing required operational aisles.
Faster Operational Throughput
Forklift operators pick and load directly from aisle faces without driving inside rack lanes, drastically cutting transit times.
Reduced Frame Damage
Because forklifts never enter the racking frame structure, risk of forklift impacts and rack maintenance costs are minimized.
Cold Storage Efficiency
Reduces total cubic room size in cold storage and freezer applications, significantly decreasing energy consumption per stored unit.
Target Applications & Industry Use Cases
Push back racking is particularly beneficial for operations with medium SKU counts and multiple pallets per SKU across diverse industrial sectors:
- Food & Beverage Distribution: High-volume, fast-moving consumer goods requiring dense lane storage.
- Cold Storage & Refrigerated Facilities: Maximizing chilled footprint efficiency where energy costs per cubic meter are high.
- 3PL & Third-Party Logistics Centers: Flexible multi-lane storage for dedicated client inventories.
- Manufacturing Staging Areas: Raw materials storage and finished goods buffer storage prior to dispatch.
Quality Assurance & Manufacturing Rigor
At PrimeBay Heavy Duty Racking Co., Ltd., quality is integrated into every stage of production. From raw structural coil selection to precision roll forming, robot welding, and automated powder coating, every batch undergoes mandatory dimensional checks, weld integrity inspections, and load deflection testing.
Before international shipment, our engineers execute full-scale trial assembly on critical cart mechanisms and inclined rail systems to guarantee smooth glide speed, mechanical safety stops, and perfect alignment on-site.