Featured Industrial Racking & Mobile Storage Systems
Explore our CE and ISO-certified heavy-duty warehouse storage machinery, electric stackers, and motorized compact rack solutions optimized for high-density storage applications.
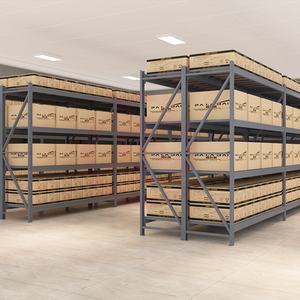
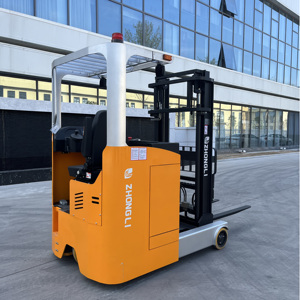
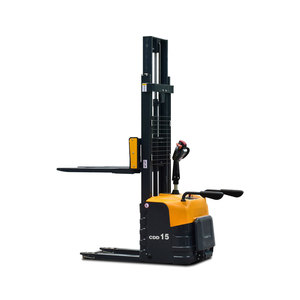
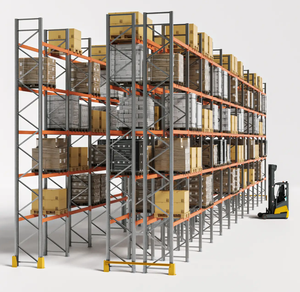
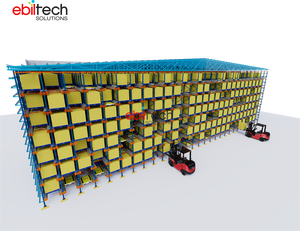
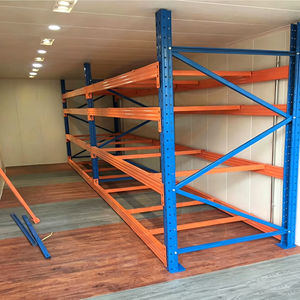
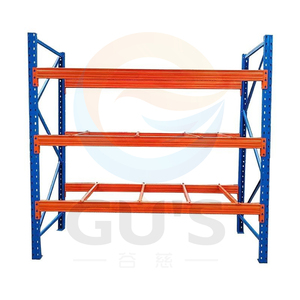
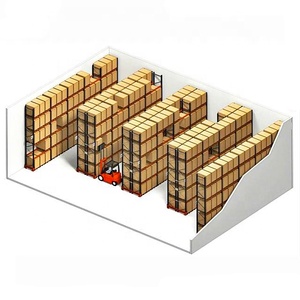
1. Architectural Overview & Los Angeles Industrial Real Estate Context
Southern California, encompassing the Greater Los Angeles Area, the Port of Los Angeles (POLA), the Port of Long Beach (POLB), and the expansive Inland Empire logistics corridor (Ontario, Rancho Cucamonga, City of Industry, Vernon, and Santa Fe Springs), represents the premier international trade gateway of North America. However, industrial warehouse space across LA County and the Inland Empire faces extraordinary economic pressures: average industrial rent rates fluctuate at record highs ($1.50 to $2.20+ NNN per square foot monthly), paired with structural vacancy rates historically constrained below national averages.
For warehouse managers, 3PL providers, cold-chain operators, and industrial logistics directors operating in Los Angeles, expanding floor footprint horizontally is frequently financially unfeasible or physically impossible. CE Certified Motorized Mobile Shelving Systems and Power-Driven Mobile Pallet Racking solve this core spatial challenge by transforming fixed service aisles into a dynamic, mobile layout. By mounting heavy-duty shelving rows onto electric, rail-guided mobile carriages, a motorized system compacts the entire footprint into a single dynamic aisle, unlocking up to 85% to 100% additional storage capacity within existing building shells.
Furthermore, operating within the Greater Los Angeles basin requires absolute compliance with local structural codes. Southern California is designated as a High Seismic Risk Zone (Seismic Design Category D, E, and F under ASCE 7 and the California Building Code / CBC 2022). Custom-engineered mobile racking supplied into the LA market must not only carry international CE structural and electrical certification but must also integrate high-ductility Q355B cold-rolled steel profiles, floor-anchored anti-tipping guide rails, dynamic braking algorithms, and structural seismic FEA (Finite Element Analysis) calculation stamps.
2. Engineering Architecture of Motorized Mobile Shelving Systems
PrimeBay Heavy Duty Racking Co., Ltd. designs and manufactures motorized mobile shelving systems engineered specifically for heavy industrial payloads, archival preservation, high-density parts distribution, and sub-zero refrigerated environments. Below is a detailed technical matrix detailing system components, steel grades, electronic control architecture, and safety protocols:
| System Parameter | Technical Specification & Standard | Engineering Advantage for LA Market |
|---|---|---|
| Structural Material | High-Tensile Cold-Rolled Steel (Q235B / Q355B equivalent to ASTM A1011) | High yield strength engineered to withstand severe seismic sway and heavy dynamic loading. |
| Carriage Load Capacity | 300 kg to 3,000 kg per shelf level; Up to 24,000 kg per mobile base carriage unit | Accommodates everything from high-density automotive spare parts to heavy palletized industrial stock. |
| Drive Mechanism | Direct-gear electric motor drives with Soft-Start / Soft-Stop Frequency Inverters | Eliminates inertia jar and product tipping during carriage acceleration and deceleration. |
| Control & Automation | Siemens / Schneider PLC control panels, Remote RF Controllers, WMS Integration | Allows aisle opening via handheld devices, forklift-mounted terminals, or automated order picking queues. |
| Safety Systems | Infrared optical safety curtains, physical pressure bumpers, emergency stop kill switches | Fully compliant with OSHA and CE Machinery Directive 2006/42/EC for operator protection inside active aisles. |
| Rail System Options | Embedded recessed floor rails or flat surface-mounted guide rails with leveling shims | Recessed rail installations allow smooth, unobstructed forklift and hand truck transit across lanes. |
| Seismic Protections | Floor-anchored anti-tip mechanical locks, floor bolt chemistry, lateral structural cross-bracing | Designed specifically to pass City of Los Angeles Department of Building and Safety (LADBS) structural plan reviews. |
| Surface Finish | Electrostatic Epoxy Powder Coating (60-80μ thickness) or Hot-Dip Galvanized (Cold Room option) | Provides exceptional corrosion resistance, impact resistance, and cleanroom suitability. |
3. Localized Application Scenarios Across Southern California
Our CE-certified motorized mobile shelving systems and heavy-duty adjustable mobile steel racks are tailor-made for the primary industry clusters powering the Greater Los Angeles economic engine:
Located heavily in Vernon, Commerce, and the South Bay, cold storage facilities suffer from exceptionally high refrigeration energy costs (LADWP and SCE industrial utility tariffs). Standard static racking wastes up to 50% of refrigerated cubic volume on empty aisles. Motorized mobile shelving compacts storage density, dramatically reducing the total refrigerated square footage required to store frozen goods, seafood, produce, and pharmaceuticals, delivering massive utility bill savings and rapid CapEx payback.
Southern California’s aerospace and defense corridor—spanning El Segundo, Torrance, Long Beach, and Palmdale—demands zero-error inventory control, ESD-safe environments, and secure access to high-value tooling, turbine components, and avionics hardware. Motorized mobile shelving systems can be equipped with electronic lockable aisles, PIN-code access, and RFID integration, providing strict chain-of-custody security while storing thousands of SKUs in a compact footprint.
In the Inland Empire (Ontario, Fontana, Chino), where massive 3PL and omni-channel e-commerce fulfillment operations manage extreme SKU proliferation, floor space efficiency dictates profit margins. Integrating motorized mobile shelving with warehouse management systems (WMS) allows picking crews to pre-open aisles automatically via batch order pick lists, maximizing cubic storage height while maintaining rapid pick turnarounds.
Serving Burbank, Hollywood, Century City, and Downtown Los Angeles (DTLA), law firms, county government bodies, medical health systems, and film production archives handle millions of historical physical records, film reels, and confidential files. High-density electric mobile shelving offers fire-suppression-compatible overhead clearance, dual-access safety sensors, and optimal archival box compaction.
4. Industry Trends Shaping Southern California Warehousing
Modern material handling in Los Angeles is undergoing a technological shift driven by real estate constraints, environmental legislation, and automation demands:
- 1. Maximizing Vertical Cube Volume Over Expansion: Developers and tenants are opting to utilize clear ceiling heights of 30ft to 40ft by deploying high-bay motorized mobile shelving and radio shuttle clad racking, effectively doubling storage capacity without paying for additional land.
- 2. California Green Building Code (Title 24) & Net-Zero Goals: Compact mobile storage directly lowers building energy consumption for lighting and climate control. By storing double the inventory in half the space, logistics operations significantly reduce their operational carbon footprint.
- 3. Automated Guided Vehicle (AGV) & AMR Integration: Modern motorized mobile carriages are increasingly engineered with open API software interfaces, permitting Autonomous Mobile Robots (AMRs) and automated stacker cranes to communicate with the motorized base, automatically triggering aisle movement during nocturnal replenishment cycles.
- 4. Stringent Local High-Piled Combustible Storage Regulations: Los Angeles Fire Department (LAFD) Regulation 4 and municipal building departments enforce strict high-piled storage permits. Motorized mobile shelving systems can be custom-spaced to ensure full ESFR (Early Suppression, Fast Response) fire sprinkler penetration through upright frames during static periods.
5. Strategic Technology Comparison: Mobile Storage vs. Conventional Systems
To evaluate capital expenditure (CapEx) ROI for your Los Angeles facility, review how motorized mobile shelving compares against traditional storage configurations:
| Storage Architecture | Floor Footprint Utilization | Pallet/SKU Selectivity | Seismic Adaptation | Best Suitable Application |
|---|---|---|---|---|
| Motorized Mobile Shelving / Racking | 85% – 90% (Maximum) | 100% Direct Access (When aisle opens) | Integrated Anti-Tip Rail Locks | High-value land (LA, South Bay), Cold Storage, Parts Archiving |
| Standard Selective Pallet Rack | 35% – 40% (Low) | 100% Direct Access | Standard Anchoring | High-throughput fast-moving items, abundant floor space |
| Drive-In / Drive-Through Rack | 65% – 75% (High) | Poor (LIFO / Bulk SKUs only) | Requires heavy top bracing | Homogeneous bulk goods, low SKU count |
| Automated Storage & Retrieval System (ASRS) | 90% – 95% (Extreme) | 100% Automated Access | Complex Structural Grid | Very high budget, mega-fulfillment centers |
6. Enterprise Strengths & Manufacturing Excellence
As a global leader in warehouse racking engineering since 2006, PrimeBay Heavy Duty Racking Co., Ltd. brings unmatched manufacturing rigor, structural integrity, and international logistics support to buyers across North America:
40,000 m² Automated Manufacturing Plant
Equipped with advanced continuous cold-roll forming lines, robotic welding arms, and automated electrostatic powder coating tunnels ensuring strict dimension tolerances and superior surface finishing.
International Safety & Structural Certifications
Certified strictly under CE (Machinery Directive), ISO 9001 quality management, ISO 14001 environmental management, and TUV Rheinland structural auditing standards.
Custom Engineering & CAD/FEA Support
Our structural engineering team provides complete 2D layout drawings, 3D BIM models, load capacity calculations, and custom upright section design within 24–48 hours of initial inquiry.
Streamlined Export to Port of LA & Long Beach
Decades of ocean shipping experience to Southern California ocean terminals (POLA/POLB). Container loading is optimized to protect powder coating and maximize freight cube capacity.
7. Frequently Asked Questions (FAQ) for Los Angeles Procurement Leads
Optimize Your Los Angeles Facility Footprint Today
Contact our senior racking structural engineers for a complimentary warehouse layout evaluation, 3D CAD design submittal, and direct factory price quote tailored to your Southern California operations.
Contact Our Engineering Team