Engineered Chemical Warehouse Heavy Duty Storage Rack Systems for Hazardous & High-Risk Materials
Storing flammable liquid drums, corrosive acids, toxic reagents, and 1,000L IBC totes demands structural integrity far beyond standard industrial storage. PrimeBay Heavy Duty Racking Co., Ltd. designs, manufactures, and deploys specialized Chemical Warehouse Heavy Duty Storage Rack systems engineered for extreme chemical compatibility, seismic stability, and stringent regulatory compliance (OSHA, NFPA 30, REACH, and CE standards).
Engineering
Why Global Chemical Logistics Leaders Trust PrimeBay Racking Engineering
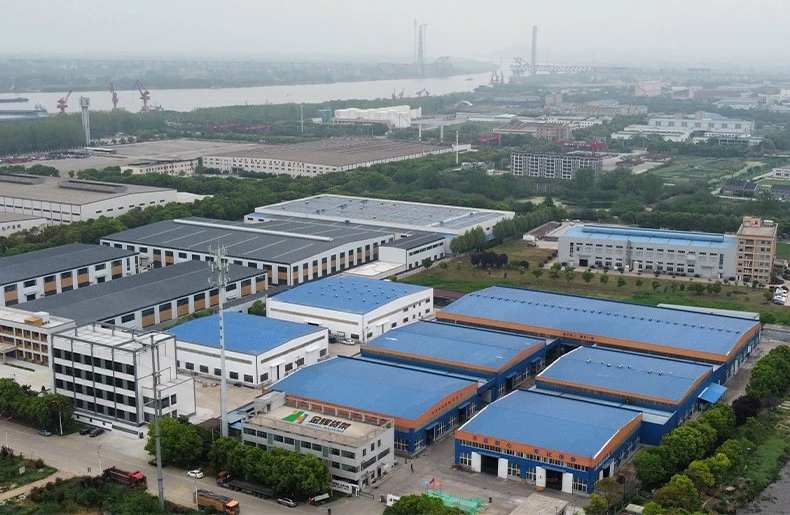
Chemical logistics operates under zero-tolerance rules for structural failure, environmental leakage, and corrosion-induced collapse. Operating from our 40,000 m² state-of-the-art production base in Nanjing, China, PrimeBay Heavy Duty Racking Co., Ltd. brings over two decades of metallurgical precision and structural design expertise to chemical enterprise supply chains.
Our Chemical Warehouse Heavy Duty Storage Rack solutions utilize high-tensile structural steel (Q235B & Q355B grades) rolled into custom upright profiles capable of supporting static loads exceeding 4,500 kg per beam level. Unlike standard commercial storage, every chemical racking structure undergoes advanced Finite Element Analysis (FEA) to verify load distribution during seismic events, thermal expansion, and liquid surge dynamics.
- Multi-stage anti-corrosion treatments (Electrostatic Epoxy & Hot-Dip Galvanizing)
- Integrated secondary spill containment basins and heavy galvanized mesh grating
- Full compliance with NFPA 30 Flammable Liquid Codes and OSHA storage guidelines
- Complete OEM/ODM customization for cold storage, cleanrooms & hazardous zones
Recommended Heavy Duty Chemical Warehouse Storage Racking Systems
Chemical products range from volatile organic solvents to dense raw material resins. Select the engineered storage methodology tailored to your warehouse SKU density, turn rates, and hazmat segregation guidelines.
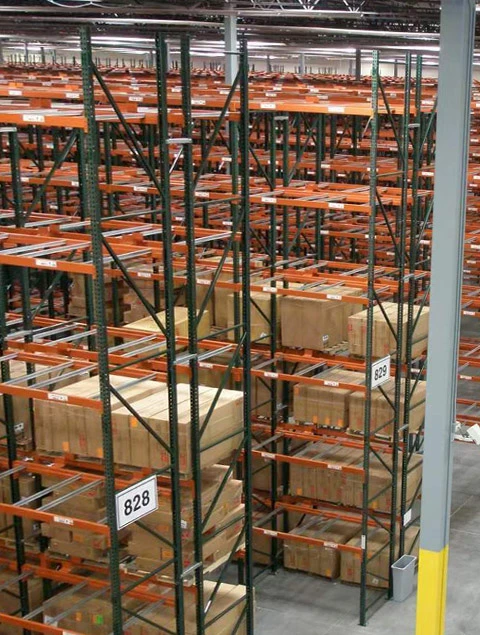
Selective Chemical Pallet Racking
Provides 100% immediate access to every chemical IBC tote, drum, or box. Outfitted with spill-containment trays and anti-acid powder coating for volatile liquid logistics.
Send an Inquiry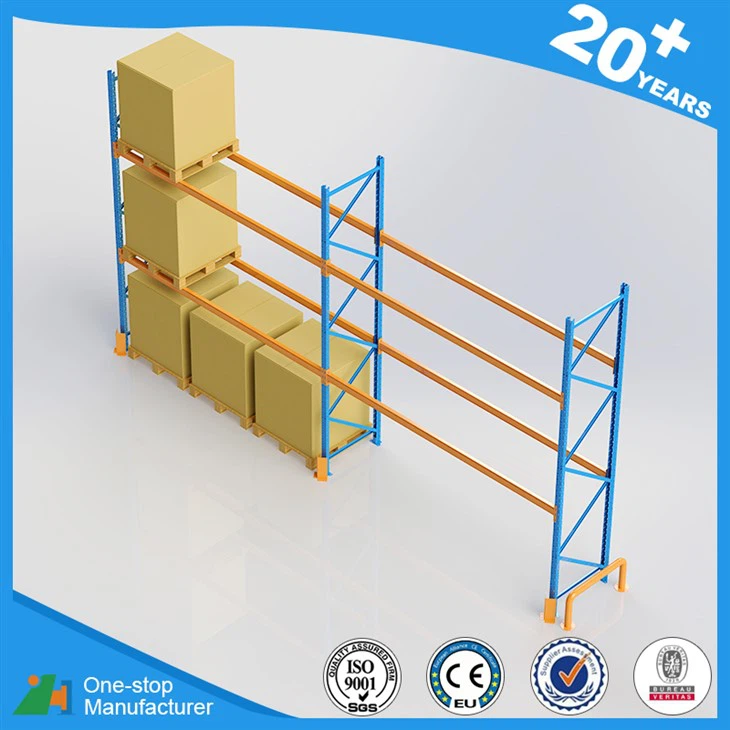
Heavy Duty Chemical Drum Racking
IBC Container Heavy Duty Racking
Galvanized Decking Spill Racking
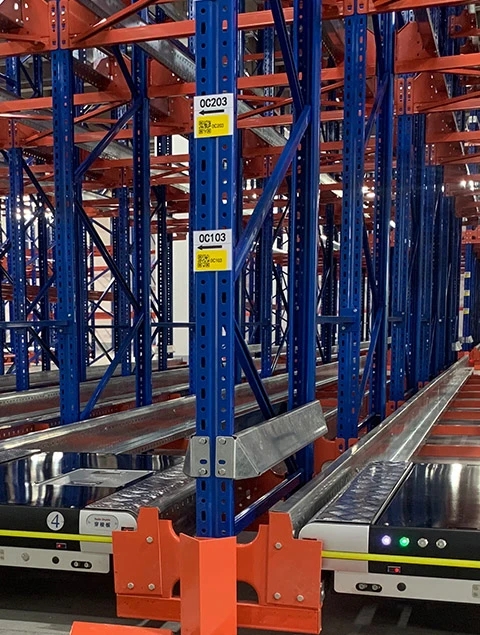
Radio Shuttle Chemical Racking
High-density automated storage featuring explosion-proof (ATEX zone certified) shuttles. Eliminates forklift entry into hazardous chemical channels.
Send an Inquiry
ATEX Radio Shuttle Storage Rack
4-Way Chemical Shuttle System
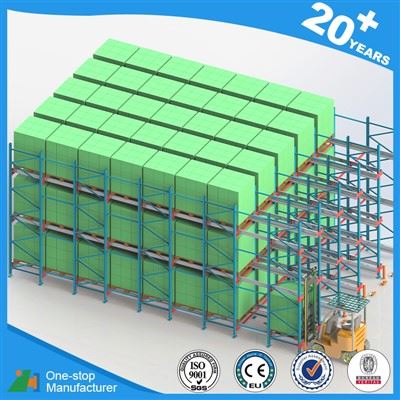
High-Density Chemical Storage
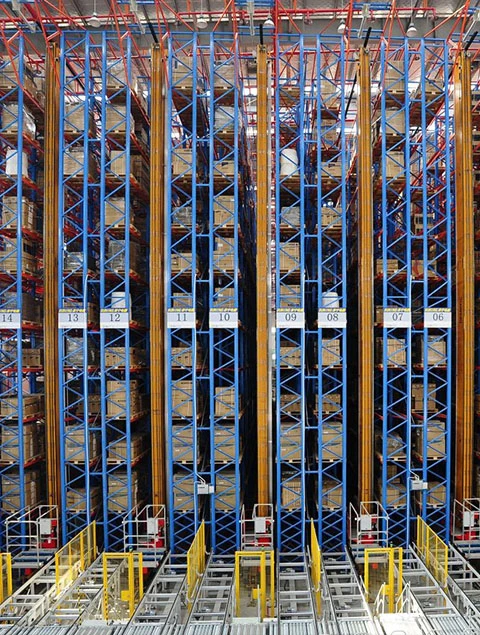
Push Back Chemical Storage Racks
2 to 5 pallet-deep nested carts on inclined rails. Offers high volumetric efficiency with LIFO access for homogeneous chemical batches.
Send an Inquiry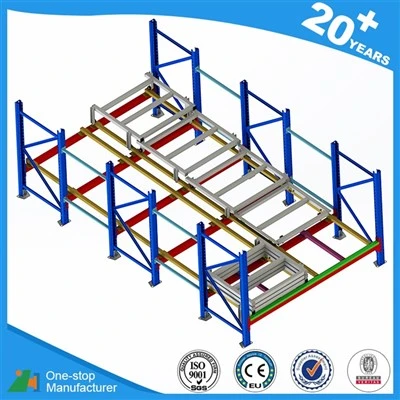
Multi-Cart Chemical Push Back
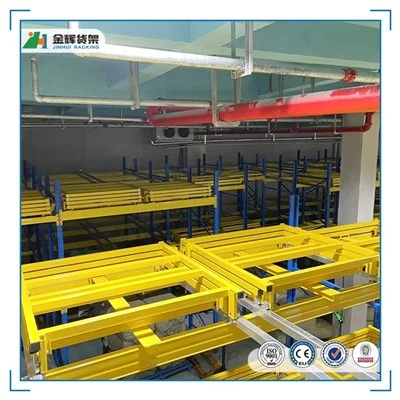
Heavy Duty Hazmat Push Back
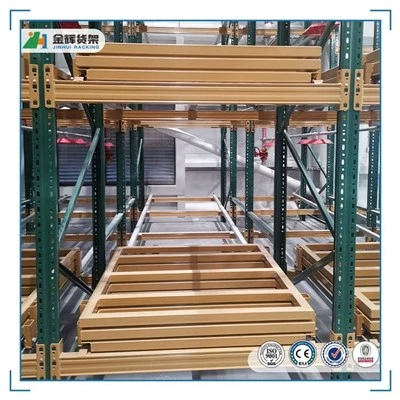
Sealed Cart Push Back Racking
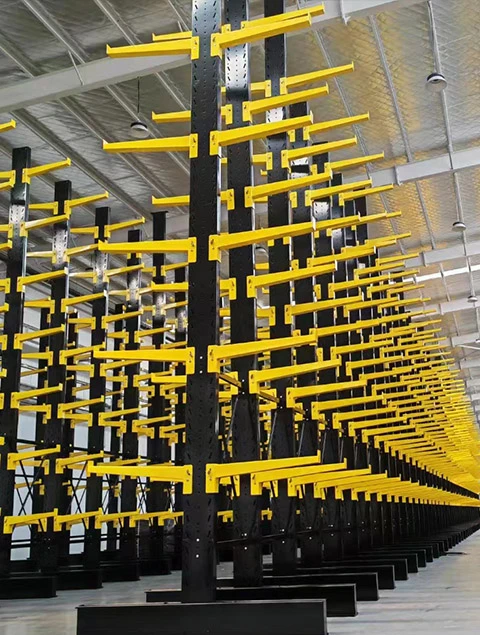
Drive-In / Drive-Through Chemical Racks
Ideal for large, uniform lots of non-volatile chemical raw materials. Maximizes floor space utilization up to 85% by eliminating aisles.
Send an Inquiry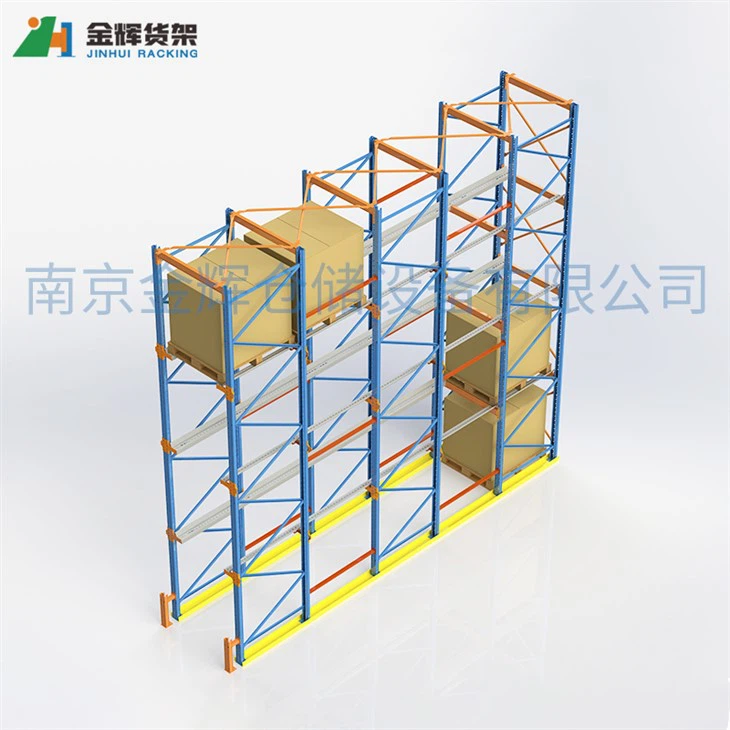
Bulk Chemical Drive-In Rack
Drive-Through FIFO Chemical Rack
Reinforced Chemical Drive-In
Chemical Warehouse ASRS Systems
Fully automated stacker cranes and software-driven high-bay racking systems designed to isolate human operators from hazardous chemical storage zones.
Send an Inquiry
High-Bay Chemical ASRS Rack
Chemical VNA High-Bay Rack
Automated Hazmat Storage Rack
Engineering Advancements in Chemical Heavy Duty Storage Racks
Modern chemical processing and third-party hazmat logistics require advanced metallurgy and protective coatings to withstand severe acid vapors, humidity, and chemical spills.
Explore core structural and anti-corrosion innovations engineered by PrimeBay Heavy Duty Racking Co., Ltd.:
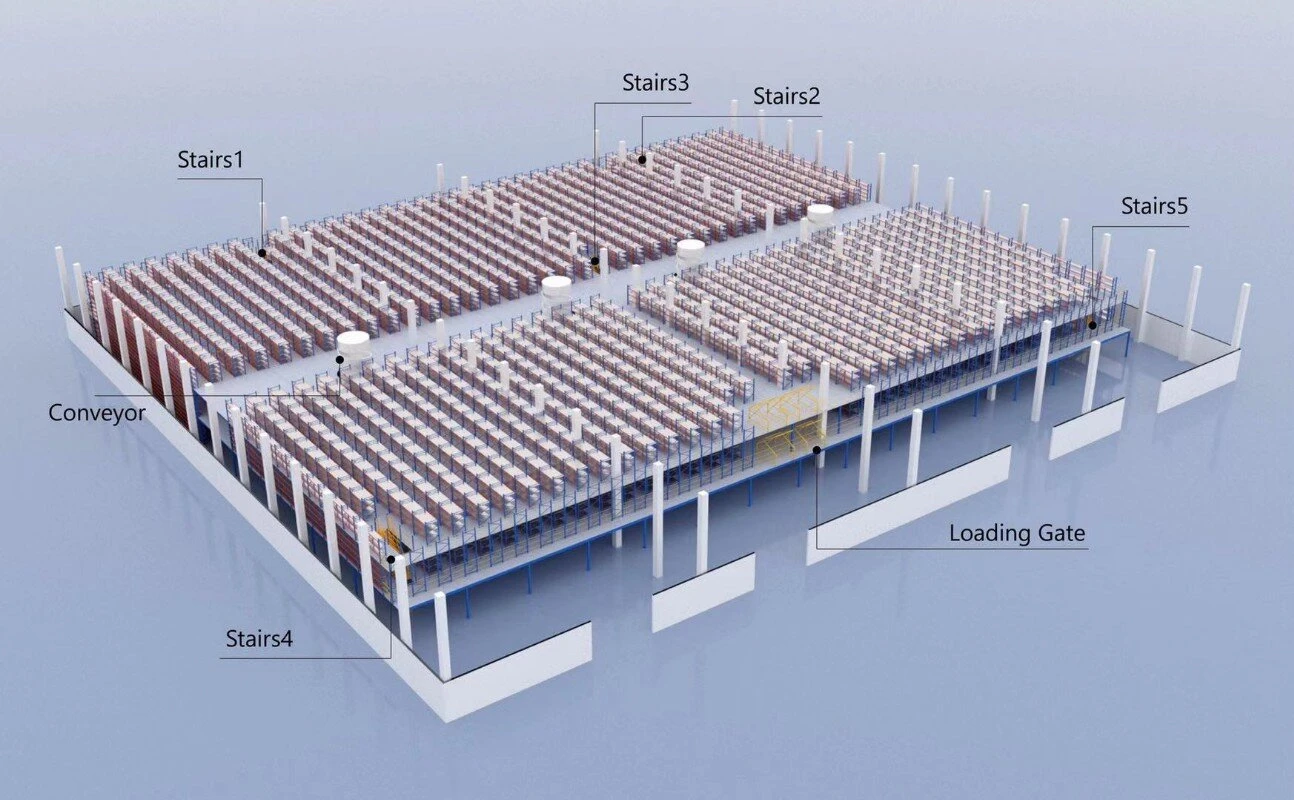
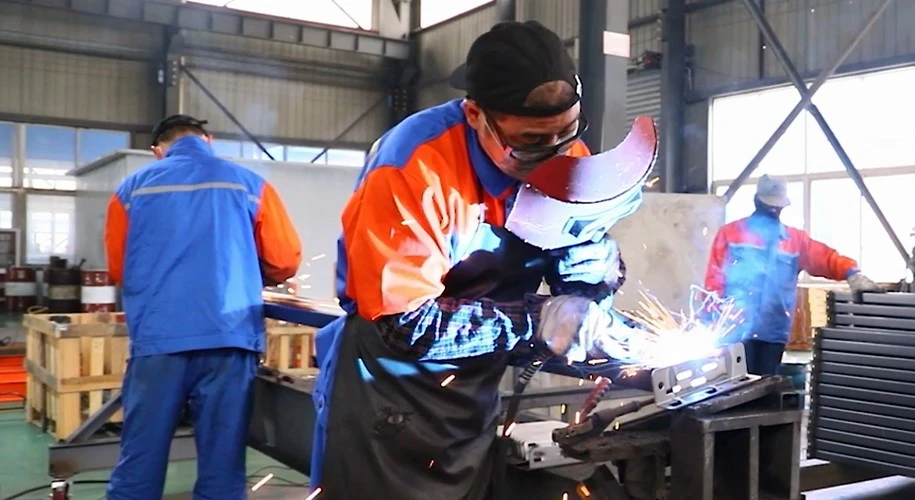
Future Procurement Trends for Chemical Storage Systems (2026–2030)
Global procurement teams in multinational chemical enterprises are shifting priorities toward automated hazmat handling, real-time safety telemetry, and zero-emission manufacturing compliance.
1. Human-Free Hazmat Automation
Supply chain leaders are upgrading from manual forklift selective racks to ATEX-certified AS/RS and Four-Way Shuttle systems. Automating storage in volatile chemical spaces drastically reduces operator exposure to toxic fumes and risk of accidental collisions.
2. IoT Telemetry & Rack Health Sensors
Modern chemical warehouse heavy duty storage racks are rapidly integrating embedded load-cell sensors and tilt indicators. These IoT modules monitor beam deflections, micro-corrosion, and structural shifts caused by thermal fluctuations in real time.
3. Modular Environmental Containment
Rather than relying solely on floor-level sump pits, chemical procurement tenders now mandate modular rack-level containment. Spill trays equipped with chemical-neutralizing drainage pipes allow rapid isolation of hazardous leaks before contamination spreads.
4. Decarbonized Steel & Eco-Coatings
With Scope 3 carbon reporting enforcement across Europe and North America, chemical buyers favor racking manufacturers utilizing green steel and volatile-organic-compound-free (VOC-free) thermosetting powder coatings.
Chemical Storage System Technical Comparison
Evaluate load capacities, chemical environment suitabilities, and containment options before finalizing your warehouse racking tender.
| Chemical Storage System | Max Beam Load / Level | Corrosion Resistance Rating | Hazmat Class Compatibility | Key Protection Accessories |
|---|---|---|---|---|
| Selective Chemical Pallet Rack | Up to 4,500 kg | High (C4 / C5 HDG) | Class 3 Flammables, Class 8 Corrosives, Class 6 Toxics | Sump trays, mesh decking, upright bull-nose protectors |
| ATEX Radio Shuttle Racking | 1,500 kg per pallet | Medium-High (Epoxy + ATEX) | Class 3 Flammables, Bulk Raw Resins, Agrochemicals | Explosion-proof batteries, optical lane sensors, guidance rails |
| Chemical Push Back Rack | 1,200 kg per cart | Medium (Polyurethane Coated) | Non-volatile liquid drums, agricultural additives | Nested stainless carts, gravity tilt stops, side retainers |
| Chemical Drive-In Storage Rack | 1,500 kg per position | High (Galvanized Rails) | Bulk homogenous chemical powders, raw polymers | Floor-anchored guide rails, reinforced top bracing |
| Automated Chemical AS/RS Rack | Up to 2,000 kg per position | Extreme (Custom Stainless Options) | Class 3, Class 4, Class 5.1 Oxidizers, Class 8 Corrosives | Automatic fire-suppression nozzles, nitrogen purging ducts |
*Structural specifications are engineered based on dynamic load requirements, seismic zone multipliers, and chemical MSDS data provided during design review.
Chemical Warehouse Heavy Duty Storage Rack FAQ
Direct technical answers to critical questions asked by chemical warehouse operators, environmental health & safety (EHS) managers, and global supply chain directors.
What specific safety standards apply to a Chemical Warehouse Heavy Duty Storage Rack?
How do I select between Hot-Dip Galvanizing (HDG) and Electrostatic Epoxy Powder Coating for chemical storage?
What secondary spill containment mechanisms can be integrated into heavy duty chemical pallet racks?
How does liquid weight sloshing affect heavy-duty chemical rack design during seismic events?
Can automated Radio Shuttle racking systems operate safely in explosion-proof (ATEX) chemical environments?
What documentation and quality certifications does PrimeBay supply with chemical racking orders?
Request a Custom Chemical Racking Layout & FEA Load Calculation
Optimizing a chemical warehouse requires precise balancing of volumetric density, hazard isolation, and regulatory compliance. Contact PrimeBay Heavy Duty Racking Co., Ltd. today to receive a complimentary CAD floorplan layout, technical tender document, and direct factory price quote from our senior engineering team.