Featured Warehouse Pallet Racking Systems
Standard and custom-engineered pallet racking solutions optimized for heavy industrial drums, liquid containers, and high-density warehouse operations.
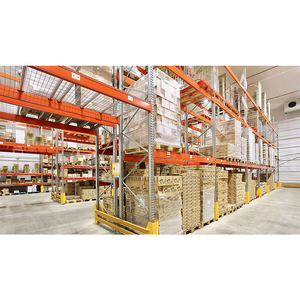
Very Narrow Aisle Storage System Reach Truck Warehouse Solution Space Saving VNA Rack
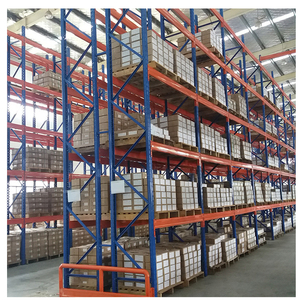
Heavy Duty Rack Storage Industrial Selective Assembly Pallet Use Rack Warehouse Storage Pallet Rack
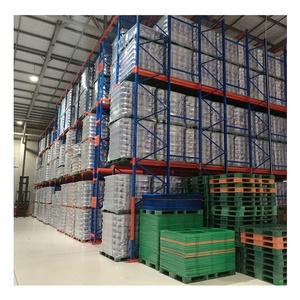
Warehouse Heavy Duty Storage FiFo Drive in Pallet Racking System
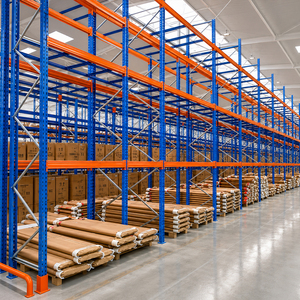
Warehouse Storage Rack System High Density Porta Pallet 1000kg Q235B Cold Rolled Steel Heavy Duty Pallet Rack Warehouse
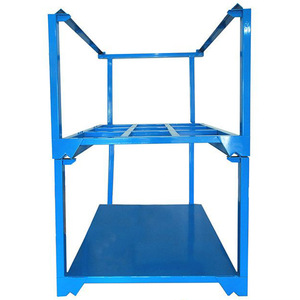
CASE CARTER OEM Warehouse Stack Foldable Portable Vertical Steel Pallet Frame Nestainer Storage Rack System
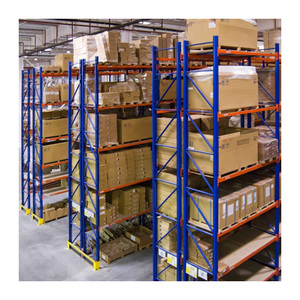
China Rack Factory Manufacturer Custom Warehouse Heavy Duty Pallet Racking Storage Shelf
Wholesale Heavy Duty Steel Structure Metal Frame Warehouse Storage Shelving Industry High-bay Pallet Modular Flow Racking System
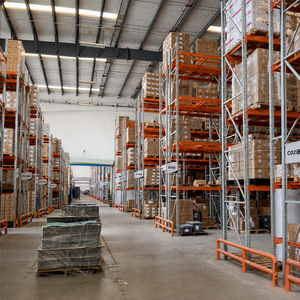
Heavy Duty Pallet Rack Back to Back Double Entry Row with Safety Guardrails for E-commerce Fulfillment Center Storage
Engineering Excellence in Industrial Heavy Drum Storage Pallet Racking
Storing 55-gallon (210-liter) steel and plastic chemical drums presents complex structural, environmental, and operational logistics challenges. Unlike standard boxed merchandise, liquid-filled drums exert high dynamic point loads, pose severe spill hazards, and demand stringent compliance with environmental containment standards (OSHA, EPA 40 CFR 264.175, and NFPA 30).
As China’s leading industrial pallet racking manufacturer, PrimeBay Heavy Duty Racking Co., Ltd. produces structural steel drum storage systems engineered explicitly for high unit load weights (up to 4,000 kg per beam level). Utilizing premium cold-rolled Q235B and Q355B structural steel, our rack profiles deliver unyielding structural integrity, localized impact resistance, and customized spill containment sumps to protect your facility from hazardous material runoff.
Selecting the Right Drum Racking Configuration
Compare structural load limits, selectivity performance, and containment capabilities across various industrial drum racking architectures.
| Racking Architecture | Load Capacity (Per Tier) | Pallet / Drum Selectivity | Primary Storage Method | Spill Containment Level | Ideal Application |
|---|---|---|---|---|---|
| Horizontal Drum Cradle Racking | 1,500 kg – 3,000 kg | 100% Direct Access | Horizontal Cradle Laydown | Integrated Base Sump Deck | Chemical dispensing, oil drum tapping & sampling |
| Selective Pallet Drum Racking | 2,000 kg – 4,000 kg | 100% Direct Access | Vertical Palletized (4 drums/pallet) | Removable Galvanized Sump Trays | High-SKU distribution, chemical raw material storage |
| Radio Shuttle Chemical Racking | 1,500 kg per shuttle load | High Density (Lane-based) | Automated Deep Lane Palletized | Integrated Floor Spill Channels | Cold storage, high-volume bulk lubricants & solvents |
| VNA High-Bay Drum Racking | 2,500 kg – 4,500 kg | 100% Direct Access | Vertical Palletized via Turret Truck | Sub-floor Drainage Basins | Space-constrained high-ceiling chemical fulfillment |
| Nestainer & Portable Stack Racks | 1,000 kg – 2,000 kg | Block Stacking (Flexibility) | Modular Nestable Steel Frames | Optional Modular Drip Pans | Seasonal chemical storage, liquid container staging |
Why Leading Global Chemical & Logistics Companies Partner With Us
From raw material selection to structural Finite Element Analysis (FEA), PrimeBay delivers certified manufacturing consistency and robust global exporter services.
Certified Quality & International Standards
Our complete production line complies strictly with ISO 9001 quality management, ISO 14001 environmental management, CE European structural standards, and TUV Rheinland auditing. Every upright frame and beam section is load-tested under FEM 10.2.02 and EN 15512 guidelines.
40,000 m² Advanced Manufacturing Base
Located in Nanjing, Jiangsu, our facility houses continuous automatic cold-roll forming lines, high-precision robotic welding stations, and an automated electrostatic powder-coating line capable of producing custom chemical-resistant finishes (zinc-rich primer + heavy epoxy powder).
In-House Structural Engineering & Custom OEM/ODM
We do not just ship off-the-shelf components. Our senior engineering team conducts CAD layout optimization, FEA stress simulation, and floor load distribution analysis tailored to your specific warehouse height, slab capacity, and forklift specifications.
10-Year Structural Warranty & Full Documentation
Every export shipment includes comprehensive installation manuals, structural calculation reports, anchor bolt layouts, and official load capacity signage. We provide an industry-leading 10-year structural warranty across all static racking components.
Integrated Hazardous Secondary Containment
All drum racking profiles can be integrated with heavy-duty hot-dip galvanized spill containment trays, leak-diverting sumps, and static grounding clips to comply strictly with local environmental protection regulations and hazardous materials handling codes.
Global Export & Project Logistics Reliability
With ongoing projects in over 85 countries—spanning Europe, North America, Southeast Asia, and the Middle East—our export team guarantees professional sea-freight packaging, steel bundle protection, container load optimization, and rapid customs documentation processing.
Future Procurement Trends in Industrial Drum Racking (2025–2030)
Anticipating regulatory changes, automation adoption, and sustainability benchmarks in global chemical and bulk liquid warehouse procurement.
Integration of Automated Storage & Retrieval (ASRS) for Liquid Drums
Traditional manual forklift handling of 55-gallon drums is increasingly giving way to fully automated stacker cranes and Heavy-Duty Four-Way Pallet Shuttles. As chemical facilities face labor constraints and safety risks, procurement managers are prioritizing racking designs configured with high-precision guide rails, photoelectric sensor cutouts, and automated drum pick-and-place interfaces. Racking structures must maintain tight manufacturing tolerances (±0.5mm) to support flawless automated positioning.
Mandatory ESG & Zero-Spill Compliance Regulations
Environmental, Social, and Governance (ESG) mandates are transforming industrial storage requirements globally. Future procurement specs demand that racking suppliers integrate 100% liquid secondary containment capacity (calculating 110% of the largest drum volume or 25% of total stored liquid volume). Buyers are turning to factories capable of delivering modular, leak-proof galvanized sump pans directly integrated beneath the structural racking base levels.
High-Yield Cold-Rolled Steels (Q355B & Ultra-High Strength Alloys)
To reduce overall warehouse floor space footprints, global buyers are specifying higher yield strength steel profiles (such as Q355B and high-grade cold-rolled coils) rather than standard commercial grade steel. This enables thinner wall profiles (2.0mm–3.0mm) without compromising load-bearing limits, effectively reducing steel raw material consumption, lowering international shipping weights, and decreasing overall freight costs.
Modular & Flexible Seismic-Resistant Frameworks
With increasing global focus on earthquake preparedness and warehouse structural safety, international procurement tenders demand racking systems certified for high seismic zones (according to ANSI MH16.1 and Eurocode EN 1998-1). Modern drum racks feature heavy-duty base plates, enlarged expansion anchor footprints, stiffened diagonal bracing frames, and modular bolt-less beam adjustment slots for fast post-event re-configuration.
Key Technological Trends in Drum Storage Equipment Manufacturing
Discover how advanced materials engineering, smart IoT monitoring, and robotic production are re-defining high-density drum pallet storage.
IoT Smart Sensor Leak Detection Integration
Modern drum racking designs are incorporating smart telemetry channels within structural beam profiles. Integrated optical liquid sensors and load-cell weight transducers detect subtle drum punctures or weight shifts instantly, triggering automated alarms to prevent cataclysmic chemical spills and structural overload.
Duplex Surface Finishes for Corrosive Atmospheres
Chemical drum storage environments subject steel to corrosive acid fumes and solvent vapors. Advanced manufacturing leverages duplex coating technology: hot-dip galvanizing per ISO 1461 followed by electrostatic application of chemical-resistant thermosetting epoxy powder coatings, delivering superior salt-spray corrosion resistance exceeding 1,000 hours.
Gravity-Assisted Drum Flow & Polyurethane Rollers
Next-generation horizontal drum storage utilizes dynamic pallet flow rails fitted with specialized polyurethane-coated steel rollers. Drums roll smoothly under gravity control with magnetic speed controllers, ensuring strict First-In, First-Out (FIFO) rotation for time-sensitive chemical compounds and lubricants.
Frequently Asked Questions by B2B Procurement Officers
Expert insights on engineering compliance, load calculations, shipping logistics, and custom OEM drum rack specifications.
1. What structural specifications are critical when calculating load capacity for 55-gallon drum racking?
Calculating load capacities for industrial drum storage requires factoring in liquid density rather than standard solid package weight. A standard 55-gallon (210L) drum filled with heavy liquid chemicals can weigh between 220 kg and 380 kg. When 4 drums are loaded onto a single wooden or steel pallet, the total unit load reaches 880 kg – 1,520 kg per pallet position.
At PrimeBay, our structural engineers calculate beam deflection limits based on a maximum ratio of L/200 under full static load. We specify cold-rolled Q235B or Q355B steel box beams with 4-hook or 5-hook connector connectors, reinforced safety locking pins, and heavy-duty upright frames (pitch 75mm or 50mm) to eliminate frame buckling risk under uneven liquid dynamic movement.
2. How does PrimeBay handle secondary spill containment compliance (EPA / OSHA)?
Compliance with EPA 40 CFR 264.175 and OSHA regulations requires liquid containment systems capable of holding at least 10% of the total volume of all stored containers, or 100% of the volume of the largest container, whichever is greater.
We engineer custom leak-proof secondary containment sumps manufactured from 2.5mm–3.0mm heavy gauge steel sheets with continuous robotic seam welding. These sumps are hot-dip galvanized or finished with liquid-resistant epoxy coatings and placed directly under racking bays. Removable steel mesh grates sit above the sumps, allowing spilled liquids to drain safely away from warehouse personnel and material handling equipment.
3. Can you design customized drum racking solutions according to my CAD warehouse layout?
Yes, absolutely. Every industrial storage project begins with a free engineering consultation. You simply provide your warehouse CAD floor plan (or a dimensional sketch detailing building clear height, column spacing, floor slab slab load capacity, and forklift turning radii).
Our engineering department utilizes AutoCAD, 3D SolidWorks, and structural calculation software to generate optimized bay layouts, bill of materials (BOM), and FEA stress reports. We provide complete 2D layout drawings and 3D renderings for customer approval before starting raw material rolling.
4. What is the difference between horizontal drum cradle racking and vertical pallet drum racking?
Horizontal Drum Cradle Racking: Drums are placed horizontally on specialized steel cradles or chocks. This orientation allows operators to install dispensing spigots or taps directly into the drum head for easy liquid decanting and sampling. It offers 100% direct access to every single drum but requires manual or specialized drum handler attachment handling.
Vertical Pallet Drum Racking: Drums stand upright, typically 4 drums per pallet, and are stored using standard heavy-duty selective pallet racking beams fitted with wire mesh decking or support bars. This layout maximizes pallet storage density, speeds up forklift loading cycles, and is best suited for bulk storage and raw material staging where liquid dispensing inside the rack is not required.
5. What international quality certifications do your drum racking products carry?
PrimeBay Heavy Duty Racking Co., Ltd. maintains rigorous international quality and safety certifications. Our factory and manufacturing processes are certified to ISO 9001 (Quality Management System) and ISO 14001 (Environmental Management System). Our structural pallet racking products hold CE compliance certificates for European market entry and undergo third-party auditing and structural load testing by TUV Rheinland.
6. What anti-corrosion surface treatments are available for chemical drum storage?
We offer three primary surface treatment options based on your facility's operational environment:
- Electrostatic Thermosetting Powder Coating: Standard durable finish (60–80 microns thick) ideal for non-corrosive indoor warehouse environments.
- Heavy Epoxy Chemical-Resistant Coating: Formulated specifically to resist chemical splatters, solvent fumes, acidic washdowns, and alkalis.
- Hot-Dip Galvanizing (HDG per ISO 1461): The ultimate anti-corrosion protection. Steel components are immersed in molten zinc at 450°C, producing a zinc coating layer (65–85 microns thick) that protects against outdoor weather exposure, extreme humidity, and aggressive chemical atmospheres for decades.
7. What is your standard production lead time and sea freight export packaging?
Standard manufacturing lead time is 15 to 25 calendar days from formal order confirmation and deposit receipt, depending on total project tonnage. For custom OEM roll profiles or hot-dip galvanizing orders, lead times range between 25 and 35 days.
All export racking components are bundled using automated steel banding, wrapped in protective plastic moisture-barrier film, and fitted with heavy wooden corner protectors. Base frames and beams are organized logically inside 20GP or 40HQ containers to facilitate fast forklift unloading upon destination port arrival.
8. What warranty and post-purchase engineering support does PrimeBay provide?
We provide a comprehensive 10-year structural warranty covering structural steel integrity against manufacturing defects, weld failures, and material degradation under normal design load conditions. Every project is accompanied by detailed assembly manuals, 3D exploded structural diagrams, bolt torque spec sheets, and official safe-load signs for display on racking end frames.
Ready to Optimize Your Chemical & Drum Storage System?
Partner with China's leading heavy-duty pallet racking exporter. Send us your floor plan or engineering requirements today for a fast, technical layout proposal and competitive factory quotation.