Engineered Heavy-Duty Storage Systems
Selected industrial pallet racks, drive-in structures, multi-tier platforms, and radio shuttle solutions built to ISO 9001 and CE certifications.
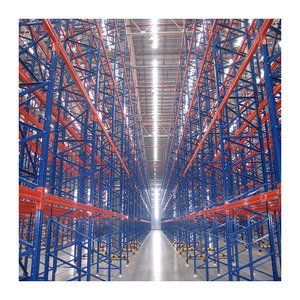
Mracking Heavy Duty Industrial Palletized Racking (1000-4000kg Capacity)
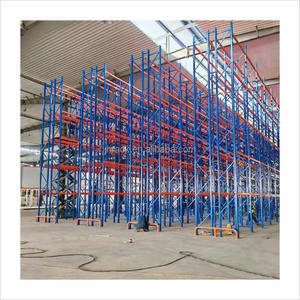
5 Layer Heavy Duty Very Narrow Aisle (VNA) Warehouse Racking for Inventory Management
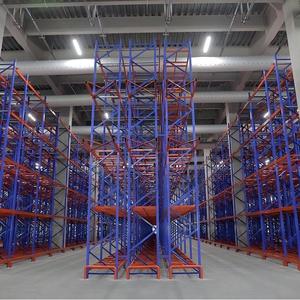
Stackable Double Deep Beam Heavy Duty Steel Pallet Racking with Upright Protectors
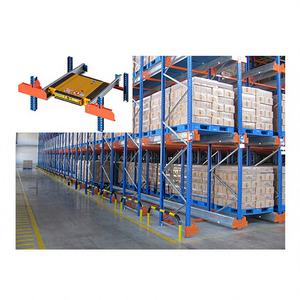
Automated High Capacity Radio Pallet Shuttle Rack System for Heavy Duty Storage
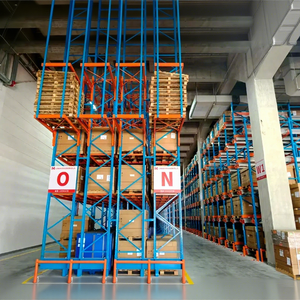
Maxrac Double Deep Pallet Racking System Multi-Layer Boltless Corrosion Protection
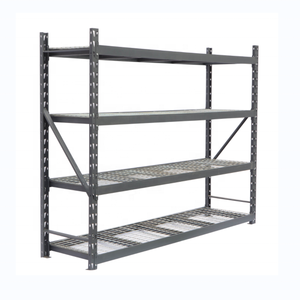
KINDE Steel Heavy Duty Industrial Warehouse Storage Pallet Racking (800kg/Level)
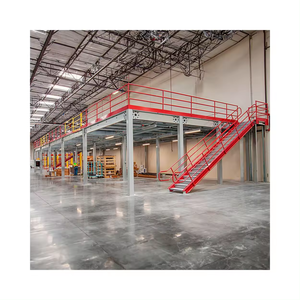
HUAWU 1000kg/sqm Industrial Mezzanine Floor Platform Rack Q235 Steel Structure
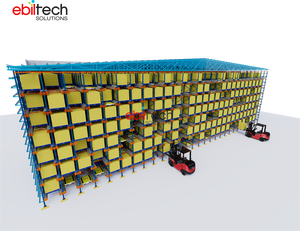
EBILTECH CE Certified Two-Way Shuttle Clad Racking for Deep Lane Storage
Global Industrial Storage Racking Ecosystem in 2026/2027
Modern global logistics, rapid e-commerce expansion, and cold chain industrial upgrades have transformed warehouse storage from simple static framing into a highly engineered, stress-analyzed asset category. Choosing the right heavy-duty pallet racking supplier directly affects warehouse operational efficiency, structural safety, payload utilization, and long-term capital expenditure (CAPEX).
This comprehensive procurement report evaluates the Top 10 Pallet Racking Suppliers & Exporters, providing industrial engineers, project contractors, 3PL logistics executives, and procurement heads with actionable benchmarking criteria. We analyze manufacturing precision, steel grade standards (such as Q235B, Q355B, and SS400 structural steel), structural load compliance (FEM 10.2.02, RMI, ANSI MH16.1), dynamic surface finishing, and global export resilience.
Information Gain Key Takeaway: Selecting an enterprise rack manufacturer should never be based solely on per-kilogram raw steel prices. Advanced engineering parameters—such as cold-roll profile beam section modulus, upright column pitch adjustability (50mm/75mm), epoxy powder coating thickness (60-80μm), and finite element analysis (FEA)—determine structural safety and long-term durability under heavy usage.
Top 10 Pallet Racking Suppliers & Exporters (2026/2027 Ranking)
Our engineering research team evaluated hundreds of storage equipment manufacturers worldwide based on five core metrics: structural design compliance, production automation level, structural steel tensile quality, export certification integrity, and OEM/ODM custom layout capabilities.
1. PrimeBay Heavy Duty Racking Co., Ltd.
Headquarters: Nanjing, Jiangsu, China
Core Strengths: 20+ years of continuous manufacturing expertise, 40,000m² automated manufacturing facility, export footprint across 85+ countries. Fully certified with CE, ISO 9001, ISO 14001, and TUV.
Specialization: Custom heavy-duty pallet racks (1000–4000kg/level), 4D radio shuttle automated systems, structural mezzanine floor platforms, and OEM/ODM engineering integration.
2. SSI Schaefer Group
Headquarters: Neunkirchen, Germany
Core Strengths: Worldwide provider of turnkey logistics, automated high-bay warehouses, tote systems, and modular pallet racking structures.
Specialization: Fully automated storage and retrieval systems (ASRS), shuttle software platforms, and cold-store infrastructure.
3. Stow Racking Systems
Headquarters: Spiere-Helkijn, Belgium
Core Strengths: Massive pan-European manufacturing footprint, advanced research into 3D automated shuttles (Movia, Atlas series), and high structural reliability.
Specialization: Drive-in pallet systems, cantilever racks for heavy industrial stock, and automated shuttle framing.
4. Mecalux, S.A.
Headquarters: Barcelona, Spain / Chicago, USA
Core Strengths: Extensive global sales network across 70+ countries, multi-location roll-forming plants, integrated warehouse management software (Easy WMS).
Specialization: Selective pallet racking, push-back dynamic cart racking, VNA turret truck racking layouts.
5. Jungheinrich Logistics Systems
Headquarters: Hamburg, Germany
Core Strengths: Seamless combination of industrial material handling equipment (forklifts) with tailored structural pallet racking platforms.
Specialization: Very Narrow Aisle (VNA) system optimization, automated AGV integration, pallet flow racking.
6. Dexion Storage Solutions
Headquarters: Brokerud, Norway / International
Core Strengths: Decades of historical innovation in slotted angle profiles and adjustable beam connection systems across APAC and Europe.
Specialization: Mobile heavy-duty pallet racking (MOVO), archive shelving, multi-tier industrial racking.
7. Unarco Material Handling, Inc.
Headquarters: Springfield, Tennessee, USA
Core Strengths: Leading North American manufacturer focusing heavily on RMI safety standards, severe impact-resistant upright column guards.
Specialization: T-Bolt boltless rack systems, structural steel rack columns, gravity flow systems.
8. Frazier Industrial Company
Headquarters: Long Valley, New Jersey, USA
Core Strengths: Pioneer in structural steel hot-rolled channel pallet racking systems, renowned for high impact resistance.
Specialization: Hot-rolled structural steel racks, heavy beverage distribution storage, high-impact drive-in systems.
9. Daifuku Co., Ltd.
Headquarters: Osaka, Japan
Core Strengths: Global leader in automated material handling solutions, ultra-high reliability AS/RS rack framing engineering.
Specialization: High-bay AS/RS rack buildings, cleanroom storage systems, automotive manufacturing buffer systems.
10. Elite Storage Solutions
Headquarters: Monroe, Georgia, USA
Core Strengths: Specialist manufacturer of high-density warehouse storage systems, engineered drive-in, drive-through, and push-back configurations.
Specialization: Push-back cart systems, heavy-duty pallet flow lanes, dynamic grocery supply warehouse racks.
Next-Generation Product Development & Procurement Trends (2026-2030)
The industrial storage industry is undergoing a structural shift driven by automated material handling, labor shortages, rising land acquisition costs, and stringent ESG sustainability mandates. Modern procurement managers are looking beyond standard steel beams to invest in future-proof racking technologies.
1. The Transition from Static Storage to Autonomous 4D Shuttle Systems
High-density storage is moving rapidly away from traditional forklift-entered drive-in racks toward automated Radio Shuttle and Four-Way (4D) Pallet Shuttle systems. By decoupling forklift trucks from the racking lanes, storage density increases by up to 70-80% compared to selective rack layouts. The automated shuttle travels along specialized internal guide rails to store and retrieve pallets rapidly, controlled via wireless remote or Warehouse Execution Systems (WES).
2. High-Strength Q355B Steel & Cold-Formed Structural Optimization
To reduce overall warehouse deadload while improving load capacity, premier exporters are shifting from standard Q235 steel to high-yield Q355B/SS500 cold-rolled structural steel. Advanced roll-forming lines allow manufacturers to engineer multi-ribbed upright columns (with 8-12 bend profiles) that achieve higher buckling strength with thinner profiles, yielding substantial savings in freight and raw material costs without compromising load-bearing limits.
3. Environmental Coatings & Anti-Corrosion Technologies
Cold chain logistics (-30°C freezer environments) and chemical storage warehouses demand specialized surface treatment finishes. High-durability hot-dip galvanizing (HDG) and thermosetting epoxy-polyester powder coatings (60–80 microns thick) ensure anti-corrosion performance over 20+ years. Automated electrostatic powder coating lines ensure zero VOC emissions while delivering scratch and impact resistance under daily forklift operations.
4. Integrated IoT Telemetry & Real-Time Structural Health Monitoring
Future high-bay racking systems (exceeding 12–15 meters in height) are incorporating IoT load sensors and optical deflection markers. These sensors detect unintended forklift impacts, structural tilt, beam overload deflections exceeding L/200 limits, and seismic vibrations in real time, alerting maintenance teams before structural failures can occur.
Warehouse Storage Racking System Selection Benchmark
Compare structural configurations, space efficiency metrics, SKU flexibility, and operational logic across core industrial racking systems:
| Storage Racking Type | Storage Density | Pallet Selectivity | Operational Logic | Forklift Aisle Width | Recommended Application |
|---|---|---|---|---|---|
| Selective Pallet Rack | Standard (30-40%) | 100% Direct Access | FIFO / LIFO | 3.5m – 4.0m | High-SKU distribution, general manufacturing, 3PL |
| Very Narrow Aisle (VNA) | High (55-65%) | 100% Direct Access | FIFO / LIFO | 1.6m – 1.9m | High vertical warehouses, pharmaceutical, e-commerce |
| Double Deep Pallet Rack | Medium-High (50%) | 50% Immediate Access | LIFO | 3.5m – 3.8m | Multiple pallets per SKU, food & beverage storage |
| Drive-In / Drive-Through | Very High (65-75%) | Low (Per Lane) | LIFO (Drive-In) / FIFO | Enters Racking Lane | Homogeneous bulk cargo, raw material batch storage |
| Radio Shuttle System | Maximum (80-85%) | High (Per Channel) | FIFO & LIFO Controlled | Outer Access Aisle Only | Cold storage freezers, FMCG, high-volume production |
| Steel Mezzanine Platform | Multiplies Floor Area | Manual / Pallet Gate | Flexible Direct Access | N/A (Multi-level Floor) | Small-parts manual picking, assembly, spare parts |
Why Global Buyers Partner with PrimeBay Heavy Duty Racking
As a leading China warehouse racking system manufacturer since 2006, PrimeBay Heavy Duty Racking Co., Ltd. bridge the gap between heavy structural engineering and competitive factory-direct manufacturing. Operating from our 40,000m² manufacturing base in Nanjing, Jiangsu, we engineer turnkey industrial storage solutions for buyers, engineering contractors, and storage distributors in over 85 countries.
International Certification & Compliance
Production processes are fully audited and certified under CE, ISO 9001 (Quality Management), ISO 14001 (Environmental Management), and TUV safety standards. We guarantee structural load calculations strictly conform to FEM 10.2.02 and RMI standards.
Complete OEM / ODM Flexibility
We provide full custom design services for distributors, engineering contractors, and facility managers. From custom upright profiles, beam box dimensions, structural color matching (RAL colors), and branded packaging to engineered load signage, we accommodate full OEM/ODM specs.
Custom CAD Layouts & Structural Integrity
Send your warehouse floor plan, clear ceiling heights, column locations, and forklift specs to our engineering team. We deliver precise 2D/3D CAD layouts, FEA stress analyses, dynamic bill of materials (BOM), and direct factory quotes within 24 hours.
Frequently Asked Questions (FAQ) for Pallet Racking Sourcing
Answers to common questions regarding structural engineering, loading safety, export logistics, and customization options:
Which international quality and safety certifications do PrimeBay racking systems carry?
Can you engineer and design custom racking layouts directly from my CAD drawings?
What is the structural warranty period for heavy-duty industrial racking?
How do I choose between Drive-In, Push-Back, and Radio Shuttle Racking systems?
• Drive-In Racking: Ideal for high-density, low-SKU bulk inventory under Last-In, First-Out (LIFO) inventory control at the lowest capital cost per pallet.
• Push-Back Racking: Ideal for medium-SKU storage with 2 to 5 pallets deep per lane, utilizing gravity-fed nested carts under LIFO operation without forklifts entering the rack structure.
• Radio Shuttle Racking: Delivers the highest space utilization under either FIFO or LIFO operation. Powered shuttle carts move pallets automatically deep within channels, reducing forklift drive times and minimizing rack collision risks—making it the ideal choice for cold storage freezers and high-volume food and beverage operations.
What raw steel grades and surface finishing standards do you apply?
Transform Your Warehouse Efficiency & Storage Capacity
Contact our structural design team today to request a free warehouse layout optimization plan, structural load calculations, and factory-direct pricing for your racking project.