Explore engineered mobile storage solutions designed to double warehouse storage capacity, optimize cold storage thermal efficiency, and eliminate unused aisle space. All units are manufactured under ISO 9001 quality controls with CE and TUV compliance.
Warehousing Storage Heavy Duty Steel Fabric Multi-Level Corrosion Protection Truck Tyre Cold Storage Stacking Metal Racks
Inquire Now
Material Rack Automated Storage Electric Mobile Warehouse Racking Systems Mobile Rack For Storage
Inquire Now
Automatic Warehouse Storage Shelving System / Mobile Shelving System From China Supplier
Inquire Now
Heavy Duty Adjustable Mobile 5-Layer Cold-Rolled Steel Shelving with 22m Height 300kg Load for Factory Storage
Inquire Now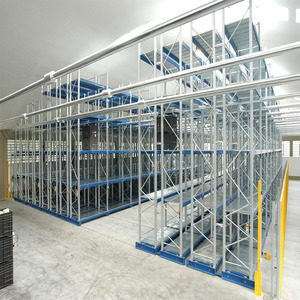
Heavy-Duty Automated Mobile Storage System Electrically Operated Mobile Shelves
Inquire Now
Heavy Duty Multipurpose Storage Rack Cage Cart Door and Window Cargo Warehouse Workshop Turnover Trolley
Inquire Now
Wooden Nightstand Organizer Night Stand Desk Charging Station Watch Glasses Storage Rack Wooden Mobile Phone Docking Station
Inquire Now
MZG Chrome Wire Shelving Rack Multi-Tier Mobile Storage Rack with Wheels Adjustable Durable for Hospital Medical Warehouse
Inquire NowExecutive Summary: The Shift to High-Density Mobile Storage Racking
In modern supply chain management, land acquisition costs and warehouse operational expenses have surged globally. Traditional static pallet racking systems devote up to 60% of total floor area exclusively to forklift access aisles. Mobile Storage Racking (also known as Powered Mobile Racking or Heavy-Duty Electric Mobile Shelving) resolves this operational bottleneck by mounting conventional racking structures onto motorized mobile bases guided by floor-embedded tracks.
By consolidating multiple aisles into a single operational aisle opened dynamically on demand via Programmable Logic Controllers (PLC) or RF remote control, mobile racking increases usable storage density by 80% to 120% within the same physical footprint.
Technical Benchmark: Mobile Racking vs. Alternative Systems
| Storage System Type | Storage Density | Pallet Selectivity | Relative Cost / Pallet | Optimal Industry Application |
|---|---|---|---|---|
| Powered Mobile Racking | Very High (85%–90%) | 100% Direct Access | Medium - High ROI | Cold Storage, 3PL, Chemical, Spare Parts |
| Standard Selective Pallet Rack | Low (40%–45%) | 100% Direct Access | Low | General Distribution, FMCG High-Turnover |
| Drive-In Racking | High (70%–75%) | Low (LIFO Only) | Medium | Homogeneous Bulk Items, Low SKU count |
| ASRS (Crane/Shuttle Automated) | Ultra-High (90%+) | 100% Automated | High Initial Investment | Large Automated Distribution Hubs |
Top 10 Mobile Storage Racking Factories & Exporters (2026 Evaluation)
Our SEO Growth and Logistics Engineering team evaluated over 60 global manufacturers based on Finite Element Analysis (FEA) structural safety, motor redundancy, PLC interface stability, international certifications (CE, ISO 9001, TUV), export capacity, and factory-direct pricing. Below are the premier global suppliers leading the mobile racking sector:
Headquarters / Manufacturing Base: Nanjing, Jiangsu, China (40,000 m² Facility)
Core Strengths: 20+ years of high-density steel racking engineering, in-house cold roll-forming, automatic welding robots, continuous electrostatic powder coating, and specialized low-temperature (-30°C) electric mobile racking motors.
PrimeBay engineered systems feature heavy-duty steel profiles (Q235B/Q355B steel), photo-electric safety light curtains, emergency stop pushbars, distance sensors, and integrated Siemens/Schneider PLC control panels. Exporting to 85+ countries with full CAD/3D structural calculation reports and a 10-year structural warranty.
A pioneer in automated logistics systems, SSI Schaefer offers heavy-duty mobile pallet racking (MOVO) tailored for cold storage and automated high-bay warehouses across Europe and North America.
Stow is a prominent European manufacturer specializing in mobile racking (Stow Mobile) and pallet shuttle systems, providing compliant warehouse solutions built to FEM guidelines.
Mecalux provides Movirack electrical mobile pallet racking solutions with integrated safety devices, software automation, and global distribution hubs.
Dexion manufactures custom mobile shelving and heavy-duty mobile racking systems engineered for archival, industrial tool storage, and cold room logistics.
Jungheinrich delivers complete intralogistics ecosystems combining electric mobile rack bases with specialized reach trucks and AGV integration.
Montel designs high-density powered mobile storage systems mainly for institutional, museum, medical, and light industrial commercial warehousing.
Known for vertical lift modules, Kardex also engineers automated dynamic storage carriages for electronics assembly and high-density unit load handling.
Frazier specializes in structural steel channel pallet racking, offering heavy-duty structural mobile racking bases for North American industrial users.
AR Racking produces heavy-duty mobile racking systems engineered for high-bay environments with automated galvanized steel roll-forming machinery.
Future Procurement & Technological Trends (2026–2030)
As global logistics shifts toward smart warehousing and carbon-neutral facility management, mobile storage racking systems are undergoing rapid technological evolution:
1. WMS/WCS Microservices Integration
Next-gen electric mobile racking units no longer rely solely on physical buttons. They integrate via REST APIs or OPC UA protocols directly into Warehouse Management Systems (WMS), allowing aisles to open automatically ahead of incoming AGVs or autonomous forklifts.
2. Low-Energy & Solar DC Drive Systems
Modern mobile carriages are utilizing variable frequency drive (VFD) brushless DC motors with regenerative braking, reducing peak electrical load start-up currents by up to 35%—a critical factor for cold storage plants.
3. Multi-Sensor Active Safety Architecture
Safety standards now require dual-layer protection: floor-level photoelectric laser curtains, emergency stop bars, and overhead ultrasonic anti-pinch sensors to protect personnel and material handling equipment.
4. High-Seismic & Cold Storage Alloys
Sourcing specs increasingly require micro-alloyed steel (e.g., Q355ND) rated for impact toughness at sub-zero temperatures down to -30°C, combined with FEA-validated seismic anchor designs.
Enterprise Advantages: PrimeBay Heavy Duty Racking Co., Ltd.
Established in 2006, PrimeBay Heavy Duty Racking Co., Ltd. operates a state-of-the-art 40,000 m² manufacturing plant located at No. 22 Ankang Road, Guli Industry District, Nanjing, Jiangsu, China. Over two decades of dedicated R&D and industrial manufacturing have established PrimeBay as a global OEM/ODM manufacturing authority in industrial racking systems.
Stringent Quality Certifications
Fully certified under ISO 9001 (Quality Management), ISO 14001 (Environmental Management), CE Mark (European Conformity), and TUV Rheinland testing standards. Full inspection certificate copies are provided with every quotation.
Full Engineering & Custom CAD Support
Our engineering department provides custom layout design, structural load calculations, and seismic analysis tailored to your specific floor drawing, column grid, forklift turning radius, and pallet dimensions.
In-House Precision Manufacturing
Equipped with 18 automated cold roll-forming production lines, robotic beam welding cells, continuous phosphating wash, and dual-station epoxy powder coating tunnels delivering durable, corrosion-resistant steel structures.
10-Year Comprehensive Warranty
All PrimeBay heavy-duty selective, mobile, radio shuttle, and mezzanine racking systems carry a 10-year structural product warranty supported by comprehensive global after-sales engineering assistance.
Frequently Asked Questions (Mobile Racking Procurement FAQ)
Technical guidance for warehouse managers, industrial general contractors, procurement officers, and 3PL operational managers.
Transform Your Warehouse Space Today
Send us your warehouse CAD drawing, clear ceiling height, pallet footprint, and max load requirements. PrimeBay engineers will generate a complimentary 3D layout, structural calculation, and factory-direct price quotation within 24 hours.