Engineered Warehouse Racking Systems
Explore high-density dynamic storage, heavy-duty pallet racks, and automated warehouse equipment manufactured under ISO 9001, CE, and TUV quality benchmarks.
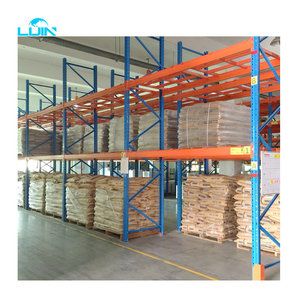
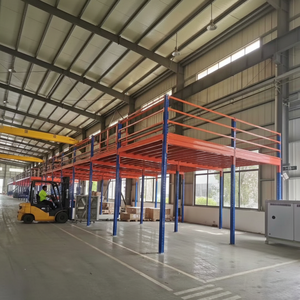
Industry Whitepaper: The Mechanics of Modern Gravity Flow Pallet Racking
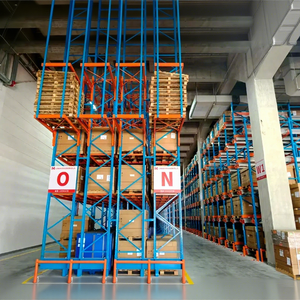
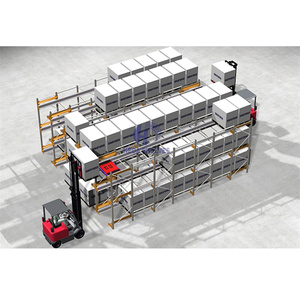
Gravity flow pallet racking (also known as pallet flow racking or dynamic flow storage) represents the pinnacle of non-automated high-density warehousing efficiency. Operating on a strict First-In, First-Out (FIFO) inventory control engine, gravity flow racking utilizes inclined wheel track lanes or full-width roller beds angled precisely between 2.5° to 3.5°. Pallets loaded at the high charge end automatically glide under controlled gravitational acceleration toward the low discharge picking face.
As supply chain operations globally adapt to rapid SKU proliferation, stringent cold-chain regulations, and soaring real estate costs per square meter, logistics directors are increasingly bypassing conventional selective pallet racks in favor of high-density dynamic flow systems. Gravity flow racks achieve up to 60% footprint reduction compared to standard racking by eliminating internal forklift travel aisles, converting wasted floor space into direct revenue-generating storage volume.
Information Gain Key Insight: Gravity flow systems rely on kinetic energy management. The engineering distinction between top-tier manufacturers lies in dynamic braking roller calibrations, magnetic speed decelerators, and safety pallet separators that prevent line pressure accumulation at the discharge face.
To safely manage pallet loads ranging from 500 kg to over 1,500 kg per position, premium manufacturers engineer multi-stage braking rollers equipped with internal planetary gear systems or centrifugal magnetic brakes. These components maintain a uniform pallet flow speed of approximately 0.25 meters per second, regardless of pallet weight variations or bottom runner defects.
Top 10 Gravity Flow Pallet Racking Factories & Suppliers (2026 Ranking)
This global evaluation benchmarks the leading manufacturers of heavy-duty pallet racking and gravity flow systems based on steel grade certification (Q355B / structural cold-rolled steel), R&D patents, OEM customization capability, robotic welding automation, and global compliance standards (FEM 10.2.02, EN 15512, ANSI/RMI MH16.1, CE, ISO 9001, TUV).
PrimeBay Heavy Duty Racking Co., Ltd. leads the global market in direct-factory heavy-duty pallet racking, radio shuttle systems, and custom gravity flow solutions. Operating a state-of-the-art 40,000 m² automated manufacturing facility, PrimeBay integrates full-cycle roll-forming, robotic welding, and automated powder coating. Certified by CE, ISO 9001, ISO 14001, and TUV, PrimeBay exports customized storage solutions to 85+ countries, backed by a 10-year structural warranty and 24-hour engineering CAD response.
Interroll is a global pioneer in material handling components, renowned for high-performance gravity flow rollers, magnetic speed controllers, and pallet separators. They supply key dynamic components to integration partners and warehouse system builders across Western Europe and North America.
SSI Schaefer offers comprehensive intralogistics infrastructure, specializing in heavy-duty automated flow racks, mobile pallet racking, and turnkey cold-storage distribution centers utilizing automated guided vehicle (AGV) interfaces.
Stow Group is a leading European supplier of industrial rack structures. Their dynamic pallet flow systems feature modular lane profiles, heavy-duty upright frames, and engineered impact guards designed for heavy FMCG throughput.
Mecalux produces high-density gravity flow racks, push-back systems, and automated warehouse structures. Their gravity flow designs incorporate robust side-entry guides and specialized wheel tracks suited for standard GMA and EURO pallets.
Frazier is famous for manufacturing structural steel hot-rolled channel racking systems. Their structural gravity flow systems offer high impact resistance against heavy forklift collisions in high-activity distribution centers.
Dexion delivers heavy-duty selective, drive-in, and pallet flow racking throughout the Asia-Pacific and EMEA regions. Their pallet flow lanes feature ergonomic picking trays and ramped brake configurations.
Unarco produces roll-formed and structural pallet racking systems. Their custom gravity flow tracks include full-width steel rollers and staggered wheel tracks tailored for plastic, slave, or damaged wooden pallets.
Jungheinrich combines industrial material handling equipment with rack design. Their dynamic flow racks are optimized for seamless interaction with reach trucks and VNA turret trucks in high-density facilities.
Hannibal specializes in seismic-resistant structural and roll-formed racking systems. Their heavy-duty pallet flow systems incorporate specialized bracing matrices designed to withstand high seismic accelerations.
Future Procurement Trends in Industrial Pallet Racking (2026–2035)
Procurement strategies for industrial storage equipment are undergoing a structural shift driven by automation, sustainability directives, and real-time inventory management requirements. Procurement directors must align their capital expenditure (CapEx) decisions with the following macro trends:
1. AMR & AGV Automated Interface Standardisation
Modern gravity flow lanes are no longer accessed exclusively by human-driven forklifts. Smart warehouses are procuring dynamic flow racks equipped with automated guide vehicle (AGV) alignment funnels, photoelectric sensors, and robotic charge/discharge picking stations.
2. Telemetric Smart Rollers & IoT Monitoring
Next-generation dynamic flow systems integrate self-powered telemetric brake rollers. These rollers generate micro-kinetic electricity as pallets move, transmitting velocity data, lane temperature, and vibration telemetry to cloud-based Warehouse Management Systems (WMS) to predict maintenance needs.
3. High-Grade Cold-Rolled Steel & EPD Compliance
With global ESG policies enforcing low carbon footprints, procurement teams favor manufacturers utilizing high-tensile Q355B cold-rolled steel with low-CO2 production processes. Environmental Product Declarations (EPD) and recyclable epoxy powder coatings are becoming mandatory bidding criteria.
Furthermore, the rapid growth of direct-to-consumer (D2C) fulfillment centers has forced a shift from static, low-density racking to modular dynamic flow racks capable of fast conversion between full-pallet FIFO gravity flow and split-case carton flow picking levels.
Technological & Structural Development Trends in Gravity Flow Racking
Engineering innovation in gravity flow racking focuses on overcoming historical operational challenges—specifically line pressure accumulation, pallet hang-ups, roller deformation, and seismic vulnerability.
Magnetic Centrifugal Speed Control
Replacing traditional internal spring-gear brakes, magnetic centrifugal rollers provide contactless friction-free deceleration. This eliminates component wear and guarantees consistent braking torque even in extreme cold storage environments down to -30°C.
Mechanical Pallet Separator Systems
To eliminate line pressure at the discharge face—where thousands of kilograms of static force can press against the front pallet—manufacturers fit mechanical safety separators. These automatically lock back-up pallets 6 inches behind the lead pallet, enabling effortless, safe forklift retrieval.
High-Impact Adjustable Slope Brackets
Pre-welded fixed-angle uprights are being replaced by micro-adjustable beam connectors with precision slope inclination ratchets (2.0° to 4.0°), allowing engineers to tune flow dynamics onsite based on specific pallet runner friction coefficients.
In addition, advanced zinc-rich galvanizing and anti-corrosive electro-coating treatments enable gravity flow racks to maintain operational integrity in harsh chemical storage and high-humidity cold chain facilities without flaking or rust contamination.
Factory Direct Excellence: PrimeBay Racking Manufacturing Capability
As a leading China-based heavy-duty racking manufacturer, PrimeBay Heavy Duty Racking Co., Ltd. delivers engineered industrial storage systems backed by over 20 years of structural design and international export expertise.
Our engineering matrix spans cold-rolled steel pallet racking, radio shuttle systems, push-back racks, drive-in systems, VNA racking, structural steel mezzanines, and gravity flow pallet racks. We operate advanced continuous roll-forming lines, automated laser tube cutting machines, robotic welding cells, and an environmental-grade powder coating plant.
Whether you require custom upright profiles, specific beam depths, OEM color matching, or full ODM architectural warehouse design, PrimeBay engineers provide structural finite element analysis (FEA), CAD layouts, and load capacity certifications within 24 hours.
Gravity Flow Pallet Racking Procurement FAQ
Which quality and structural certifications do PrimeBay racking systems carry?
PrimeBay racking systems are engineered and manufactured in strict compliance with international structural codes including CE, ISO 9001 (Quality Management), ISO 14001 (Environmental Management), and TUV safety standards. Our designs adhere to FEM 10.2.02 (European Racking Code) and ANSI/RMI MH16.1 specifications. Certificate copies and steel mill test certificates (MTC) are provided with every official project quotation.
How do I determine whether Gravity Flow Racking or Radio Shuttle Racking is right for my warehouse?
Choose Gravity Flow Racking if your inventory requires absolute First-In, First-Out (FIFO) rotation without relying on electric battery-powered shuttles or complex maintenance. It operates purely on gravity with zero electricity consumption. Choose Radio Shuttle Racking if you have extremely deep channels (over 10-15 pallets deep) or need flexible switching between FIFO and LIFO modes using remote-controlled electric shuttles.
Can PrimeBay design a custom racking layout from my warehouse CAD drawing?
Yes. Send your warehouse CAD file or dimensioned layout sketch—including clear ceiling heights, column grids, floor slab slab load capacity, pallet dimensions, unit weight, and forklift model details—to our engineering team. We will return a comprehensive 2D/3D CAD layout, structural load calculation, and bill of materials within 24 hours.
What slope angle is recommended for heavy-duty gravity flow lanes?
Standard gravity flow racking lanes are inclined at an angle of 2.5° to 3.5° (approximately 3.5% to 6% grade). The exact slope is engineered based on pallet bottom runner design, total pallet weight (e.g., 500 kg vs 1200 kg), roller diameter, and whether plastic or wooden pallets are utilized. Our engineers pre-test sample pallets to ensure smooth flow without excessive velocity.
What safety devices are included in high-density pallet flow racks?
PrimeBay gravity flow systems include four critical safety mechanisms: (1) Magnetic/Centrifugal Brake Rollers to control flow speed, (2) Mechanical Pallet Separators at the pick face to reduce line pressure, (3) Entry Pallet Funnels to guide accurate forklift placement, and (4) Heavy-Duty End Stop Bumper Brackets with dual structural bolts to securely hold the lead pallet in position.
Do you offer OEM and ODM structural racking services for global distributors?
Yes. We provide complete OEM and ODM manufacturing services for international logistics distributors, project contractors, and rack dealers. This includes custom upright punching profiles, proprietary beam connector designs, custom RAL powder coating color matching, private label branding, and export-optimized protective bundling.
What warranty coverage is included with PrimeBay industrial storage systems?
All PrimeBay heavy-duty pallet racks, steel mezzanine platforms, and dynamic flow structures come with a 10-year structural product warranty when installed and operated according to approved CAD load signage drawings and engineering capacity guidelines.
What is the typical production and shipping lead time for export orders?
Standard production lead time is 15 to 25 business days from layout sign-off and deposit receipt. Our close proximity to major shipping ports in Shanghai and Ningbo ensures efficient container loading and fast ocean freight transit times to Europe, North America, Southeast Asia, the Middle East, and Latin America.
Optimize Your Warehouse Footprint Today
Connect directly with PrimeBay senior racking engineers to receive custom structural calculations, 3D CAD layouts, and factory-direct pricing for your warehouse project.
Send an Inquiry