Enterprise Product Catalog
High-Density Double Row & Heavy-Duty Pallet Racking Systems
Engineered for high structural stability, maximum cube utilization, and compliance with ISO 9001, CE, and FEM 10.2.02 European standards.
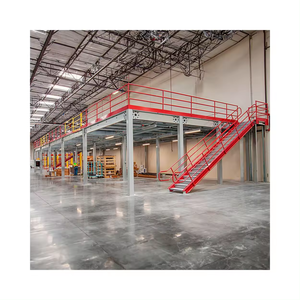
Industrial Mezzanine Floor Rack System Platform
Get a Quote
CE Certified Industrial Warehouse Pallet Storage System
Get a Quote
Heavy Duty Adjustable Mobile Steel Storage System
Get a Quote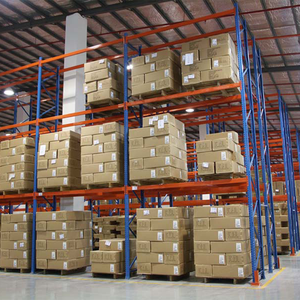
Reinforced Steel Selective Pallet Racking with Guard Rails
Get a Quote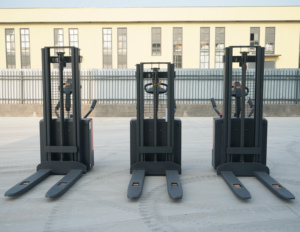
Electric Reach Stacker & Forklift System Integration
Get a Quote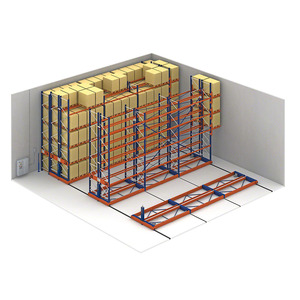
Automated Electric Mobile Warehouse Storage Racking
Get a Quote
Custom Heavy-Duty Iron Metal Warehouse Racking Equipment
Get a Quote+40%
Storage Density vs Selective
20+
Years Manufacturing Experience
85+
Countries Exported Worldwide
10-Year
Factory Structural Warranty
Understanding Double Row (Double-Deep) Pallet Racking Engineering
In modern intralogistics, warehouse operators face a constant friction point: balancing maximum storage floor density with immediate pallet accessibility (selectivity). Single-selective pallet racking delivers 100% direct access to every pallet position but requires extensive dedicated forklift operating aisles, often utilizing less than 42% of total building cubic footprint.
Double Row Pallet Racking (frequently designated as Double-Deep Pallet Racking) stores pallets two rows deep instead of one, placing back-to-back rack structures in a consolidated grid. By eliminating 50% of inner operating aisles required by traditional single-selective systems, double row pallet racking increases operational storage capacity by 30% to 45% within the same physical warehouse footprint.
LIFO Inventory Velocity
Operates on a Last-In, First-Out workflow per lane. Highly suited for manufacturing, cold storage, and bulk distribution storing identical SKUs.
Reach Truck Compatibility
Requires specialized extended reach trucks equipped with a dual-pantograph mechanism or telescopic forks engineered for deep frame extension.
Reinforced Frame FEA
Custom structural upright profiles designed with Finite Element Analysis to counteract additional rotational moment arms created by deep loading.
Technical Comparison: Double Row vs. Other Heavy-Duty Racking Systems
| Storage Racking System Type | Floor Space Utilization | Direct Selectivity Ratio | Forklift Equipment Required | Capital Expenditure (CapEx) |
|---|---|---|---|---|
| Double Row (Double-Deep) Pallet Rack | High (60-68%) | 50% Direct Access | Pantograph Reach Truck / Telescopic Forks | Moderate / High ROI |
| Standard Selective Pallet Racking | Medium (40-45%) | 100% Direct Access | Standard Counterbalance / Reach Truck | Standard Economy |
| Drive-In / Drive-Through Racking | Very High (75-80%) | Low (Per Lane LIFO) | Standard Counterbalance (Enters Rack) | Low - Moderate |
| Radio Shuttle Automated Racking | Ultra High (>85%) | Automated FIFO/LIFO | Automated Shuttle Cart + Standard Lift | Higher Capital Investment |
Sourcing Criteria: How to Evaluate the Top 10 Double Row Racking Factories
Purchasing heavy-duty structural steel racking directly from international manufacturers involves strict risk management. A structural racking failure caused by improper steel roll-forming, poor weld penetration, or incorrect load beam deflection calculations can lead to catastrophic warehouse accidents and multimillion-dollar supply chain delays.
When evaluating global exporters and tier-1 China factories, professional procurement directors and structural engineers must verify six vital manufacturing benchmarks:
- Raw Material Certification & Tensile Integrity: Leading exporters utilize certified structural grade cold-rolled steel (Q235B and high-yield strength Q355B). Mill test certificates (MTC) according to EN 10204 3.1 must verify yield strength and elongation limits.
- Automated Continuous Cold Roll-Forming Precision: Modern factories employ multi-stage CNC continuous roll-forming production lines to ensure uniform profile thickness, zero torsional twist, and exact hole pitch tolerances across 11+ meter vertical upright frames.
- Robotic Beam Connector Welding: Heavy-duty load beams require automatic robotic arc welding between beam profiles and multi-claw end connectors. This guarantees 100% weld penetration, preventing fatigue cracks under continuous cyclic pallet loading.
- Electrostatic Powder Coating Durability: Surface treatment must include multi-stage pre-washing, degreasing, phosphatizing, and automatic thermosetting epoxy powder coating (>80 microns thickness) to withstand humidity, impact, and cold store temperatures.
- Compliance with International Racking Standards: Verify that designs comply with EN 15512 (European structural code for adjustable pallet racking), ANSI MH16.1 (US RMI specification), and FEM 10.2.02.
Manufacturing Powerhouse
PrimeBay Enterprise Advantages & Production Capability
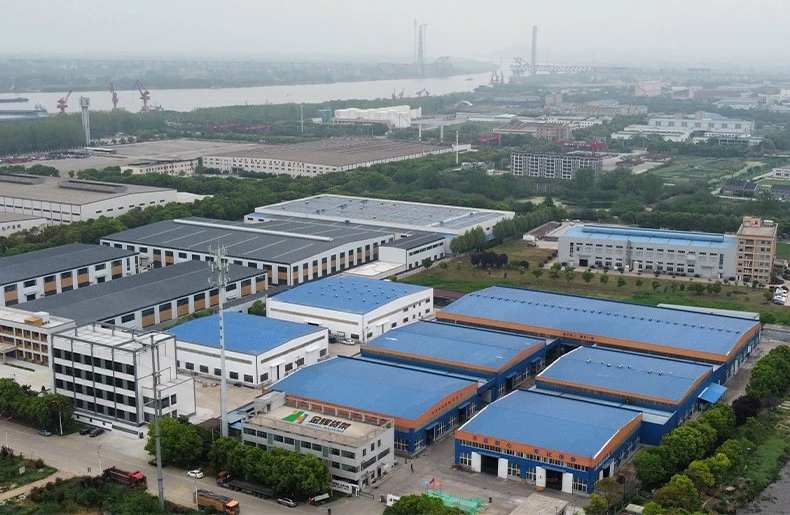
Established in 2006, PrimeBay Heavy Duty Racking Co., Ltd. has grown into one of Asia's premier double row and heavy-duty industrial storage system exporters. Operating out of a state-of-the-art 40,000 square meter manufacturing base in Nanjing, China, PrimeBay delivers custom warehouse racking to clients across 85+ countries.
- Full Engineering Team & CAD/FEA Service: In-house structural engineers provide customized 2D CAD floor plan optimization and Finite Element Analysis load reports before production.
- Certified Quality System: Certified under ISO 9001, ISO 14001, CE marking, and independently audited by TUV Rheinland for global compliance.
- Robust OEM & ODM Capabilities: Full OEM manufacturing supporting customized upright profiles, unique powder coating color palettes (RAL standard), custom branding, and specialized export packaging.
- 10-Year Factory Structural Warranty: Backed by rigorous quality control from raw coil inspection to final loading container sea-freight packaging.
Future Development & Sourcing Trends in Industrial Racking Systems
As global logistics shifts towards automation, supply chain resilience, and environmental sustainability, procurement strategies for double row pallet racking systems are rapidly evolving. Buyers must position their infrastructure for four major industry shifts:
AGV & AMR Integration
Double row racking frames are increasingly modified with optical reflector brackets and guided floor entry tracks to accommodate Autonomous Mobile Robots and automated reach stackers.
High-Tensile Thin-Gauge Steel
Advancements in cold-formed metallurgical processing enable Q355B and high-yield micro-alloy steels to reduce structural dead weight while increasing ultimate beam deflection limits.
Sustainable & Green Sourcing
Modern buyers mandate zero-VOC powder coating processes, eco-friendly zinc-phosphate pretreatment, and fully recyclable steel profiles to align with global ESG directives.
In addition, seismic engineering has become a critical procurement factor. Exporters must now calculate dynamic response spectrum analysis for double row installations situated in active seismic zones (such as South America, New Zealand, and coastal Asia-Pacific regions), utilizing heavy-duty baseplates, chemical anchor bolts, and vertical X-bracing towers.
Expert Answers
Frequently Asked Procurement & Engineering Questions
Direct technical guidance from PrimeBay's engineering and international logistics team.
What is the exact aisle width requirement for Double Row Pallet Racking?
Operating aisle widths for double row racking typically range from 3.0 meters to 3.4 meters, depending on the extended reach pantograph forklift model. While slightly wider than narrow aisle (VNA) systems, double row racking completely eliminates half of the aisles required by standard selective setups, yielding a net building space saving of up to 40%.
How do you manage inventory rotation in a LIFO Double-Deep system?
Double row racking operates on a Last-In, First-Out (LIFO) protocol per individual bay depth. To prevent stock aging, warehouse management systems (WMS) assign identical SKUs (or products with matching batch/lot dates) to both front and rear pallet positions within the same depth lane.
What structural safety accessories are recommended for double row installations?
Because rear pallets are loaded at extended reach distances, safety accessories are crucial. We strongly recommend installing pallet guide rails, rear pallet stop beams (safety backstops), frame column protectors, and heavy-duty row spacers to maintain rigid alignment between double back-to-back frames.
Can PrimeBay engineer racking systems to custom building drawings?
Yes. Send your CAD warehouse floor plan along with building clear heights, floor slab load ratings, pallet dimensions (W x D x H), unit pallet weights, and forklift specifications. Our engineering team will return a complete 2D layout, bill of materials, and structural calculation report within 24–48 hours.
What certifications and warranties do PrimeBay double row racking systems carry?
All PrimeBay manufacturing operations adhere to ISO 9001 and ISO 14001 standards. Our structural designs carry CE certificates and comply with EN 15512, FEM 10.2.02, and ANSI MH16.1 specifications. Every system comes standard with a 10-year factory structural warranty.
What is the standard production lead time and ocean export shipping arrangement?
Standard manufacturing lead times are 15 to 25 days from order confirmation and deposit. Components are securely bundled on custom steel pallets with protective wrapping to prevent shipping scratch damage inside 40ft High Cube containers. We provide complete EXW, FOB, CIF, or DDP shipping terms worldwide.
Optimize Your Warehouse Storage Density Today
Consult with PrimeBay's senior structural racking engineers. Get a complimentary warehouse CAD design, load capacity analysis, and direct factory pricing within 24 hours.
Get a Quote