Automated & Heavy-Duty Pallet Handling Systems
Direct-from-factory high-density racking, radio shuttle systems, and automated storage solutions engineered to ISO 9001, CE, and TUV standards.
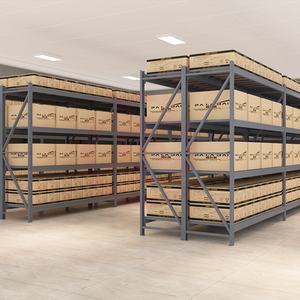
Heavy Duty Adjustable Mobile 5-Layer Cold-Rolled Steel Shelving with 22m Height 300kg Load for Factory Storage
Inquire Now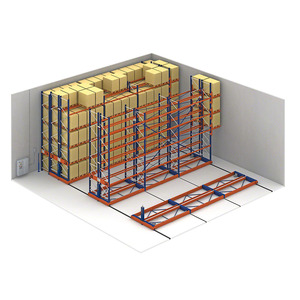
Material Rack Automated Storage Electric Mobile Warehouse Racking Systems Mobile Rack For Storage
Inquire Now
Industrial Steel Products VNA Very Narrow Aisle Selective Pallet Racks Steel Shelves Rack
Inquire Now
HUAWU 5 Ton Heavy Duty Selective Pallet Rack Steel Q235 Industrial Warehouse Storage Racking System PR-05
Inquire Now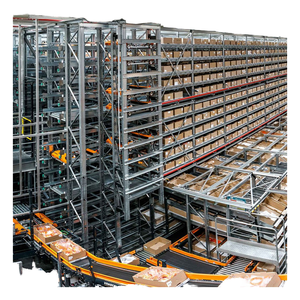
Automated Storage and Retrieval System Warehouse Bins Storage Solutions Pallet Rack ASRS Racking System
Inquire Now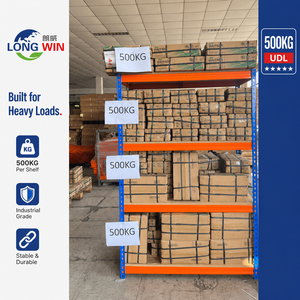
Extra Heavy Duty Boltless Steel Rack 5-Tier Adjustable 2000kg Rivet Lock Garage Warehouse Heavy Duty Warehouse Rack
Inquire Now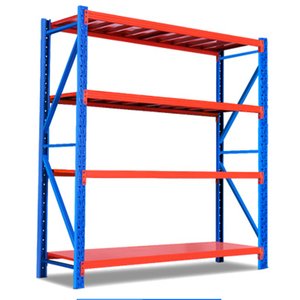
HUAWU 200kg Per Layer Boltless Shelving System 4 Shelf Steel Q235 Light Duty Warehouse Storage Rack HD036
Inquire Now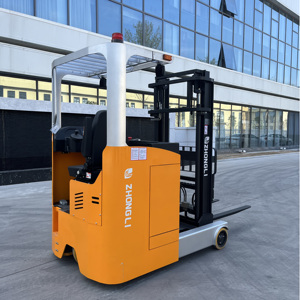
Reach Truck 8m 12m Storage Big Battery Stacker Seated Type Electric Reach Truck Mounted Forklift Stacker
Inquire NowTop 10 Automated Pallet Handling System Factories & Global Exporters Benchmark
As modern logistics transitions toward hyper-efficiency and automated labor replacement, selecting the right automated pallet handling factory is critical for industrial real estate developers, 3PL providers, cold chain operators, and large manufacturing facilities. Automated Pallet Handling Systems (APHS)—encompassing Automated Storage and Retrieval Systems (AS/RS), 2-Way and 4-Way Radio Shuttle Matrices, Electric Powered Mobile Racking (PMR), and Very Narrow Aisle (VNA) automated guided vehicle environments—demand rigorous structural integrity, precise component tolerances, and deep software-hardware integration capability.
In accordance with global quality frameworks such as FEM 10.2.02, EN 15635, and ANSI/RMI MH16.1, we have benchmarked the world’s top 10 factories and exporters specializing in automated pallet handling systems. These manufacturers have demonstrated technical superiority, high-capacity cold-rolled steel profiling, rigorous quality assurance, and international export leadership.
PrimeBay Heavy Duty Racking Co., Ltd. (China)
Headquartered in Nanjing, PrimeBay is a premier OEM/ODM exporter with a 40,000 m² smart production center. Specializing in high-bay ASRS structural racks, 4-Way Radio Shuttle matrices, and heavy-duty cold-rolled steel racking systems certified to CE, ISO 9001, ISO 14001, and TUV.
Daifuku Co., Ltd. (Japan)
A global pioneer in material handling automation, Daifuku excels in fully integrated stacker crane ASRS systems, automated rail-guided vehicles (RGV), and complex warehouse control software systems for automotive and semiconductor industries.
SSI Schaefer Group (Germany)
Renowned for European structural engineering excellence, SSI Schaefer produces high-density automated pallet shuttles, mobile racking, and pallet conveyor networks designed for extreme cold storage environments.
Mecalux, S.A. (Spain)
Operating major steel fabrication facilities in Europe and the Americas, Mecalux offers advanced Pallet Shuttle systems, clad-rack warehouse structures, and integrated WMS/WCS logistics software.
Dematic / KION Group (USA/Germany)
A global supply chain automation behemoth specializing in high-throughput pallet automated storage, micro-fulfillment automation, and heavy load transport AGVs.
Jungheinrich AG (Germany)
Integrates automated narrow aisle (VNA) equipment, automated reach trucks, and modular radio shuttle racking systems built for maximum volumetric storage efficiency.
Kardex Group (Switzerland)
A specialized manufacturer focused on automated dynamic storage and retrieval solutions, heavy pallet vertical lifts, and buffer systems for manufacturing logistics.
Interroll Group (Switzerland)
Global market leader in dynamic pallet flow modules, gravity roller tracks, and magnetic speed controllers essential for FIFO automated pallet flow storage.
System Logistics / Sidel (Italy)
Tailors automated pallet handling systems specifically for the food, beverage, and bottling industries, providing ultra-fast stacker cranes and automated palletizing lines.
Murata Machinery, Ltd. / Muratec (Japan)
Specializes in cleanroom automated pallet storage, high-density automated material handling systems, and rail-guided pallet transport loops for high-tech manufacturing.
Technical Insight for Buyers: Selecting a factory is not merely choosing steel—it is evaluating structural yield strength (Q235 vs Q355B grades), cold-roll profile beam engineering, dynamic deflection limits (L/200 standard), anti-seismic bracing, and surface treatment longevity (such as electrostatic powder coating thickness ≥ 70-80μm).
Future Procurement & Technological Trends in Automated Pallet Handling (2026–2030)
The global automated pallet handling landscape is experiencing a paradigm shift. Rising labor costs, extreme cold-chain storage demands (-25°C to -30°C), and the expansion of omnichannel e-commerce are forcing logistics engineers to move beyond traditional manual racking. When procuring systems over the next decade, enterprise buyers must evaluate four key technological vectors:
1. Shift from 2-Way Shuttles to 4-Way Radio Shuttle Matrix Systems
Traditional 2-way radio shuttles travel only along longitudinal channels, requiring forklifts to move the shuttle between aisles. The emerging global procurement standard is the 4-Way Radio Shuttle System. Operating on custom 3D grid racking channels, 4-way shuttles can change directions autonomously, cross aisles, and ascend vertical lift hoist systems. This transforms racking into a fully automated robotic grid, eliminating up to 90% of internal forklift traffic while increasing storage density by up to 40% compared to traditional selective racking.
2. LiFePO4 Supercapacitors and Green Energy Integration
Energy consumption in 24/7 automated warehouses—particularly cold storage—represents a major operational expense (OPEX). Next-generation shuttle carriers are now manufactured with Lithium Iron Phosphate (LiFePO4) power cells combined with supercapacitors. Featuring 5-minute rapid inductive charging and energy recovery during lowering phases, modern automated shuttles achieve continuous operation while reducing energy consumption by 30-35% compared to legacy lead-acid systems.
3. Plug-and-Play WMS/WCS IoT Ecosystems
Historically, integrating factory-built racking automation with enterprise Resource Planning (ERP) or Warehouse Management Systems (WMS) required custom, costly middleware software. Future-proof procurement demands standardized open API interfaces, MQTT protocols, and 5G industrial IoT sensors directly embedded inside upright frames and shuttles. This enables real-time structural health monitoring, strain gauge overload detection, and predictive maintenance alerts before structural fatigue occurs.
4. Hybrid Mobile Automation: AMR + Mobile Racking
For operations facing space constraints without vertical height for tall ASRS towers, Electric Powered Mobile Racking (PMR) integrated with Autonomous Mobile Robots (AMRs) represents the fastest-growing procurement trend. Mobile racks slide laterally on embedded floor rails to open a single operational aisle on demand, yielding an 85% floor space utilization rate.
| Automated System Type | Volumetric Storage Density | Throughput Speed (Pallets/Hr) | Initial CAPEX | Optimal Industry Application |
|---|---|---|---|---|
| 4-Way Radio Shuttle Matrix | Very High (>85%) | High (Flexibly Scalable) | Medium–High | Cold Chain, FMCG, Beverage, High-Density Stock |
| Crane-Based ASRS (High-Bay) | Maximum (>90%) | Very High (Continuous) | High | Large Manufacturing, 3PL Hubs, Heavy Industrial |
| Electric Mobile Racking (PMR) | High (up to 85%) | Medium (Aisle Opening Time) | Medium | Cold Storage, Chemical, Raw Material Archives |
| Very Narrow Aisle (VNA) Automated | Medium–High (60-70%) | High (Direct Selectivity) | Low–Medium | High SKU Variance, Distribution Centers |
PrimeBay Engineering Capabilities & Manufacturing Excellence
As a specialized manufacturer founded in 2006, PrimeBay Heavy Duty Racking Co., Ltd. operates a 40,000 m² state-of-the-art production base located in Nanjing, Jiangsu, China. Unlike generic trading entities, PrimeBay maintains absolute control over every phase of production—from raw high-strength cold-rolled coil profiling to robotic welding and automated electrostatic powder coating.
High-Grade Certified Steel
We source premium Q235B and Q355B steel coils exclusively from premier national steel mills. Structural load-bearing capacity is validated through finite element modeling (FEM) and physical destructive testing.
Precision Roll-Forming
Equipped with 20+ automated continuous roll-forming production lines, executing sub-millimeter pitch hole punching for high-bay uprights reaching heights up to 25 meters.
Certified Compliance
All manufactured racking and shuttle systems are fully certified under CE, ISO 9001 (Quality), ISO 14001 (Environmental), and TUV Rheinland performance guidelines.
Full OEM & ODM Support
We design custom upright profiles, beam connections, safety accessories, specialized shuttle rails, and custom brand powder coating finishes for engineering contractors and overseas distributors.
Global Project Footprint
Having completed over 2,000 industrial warehouse projects across 85+ countries, our engineering team supplies full CAD/3D layouts, structural calculations, and installation supervisors worldwide.
10-Year Warranty Coverage
Every structural pallet rack installation manufactured by PrimeBay includes a 10-year comprehensive structural warranty, guaranteeing operational safety under design load specifications.