High-Density Mobile & Industrial Pallet Storage Showcase
Explore our factory-engineered range of modular pallet frames, heavy-duty mobile shelving, stackable steel nestainers, and self-loading stackers manufactured to EN 15512 structural specifications.
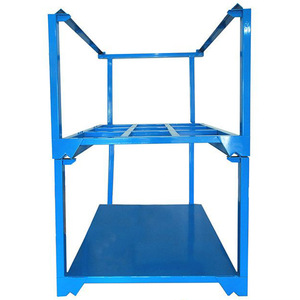
CASE CARTER OEM Warehouse Stack Foldable Portable Vertical Steel Pallet Frame Nestainer Storage Rack System
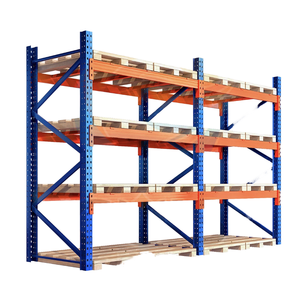
1-5 Layer Heavy Duty US Type Detachable Pallet Rack Storage Steel Stacking Rack Supplier For Bulk Storage Plant Large Warehouse
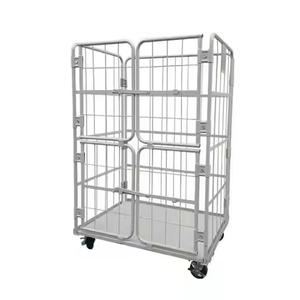
High Quality Portable Collapsible Steel Selective Pallet Rack with Corrosion Protection 1-5 Ton Capacity for Warehouse Storage
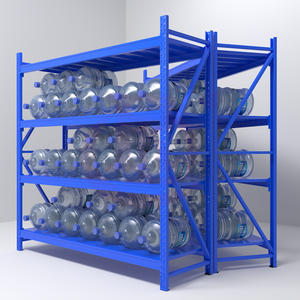
Heavy Duty Adjustable Mobile 5 Layer Cold-Rolled Steel Pallet Rack with 2m Beam 300kg Load for Industrial Warehousing
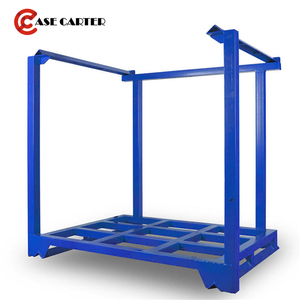
CASE CARTER OEM Powder Coating Heavy Duty Foldable Portable Stacking Steel Tire Storage Rack Palletainer
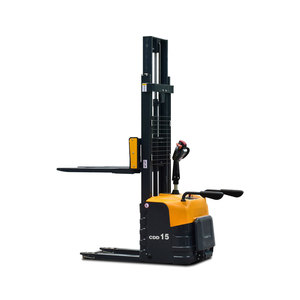
Factory Direct Sales Electric Pallet Lift Stackers 1.5-Ton 2-Ton 3m 4m 5m Portable Self-Loading Systems
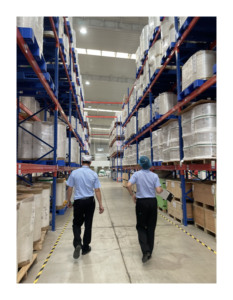
Heavy Duty Mobile Shelving Pallet Rack Warehouse & Supply Selective Racking Boltless Shelving System
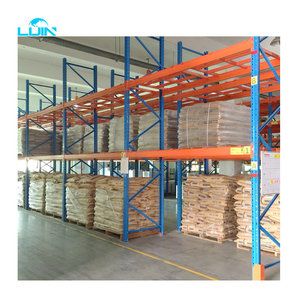
1 Ton Warehouse Storage Adjustable Pallet Racking Shelf Unit Forklift Assemble Manufacturer Steel Rack
Industrial Authority: PrimeBay Engineering Benchmark
Operating from our 40,000 m² state-of-the-art production base in Nanjing, China, PrimeBay Heavy Duty Racking Co., Ltd. has established itself over two decades as a trusted original equipment manufacturer (OEM) and original design manufacturer (ODM) for high-density warehouse storage systems globally.
Rigorous Certification Standards
Our complete manufacturing pipeline is accredited under ISO 9001 (Quality Management), ISO 14001 (Environmental Management), CE safety compliance, and TUV Rheinland structural testing. Every component undergoes raw material testing using certified Q235B and Q355B high-tensile cold-rolled steel profiles.
Full OEM & ODM Engineering
We provide tailored dimensional design, custom upright profile forming, seismic load bracing calculations, specific beam depth selections, electrostatic powder-coating finishes in customized RAL color spectrums, and brand packaging customized for international rack distributors and system integrators.
Turnkey Export Execution
From CAD layout design and structural simulations using Finite Element Analysis (FEA) to strict container loading optimization, pre-drilled components, and detailed step-by-step installation blueprints, PrimeBay guarantees seamless delivery to over 85 countries worldwide.
Engineering Whitepaper: The Evolution of Powered Mobile Pallet Racking (PMR) in Modern Warehousing
In the modern logistics ecosystem, warehouse operators face a dual challenge: escalating land costs per square meter and an increasing demand for high SKU selectivity. Traditional static selective pallet racking provides 100% immediate access to every pallet position but leaves up to 60% of floor space unutilized due to multiple operational aisles. Conversely, static high-density systems like Drive-In or Push-Back racking sacrifice individual pallet accessibility in favor of footprint efficiency.
Powered Mobile Pallet Racking (PMR) eliminates permanent access aisles by mounting heavy-duty selective rack superstructures onto motorized mobile bases guided by floor-embedded steel rails. When a specific storage lane is requested via RF remote, barcode scanning, or WMS integration, the mobile carriages smoothly traverse sideways on heavy-duty steel wheels to create a single working aisle precisely where needed. This simple structural shift increases warehouse volumetric utilization by 80% to 100% compared to static selective racking without losing 100% SKU selectivity.
Core Structural Components & Manufacturing Tolerances
As a specialized B2B manufacturer, PrimeBay engineers mobile racking systems capable of carrying unit loads up to 30,000 kg per double-entry mobile carriage block. Achieving long-term structural reliability under repetitive dynamic movement requires exact metallurgy and structural tolerances:
1. High-Tensile Steel Profiles & Uprights
Our upright frames are cold-rolled from certified Q355B steel, featuring continuous omega-shaped cross-sections designed to maximize torsional rigidity. Profile thicknesses range from 1.8mm to 2.5mm, perforated at precise 50mm or 75mm pitch intervals to allow flexible beam height adjustments while maintaining high load-bearing structural integrity under FEM 10.2.07 standards.
2. Motorized Carriages & Rail Guidance
Mobile bases are fabricated from high-grade structural steel channels housing integrated planetary gear motors and forged steel wheels. Guidance rails—available in flat-surface or inverted V-groove configurations—are precision-ground and anchored into the floor slab, requiring slab levelness tolerances compliant with DIN 18202 standards to prevent dynamic derailment.
Integrated Safety Protocols & PLC Automation Controls
Safety is paramount when maneuvering tons of steel and stacked palletized freight inside industrial spaces. PrimeBay mobile racking systems incorporate multi-layered electronic and mechanical protection systems designed to meet European CE safety directives (EN 15095):
- Continuous Photoelectric Safety Curtains: Infrared optical sensors span the full length of every aisle floor edge. If an operator, forklift, or dropped box interrupts the beam while carriages are moving, the PLC controller immediately engages emergency electronic braking.
- Impact-Absorbing Bumper Switches: Physical micro-switch bumpers run along the bottom sides of each mobile base, stopping carriage motion upon physical contact with any obstacle.
- Aisle Access Locking Systems: Manual or automated keylock switches allow operators to freeze aisle positions during prolonged picking or maintenance operations, preventing unintended rack movement.
- Sub-Zero Cold Chain Operational Design: Internal control panels, wire harnesses, drive motors, and limit switches are treated with specialized anti-condensation heating elements and low-temperature synthetic lubricants, maintaining reliable operation in cold storage environments down to -30°C.
Comprehensive Racking System Technical Comparison Matrix
| Storage Racking System Type | Footprint Capacity Utilization | Direct SKU Access Level | Handling Speed / Throughput | Cost per Pallet Position | Best Industry Application |
|---|---|---|---|---|---|
| Powered Mobile Pallet Rack (PMR) | 85% - 90% (Very High) | 100% (Direct Access) | Medium - High | Medium - High | Cold Storage, 3PL, Pharmaceuticals, Automotive Parts |
| Standard Selective Pallet Rack | 40% - 50% (Standard) | 100% (Direct Access) | High | Low (Baseline) | General Manufacturing, High-Rotation Warehouses |
| Drive-In / Drive-Through Rack | 75% - 85% (High) | Low (LIFO Lane Access) | Slow - Medium | Low - Medium | Raw Material Storage, Bulk Uniform Commodities |
| Radio Shuttle Cart Racking | 80% - 90% (Very High) | Medium (Lane Selectivity) | Very High | High | Food & Beverage, High-Volume FMCG Distribution |
| Stackable Steel Nestainers / Racks | 70% - 80% (Flexible High) | Block Selectivity | Medium | Low | Seasonal Warehousing, Tire Storage, Freight Transit |
Global Procurement & Future Technology Trends in Industrial Racking
As warehouse operations transition toward Industry 4.0 automation, the global procurement strategy for pallet storage systems is shifting from static passive furniture to intelligent integrated hardware. B2B buyers, facility engineers, and supply chain directors must evaluate the following key trends when selecting an OEM/ODM manufacturing partner:
1. Integration with WMS & Autonomous Mobile Robots (AMRs)
Modern mobile pallet racking is no longer operated solely via manual push buttons. Next-generation systems integrate directly with Warehouse Management Software (WMS) via Modbus, Profinet, or Wi-Fi communication protocols. When an Autonomous Mobile Robot (AMR) or automated guided forklift is dispatched to retrieve a pallet, the WMS automatically opens the required aisle en route, eliminating idle travel time and achieving fully automated dark warehousing capability.
2. ESG Sustainability & Cold-Chain Energy Savings
With energy costs rising globally, cold storage facilities represent one of the most energy-intensive warehouse sectors. Because cooling energy consumption is directly tied to total refrigerated building volume, doubling storage density with powered mobile racking reduces cubic meter cooling requirements per pallet by up to 50%. This delivers massive reduction in operational carbon footprints and ongoing utility expenses.
3. Flexible Modular & Portable Stacking Racks (Nestainers)
For third-party logistics (3PL) providers managing fluctuating seasonal inventories, fixed racking installations can restrict layout agility. Modular collapsible steel stack frames and nestainers allow warehouses to erect temporary high-density vertical block storage during peak seasons and fold or nest the frames when empty to reclaim 80% floor area for processing.
4. Advanced Surface Corrosion Treatments for Harsh Environments
Global buyers increasingly require custom surface treatment protocols. PrimeBay provides advanced pre-treatment cleaning, hot-dip galvanizing for humid or chemical applications, and thermosetting epoxy-polyester electrostatic powder coating (60–80 microns thickness). This ensures maximum corrosion resistance, impact durability, and adherence to food safety hygiene standards across tropical, coastal, and sub-zero deployment zones.
Detailed Product Engineering Specifications & Customization
PrimeBay provides specialized OEM/ODM manufacturing across 5 major storage system families. Below is an engineering overview of our primary product lines built for international export.
A. Heavy-Duty Mobile Shelving & Pallet Racks
Designed for high-bay industrial distribution centers requiring maximum floor space efficiency and selective pallet access.
- Load Capacity: 500 kg to 3,000 kg per beam level; up to 30 tons per mobile carriage base.
- Beam Span: Custom clear spans up to 3.9 meters manufactured using high-strength rolled box beams.
- Drive Mechanism: Synchronized electric gear motors with soft-start/soft-stop frequency converters.
- Safety Features: Infrared anti-collision sensors, emergency stop buttons, floor obstacle bumpers.
B. Nestainer Storage Racks & Foldable Steel Frames
Versatile portable stacking racks engineered for bulky items, un-palletized cargo, or flexible bulk storage layouts.
- Stacking Capacity: 1-ton to 2-ton payload capacity per frame; safely stackable 4 to 5 units high.
- Design Flexibility: Foldable vertical posts, nested base frames, detachable side meshes.
- Finish: Heavy-duty powder coating or hot-dip galvanizing for outdoor weather resistance.
- Forklift Handling: 4-way entry design for standard forklift forks and pallet jacks.
C. Heavy Duty US-Type Teardrop Pallet Racking
Standardized selective racking featuring compatible teardrop connection holes widely used across North & South American markets.
- Upright Profile: 3" x 3" standard punch pattern with automatic safety beam lock pins.
- Height Availability: Up to 12 meters single continuous upright profile height.
- Beam Options: Step beams accommodating wire decking, steel shelf plates, or wooden pallets.
- Compliance: Manufactured in accordance with RMI (Rack Manufacturers Institute) standards.
D. Specialized Portable Tire Storage Racks & Palletainers
Dedicated vertical and horizontal stacking solutions tailored for automotive OEMs, tire distributors, and transport hubs.
- Tire Capacity: Holds 28 to 50 passenger or truck tires per stackable unit frame.
- Space Saving: Collapsible side frames fold completely flat when empty for reverse logistics savings.
- Structural Rigidity: Interlocking post caps prevent tipping during high vertical stack storage.
- OEM Branding: Stenciled company logos and customized color matching available.
Frequently Asked Questions (FAQ) for Procurement & Engineering Teams
Clear, authoritative technical answers addressing common structural, installation, and procurement questions raised by warehouse operators and importers prior to purchasing.
What warehouse floor slab specifications are required for installing powered mobile pallet racking?
How does PrimeBay ensure quality control during structural steel manufacturing?
Can PrimeBay design and manufacture custom OEM/ODM racking according to existing warehouse drawings?
What safety features protect operators working inside mobile racking aisles?
What is the typical production lead time and export delivery process for overseas buyers?
What warranty and after-sales support does PrimeBay provide for international projects?
Request a Custom Layout & Structural Racking Quotation
Partner directly with China's leading OEM/ODM mobile pallet racking manufacturer. Our engineering team is ready to analyze your warehouse floor plan and optimize your storage density.
Fast Response Guaranteed | Free CAD Engineering Layouts | Factory-Direct Pricing