Featured Industrial Storage & Pallet Racking Systems
Explore our core OEM/ODM pallet racking configurations designed for maximum cube utilization, cold storage efficiency, and heavy load capacity.
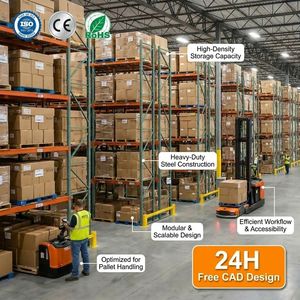
CE Certified Industrial Warehouse Stacking Shelves Pallet Rack Storage System for Logistic Center
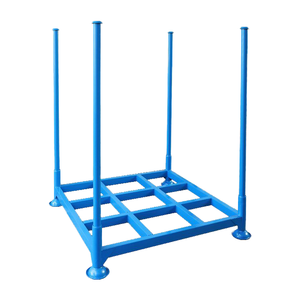
Warehousing Storage Heavy Duty Steel Fabric Multi-Level Corrosion Protection Truck Tyre Cold Storage Stacking Metal Racks
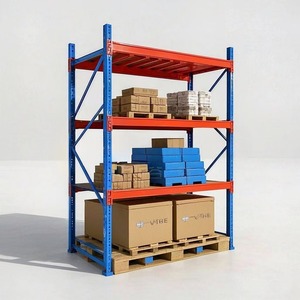
Factory Direct Custom Heavy-Duty Pallet Shelving Green Safe Storage Racks Industrial Free Adjustment Height for Warehouse
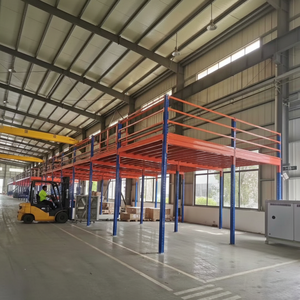
Custom Heavy-Duty Two-Story Mezzanine Racking Platform Warehouse Multi-Level Storage Flooring System in Red/Blue
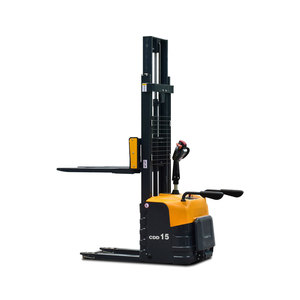
Factory Direct Sales Electric Pallet Lift Stackers 1.5-Ton 2-Ton 3m 4m 5m Portable Self-Loading
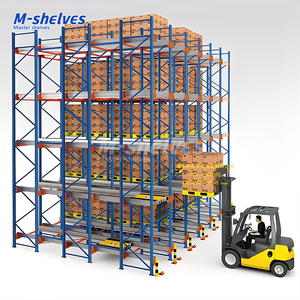
Innovative Auto Shuttle Racking System for Intelligent Cold Storage Steel Pallet Racks Automatic Shuttle Shelving
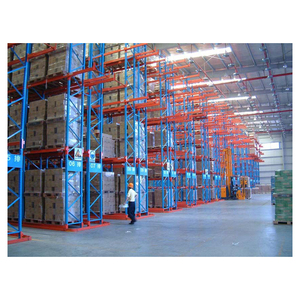
Narrow Aisle Racks Factory Price Heavy Duty VNA Rack Very Narrow Aisle Racking High Density Warehouse Storage Rack
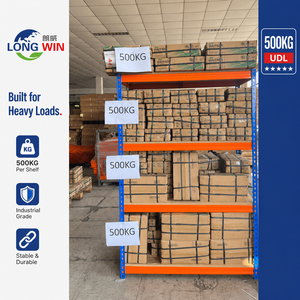
Extra Heavy Duty Boltless Steel Rack 5-Tier Adjustable 2000kg Rivet Lock Garage Warehouse Heavy Duty Warehouse Rack
Technical Architecture of OEM/ODM Drive-In Pallet Racking Systems
An authoritative analysis of high-density LIFO storage mechanics, load redistribution dynamics, and steel structural integrity.
Modern warehouse logistics managers and industrial civil engineers face a constant operational challenge: maximizing cubic volumetric storage efficiency while minimizing capital expenditure per pallet position. Drive-In Pallet Racking systems represent the gold standard for high-density Last-In, First-Out (LIFO) inventory management, eliminating operational aisles to consolidate up to 75% to 85% of total floor space into productive storage slots.
Unlike standard selective pallet racking, where every row is separated by dedicated forklift aisles, Drive-In racking allows counterbalanced or reach forklifts to physically enter the rack structure’s internal bays. Pallets rest on continuous heavy-duty cantilever support rails mounted to upright columns. This continuous lane architecture requires precise engineering calculation, strict steel metallurgical standards, and robust structural bracing to handle dynamic operational stress, impact loads, and seismic forces.
High-Yield Cold-Rolled Steel
Utilizing high-tensile Q235B and Q355B structural steel profiles. Upright posts undergo precision multi-stage cold roll forming to optimize moment of inertia and buckling resistance under heavy axial compression.
Cantilever Rail & Arm Geometry
Engineered pallet support rails feature a tapered entry lip and heavy gauge steel formation. This self-centering design prevents pallet snagging and ensures seamless forklift insertion deep into 2 to 10+ pallet lanes.
Structural Portal & Top Bracing
To compensate for the lack of traditional horizontal beam ties inside forklift lanes, top structural beams and rear diagonal X-bracings bind frame tops into a rigid 3D diaphragm structure compliant with FEM 10.2.02 standards.
Cold Storage & Bulk Commodity Optimization
Drive-In pallet racking shines brightest in environments where facility operating costs are extremely high per square meter—most notably in refrigerated cold storage warehouses (-25°C to -30°C), fast-moving consumer goods (FMCG) distribution centers, agricultural seed storage, and raw chemical material facilities.
By removing 60% of forklift aisles compared to selective racking setups, heating or cooling efficiency increases exponentially. The reduced air volume movement minimizes thermal loss, directly reducing monthly HVAC energy consumption while doubling pallet capacity on the existing concrete floor slab.
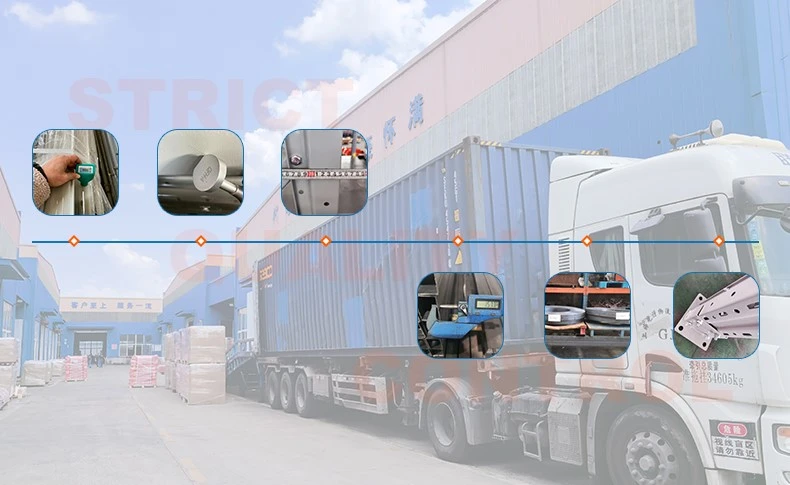
Tailored Engineering for Global Racking Distributors & EPC Contractors
Custom dimensions, structural profiling, safety accessories, and automated manufacturing precision.
At PrimeBay Heavy Duty Racking Co., Ltd., we act as the primary OEM (Original Equipment Manufacturer) and ODM (Original Design Manufacturer) engine for leading European, American, Middle Eastern, and Southeast Asian storage system integrators. No two warehouses share identical floor plan parameters, pallet weights, or forklift clearance envelopes. Therefore, our engineering team utilizes finite element analysis (FEA) software to tailor rack structural components to exact client specifications.
Custom Steel Profiles & Upright Options
We roll-form upright column profiles ranging from 80mm to 120mm face widths with steel thicknesses from 1.8mm up to 3.0mm. Pitch adjustments are available in standard 50mm, 75mm, or 76.2mm (3-inch) increments, allowing exact vertical compatibility with existing legacy racking brands worldwide.
Corrosion Protection & Surface Finishing
All finished components undergo a 7-stage pre-treatment wash including zinc phosphating, followed by high-grade electrostatic thermosetting epoxy polyester powder coating (60–80 micron thickness). For deep-freeze environments or high-humidity outdoor applications, hot-dip galvanizing (HDG) coating per ISO 1461 is fully supported.
High-Density Storage Systems Decision Matrix
Compare operational characteristics across main industrial warehouse racking configurations to evaluate storage density, selectivity, and overall investment.
| Racking Architecture | Storage Density | SKU Selectivity | Operational Logic | Forklift Compatibility | CapEx cost per Pallet |
|---|---|---|---|---|---|
| Drive-In Pallet Racking | Very High (75-85%) | Low (Per Lane LIFO) | LIFO (Last-In, First-Out) | Standard Counterbalance / Reach | Economical / Low |
| Drive-Through Racking | High (70-80%) | Medium (Dual Access) | FIFO (First-In, First-Out) | Standard Counterbalance / Reach | Low to Medium |
| Radio Shuttle Racking | Maximum (85-90%) | Medium (Per Lane) | FIFO or LIFO (Automated) | Standard Forklift + Shuttle Bot | Medium to High |
| Push-Back Racking | High (65-75%) | Medium (2-5 Deep) | LIFO (Nested Carts) | Standard Reach Truck | Moderate |
| Selective Pallet Rack | Standard (35-40%) | 100% Direct Access | FIFO / LIFO Flexible | All Forklift Types | Lowest Initial CapEx |
Future Development Trends in Drive-In & High-Density Storage (2025–2035)
How automation, IoT sensing, and green steel manufacturing are reshaping industrial warehousing.
AGV & AMR Guided Entry Integration
The transition from human forklift drivers to Autonomous Guided Vehicles (AGVs) requires narrower tolerances (+/- 2mm) on pallet rail alignments. Future OEM Drive-In systems feature laser reflector target plates and optical guide channels built into the base floor rails.
Smart Structural Health Sensors
Integrating wireless IoT strain gauges and piezoelectric impact sensors on bottom column uprights. Maintenance managers receive instant alerts on mobile dashboards if a forklift bumps a protective column guard during operation.
Sustainable Zero-VOC & Eco-Steel
Global logistics operators are demanding carbon-neutral warehouse supply chains. Manufacturing modern drive-in racks uses recycled electric arc furnace (EAF) steel and solvent-free lead-free powder coatings, dropping embodied carbon footprint by over 30%.
Why Partner with PrimeBay Heavy Duty Racking Co., Ltd.?
Over two decades of precision cold roll-forming, global logistics export expertise, and rigorous quality assurance.
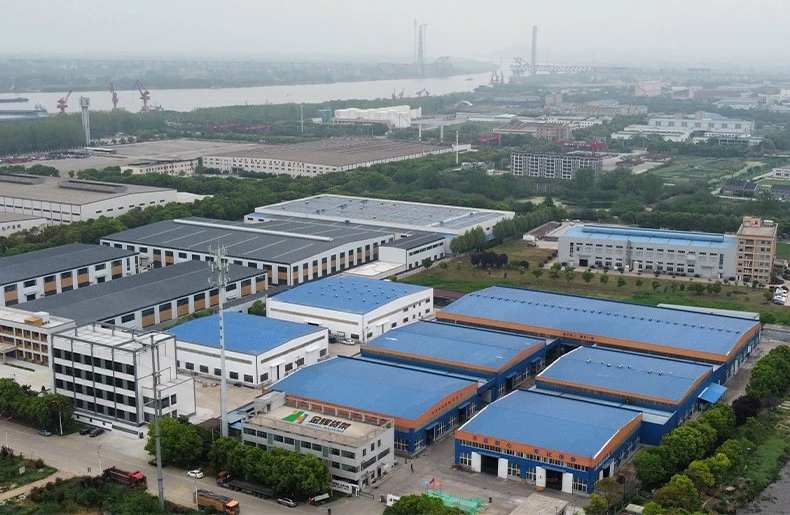
20+ Years of Manufacturing Excellence in Nanjing
Established in 2006, PrimeBay Heavy Duty Racking Co., Ltd. operates a modern 40,000 square meter manufacturing facility in the Guli Industry District of Nanjing, Jiangsu, China. Equipped with fully automated continuous roll-forming production lines, robotic welding stations, and automated powder coating plants, we deliver end-to-end quality control from raw steel coil inspection to final sea freight packaging.
Our complete structural product ecosystem includes Heavy Duty Pallet Racking, Drive-In & Drive-Through Storage Systems, Radio Shuttle Racks, Push-Back Racks, Steel Mezzanine Platforms, VNA Racking, and Cantilever Racks exported to over 85 countries worldwide.
CE & TUV Certified
Fully compliant with EN 15512, EN 15620, EN 15629, and FEM 10.2.02 European design norms. Factory verified by ISO 9001, ISO 14001, and TUV Rheinland.
In-House Testing Rig
Equipped with universal tension testing machines, salt-spray corrosion chambers, and full-scale column compression testing rigs to verify dynamic capacity.
10-Year Warranty
All structural steel uprights, load arms, and top beams are covered under our binding 10-year factory warranty against structural manufacturing defects.
Global Turnkey OEM/ODM
From CAD layout design, structural engineering calculation reports to containerized sea shipment and installation supervision manuals.
Frequently Asked Questions for OEM/ODM Racking Buyers
Expert answers addressing structural engineering, procurement workflows, customization, and freight packaging.
What warehouse parameters are required to calculate a Drive-In Racking quote?
To produce an accurate CAD layout, structural load calculation, and quotation, our engineering team requires: (1) Warehouse building CAD drawing or dimensioned sketch showing column grid, clear height under trusses, building doors, and obstacles; (2) Pallet dimensions (Length x Width x Height including cargo overhang); (3) Maximum weight per loaded pallet (e.g., 1000kg or 1500kg); (4) Forklift specifications including overall collapsed mast height, maximum lift height, turning radius, and outer chassis width.
How does Drive-In racking compare to Radio Shuttle racking in operational costs?
Drive-In racking has a significantly lower initial Capital Expenditure (CapEx) because it contains no electrical or motorized moving components. However, Radio Shuttle racking reduces forklift driver cycle times because the shuttle moves pallets deep inside the channel automatically. Drive-In racking remains the preferred economical choice for low-turnover, homogenous bulk storage where budget optimization is primary.
Which certifications do PrimeBay racking systems carry for international projects?
Our production facilities and products carry CE certification (European Conformity), ISO 9001 (Quality Management), ISO 14001 (Environmental Management), and TUV Rheinland factory audit compliance. Full certificate copies and structural steel test reports (MTC - Mill Test Certificates) are provided alongside quotation and shipping documentation.
What protective measures are installed to prevent forklift collision damage?
Because forklifts enter directly inside the rack structure, protection is paramount. We engineer heavy-gauge steel column guards (independent floor-anchored or snap-on wrap protectors), continuous floor guide rails (angle steel or heavy C-channel profile) running the entire lane length, and heavy-duty portal top ties to absorb dynamic forklift impacts without compromising column load capacity.
Can PrimeBay manufacture custom upright profiles matching our local brand standards?
Yes. As a dedicated OEM/ODM manufacturer, we offer custom cold-roll tooling to replicate or integrate with major global racking post profiles (such as 50mm pitch, 75mm pitch, or 76.2mm 3-inch pitch teardrop configurations). We also support private labeling, custom RAL electrostatic powder colors, and branded carton packaging for global rack distributors.
What steel grades and mill standards are used in your racking components?
We strictly utilize certified hot-rolled coil structural steel conforming to Q235B (yield strength ≥ 235 MPa) for standard beams and bracings, and Q355B / Q345B (yield strength ≥ 355 MPa) for heavy-duty tall upright columns. Every raw material batch undergoes chemical analysis and tensile yield testing prior to roll forming.
What is the standard production lead time and sea freight loading capacity?
Standard manufacturing lead time is 15 to 25 business days following CAD drawing sign-off and deposit receipt. Components are bundled with steel strapping, protective cardboard corners, and wooden skid bases designed for rapid loading and unloading via forklift from 40ft High Cube (40HQ) shipping containers.
What is the maximum lane depth for Drive-In pallet racking lanes?
Drive-In lanes typically range from 3 to 10 pallets deep. While deeper lanes increase volumetric density, lanes deeper than 7–8 pallets are often configured as Drive-Through racking (accessible from both front and back) to maintain reasonable driver turnaround times and mitigate collision risks.
How are seismic forces and floor concrete anchor loads calculated?
Our structural engineering team reviews local building code seismic zone coefficients (PGA values). We calculate minimum concrete slab thickness (typically 150mm to 250mm reinforced concrete) and specify high-tensile mechanical expansion anchors or chemical epoxy anchor bolts to withstand seismic shear and overturning uplift moments.
What structural warranty and after-sales support do you provide?
PrimeBay racking systems are backed by a comprehensive 10-Year Structural Warranty. In addition, we supply detailed 3D step-by-step assembly drawings, installation videos, safety load signage plates for bay ends, and remote engineering inspection support during site installation.
Ready to Optimize Your Warehouse Cube Storage Capacity?
Contact PrimeBay's engineering design team today. Send us your building floor plan or racking project parameters for a complimentary CAD layout and OEM quotation within 24 hours.