Engineered Pharmaceutical Storage Systems
Factory-direct pallet racking solutions customized for strict temperature control, hygiene compliance, and heavy-duty load handling.
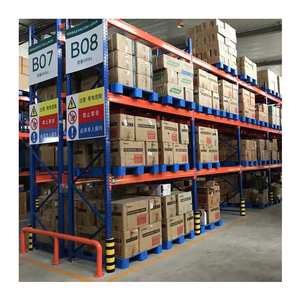
Heavy Duty Selective Pallet Rack 5 Ton Capacity Industrial Warehouse Storage Shelving System Adjustable Steel Rack
Get Catalog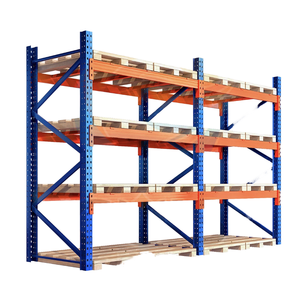
1-5 Layer Heavy Duty US Type Detachable Pallet Rack Storage Steel Stacking Rack Supplier For Bulk Storage Plant Large Warehouse
Get Catalog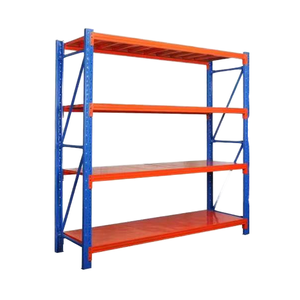
Mracking Heavy Duty Selective Galvanized Steel Shelf Good Quality Warehouse Stacking Pallet Racking System Corrosion Protection
Get Catalog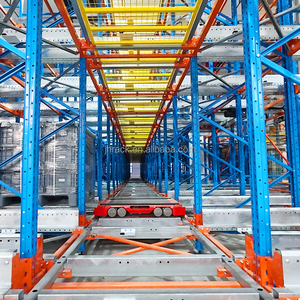
Customizable Multi-Deep 4-Way Shuttle Pallet Racking System | High-Density Automatic Pallet Rack Storage for Distribution Center
Get Catalog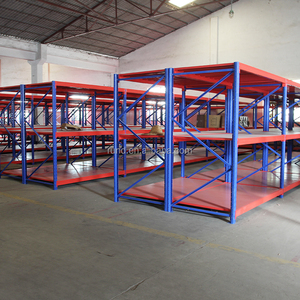
Heavy Duty 5-Layer Selective Pallet Rack 1500-4500kgs/level Warehouse Storage System Steel Iron Stacking Racks Shelves Carton
Get Catalog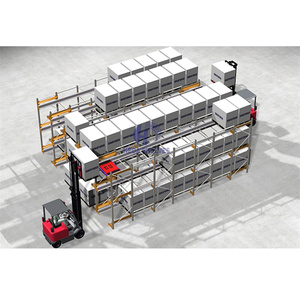
Shuttle Rack Radio Shuttle Rack Pallet Shuttle Rack Automated Storage System for High-Density Pallet Storage FIFO System
Get Catalog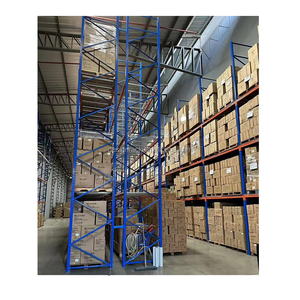
Logistics Center Pallet Rack Warehouse Rack Manufacturer Q235B Steel Heavy Duty Storage Rack Custom Design ISO Certified System
Get Catalog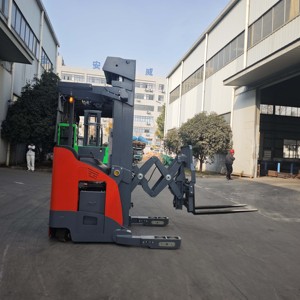
4500 Lbs Heavy Duty High Efficiency Double Deep Pallet Racking Suitable Electric Scissors Reach Truck
Get CatalogEngineering Compliance in Pharmaceutical Pallet Racking Architecture
The global pharmaceutical logistics sector operates under stringent regulatory frameworks where inventory integrity, batch traceability, and environmental controls directly impact public health and enterprise viability. Unlike standard retail distribution centers, pharmaceutical warehouses demand structural rack systems engineered to satisfy Good Manufacturing Practice (GMP) and Good Storage Practice (GSP) mandates. Selecting premier China Top Pharmaceutical Pallet Racking Manufacturers & Suppliers is no longer merely a procurement exercise in structural steel acquisition—it is an strategic decision involving structural safety, anti-microbial surface treatment, seismic resistance, and automated cold chain compatibility.
In modern biopharmaceutical and active pharmaceutical ingredient (API) storage operations, floor space utilization must be balanced against atmospheric circulation, thermal mapping uniformities, cleanroom particulate boundaries, and strict First-In, First-Out (FIFO) stock management. As high-value biologics, vaccines, and temperature-sensitive therapeutics flood global supply chains, industrial racking systems must eliminate off-gassing, prevent steel oxidation under high-humidity conditions, and provide high-density structural stability under continuous dynamic loading.
Structural Steel Integrity & Surface Engineering Standards
The structural load dynamics of pharmaceutical pallet racks require precise finite element analysis (FEA) modeling. Pharmaceutical unit loads frequently carry immense concentrated weights—ranging from 1,000 kg to over 4,500 kg per beam level—requiring high moment of inertia profiles for upright columns and box beams to prevent elastic deformation over multi-decade lifespans.
Leading Chinese racking manufacturers employ high-grade structural steel (SS400, Q235B, and Q355B grade profiles) precision roll-formed on automated continuous production lines. Beam connector hooks are stamped with 3 to 4 safety claws and fitted with automatic safety locks to eliminate risk of dislodgement during rapid forklift access.
| Technical Specification | Standard Commercial Racking | Pharma-Grade Heavy Duty Racking | Compliance Impact |
|---|---|---|---|
| Steel Raw Material | Standard Recycled Commercial Steel | Certified Prime Q235B / Q355B Cold-Rolled Steel | Eliminates structural fatigue & micro-defects |
| Surface Finish | Basic Industrial Spray Paint | Thermosetting Anti-Microbial Powder / Galvanized | Zero VOC off-gassing; resistant to wipe-down chemicals |
| Cold Storage Tolerance | 0°C to +40°C | -30°C to -80°C Ultra-Low Bio-Freezer Safe | Prevents low-temperature steel embrittlement |
| Cleanroom Class | Non-certified (dust trap design) | ISO Class 5 to Class 8 Compatible | Smooth closed-profile welds prevent particulate accumulation |
| Structural Certifications | Local Mill Test Certificates | CE, ISO 9001, ISO 14001, TUV, ANSI/RMI MH16.1 | Full regulatory audit acceptance (FDA / EMA) |
Racking System Selection Guide for Bio-Pharma Logistics
Selecting the optimal pallet racking configuration requires aligning warehouse clear height, SKU variety, turnover rates, and cold chain power consumption. Below is an engineering comparison matrix designed for pharmaceutical warehouse operations directors and facility engineers:
Selective Pallet Racking
Storage Density: Standard (40-50% Floor Utilisation)
Selectivity: 100% Direct Pallet Access
Best For: High SKU variety, raw material quarantine zones, clinical trial batch storage. Allows immediate inspection and isolation of specific lot numbers.
Radio Shuttle Racking
Storage Density: Very High (75-85% Floor Utilisation)
Selectivity: Lane-by-Lane (FIFO / LIFO)
Best For: Cold storage vaults, vaccine distribution centers, mass finished-goods warehousing. Semi-automated shuttle vehicles eliminate forklift intrusion into sub-zero vaults.
Automated 4-Way Shuttle ASRS
Storage Density: Ultra-High (85-95% Floor Utilisation)
Selectivity: Fully Automated Individual SKU Retrieval
Best For: Fully automated lights-out pharmaceutical logistics hubs. Integrates seamlessly with WMS/WCS software for real-time inventory serialization.
Future Sourcing & Technology Trends in Pharmaceutical Storage Racking
As the pharmaceutical industry shifts toward personalized medicine, mRNA therapeutics, and localized cold chain hubs, warehouse storage requirements are undergoing a profound technological transformation. Forward-thinking procurement teams must evaluate structural racking systems based on long-term adaptability and green supply chain initiatives.
1. Integration with Autonomous Mobile Robots (AMRs)
Modern pharma facilities are transitioning from standard forklifts to fleet-managed AMRs and automated guided vehicles (AGVs). Racking bases now incorporate precision floor guide channels, RFID positioning markers, and laser-reflective target plates built directly into upright profiles to facilitate sub-millimeter robotic docking.
2. Smart Sensor Structural Health Monitoring
High-bay pharmaceutical racking systems reaching heights of 15 to 40 meters are increasingly outfitted with IoT strain gauges, tilt sensors, and ambient temperature sensors. These integrated smart devices provide real-time alerts regarding structural overloading, seismic shock, or air circulation dead zones that could compromise thermal stability.
3. Net-Zero Carbon & Eco-Coating Systems
Global pharmaceutical corporations are enforcing Scope 3 carbon reduction mandates on their equipment vendors. Chinese manufacturers lead this transition by utilizing 100% recyclable structural steel, zero-VOC electrostatic powder application, and solar-powered manufacturing operations.
Why Partner with PrimeBay Heavy Duty Racking Co., Ltd.
PrimeBay Heavy Duty Racking Co., Ltd. stands as a premier manufacturer and global exporter of high-spec industrial warehouse storage systems. Operating from our 40,000 square meter advanced manufacturing base in Nanjing, Jiangsu, we specialize in high-load, precision-engineered storage solutions for pharmaceutical distributors, third-party logistics (3PL) providers, and industrial operations worldwide.
Our fully integrated manufacturing plant houses continuous roll-forming lines, automated robotic welding cells, Swiss-engineered powder coating lines, and rigorous quality control laboratories. Every project commissioned with PrimeBay undergoes rigorous finite element structural calculation, ensuring structural compliance with international structural standards including EN 15512, FEM 10.2.02, and ANSI/RMI MH16.1.
Frequently Asked Questions (FAQ) for Global Buyers
Addressing essential technical, quality control, and international shipping queries from pharmaceutical warehouse procurement officers.
What specific certifications guarantee PrimeBay racking meets international pharma standards?
PrimeBay manufacturing processes and product lines hold full certifications for CE, ISO 9001 (Quality Management), ISO 14001 (Environmental Management), and TUV Rheinland structural safety compliance. Detailed structural load test reports and raw material mill certificates (MTC) are delivered with every quotation and shipment batch.
How do your racking designs accommodate cleanroom hygiene and sterilization protocol?
Our pharmaceutical-grade racking utilizes closed box beams, smooth tubular columns, and fully welded seams that eliminate recessed crevices where moisture or dust accumulates. Coatings are specifically formulated to withstand continuous wiping with isopropyl alcohol (IPA), hydrogen peroxide vapor (VHP), and quaternary ammonium sanitizers without coating degradation.
Can PrimeBay engineer cold storage racking for sub-zero bio-pharmaceutical freezers (-25°C to -40°C)?
Yes. Sub-zero cold storage requires micro-alloyed steel formulations with high impact toughness at low temperatures to prevent brittle fracture. We utilize specialized low-temperature carbon steel combined with hot-dip galvanized or cold-room epoxy coatings engineered to prevent rust, blistering, and structural fatigue in extreme cold environments.
Do you offer OEM and ODM structural customization based on existing warehouse drawings?
Absolutely. Send your facility DWG/CAD architectural drawings along with clear floor height, column layout grid, pallet dimensions, load weights, and handling equipment specs. Our senior structural engineering team will deliver optimized layout designs, FEA load calculations, and competitive factory-direct pricing within 24 business hours.
What is the expected lead time and shipping process for overseas projects?
Standard production lead times range from 15 to 25 days depending on total tonnage and custom specifications. Components are packed using protective wooden skids, steel banding, and moisture-proof plastic wrapping to prevent damage during sea transport. We ship FOB, CIF, or DDP to over 85 countries across North America, Europe, Asia, and the Middle East.