Product Catalog
Featured Warehouse Storage & Flow Racking Systems
Explore our heavy-duty engineered racking systems designed for seamless intralogistics, high SKU throughput, and optimized footprint utilization.
Industry Whitepaper
Engineering Excellence in High-Density Carton Flow Racking Systems
Optimizing Fast-Moving SKU Pick Rates, FIFO Inventory Control, and Ergonomic Fulfillment Architecture for Modern Intralogistics Hubs.
In modern warehouse management, material handling efficiency directly dictates supply chain profitability. Fast-moving consumer goods (FMCG), e-commerce fulfillment centers, pharmaceutical distribution hubs, and automotive assembly lines demand dynamic storage solutions that eliminate labor bottlenecks, maximize vertical space utilization, and enforce strict First-In, First-Out (FIFO) stock rotation. Carton Flow Racking—also known as live carton storage or gravity flow rack systems—serves as the backbone of high-efficiency order-picking operations worldwide.
As a leading Chinese manufacturer and global exporter, PrimeBay Heavy Duty Racking Co., Ltd. (operating from our 40,000 m² state-of-the-art production complex in Nanjing, Jiangsu) delivers custom-engineered carton flow storage systems that bridge the gap between static manual shelving and fully automated material handling equipment. By utilizing precision-inclined roller beds and custom-extruded aluminum or durable plastic wheel tracks, our flow racks convert gravity into free kinetic energy. Items loaded from the rear charge lane automatically glide down toward the front discharge picking face, reducing picker search times by up to 75% while boosting overall order fulfillment accuracy.
Dynamic FIFO Optimization
Separate loading and picking aisles prevent forklift and foot-traffic collisions while automatically enforcing strict product expiration management.
Up to 40% Labor Savings
Minimized travel paths allow warehouse pickers to spend less time walking and searching, drastically decreasing cost-per-pick metrics.
Ergonomic Pick Face Design
Available with tilt presentation trays and specialized lane dividers to present cartons at optimal ergonomic angles for reduced picker fatigue.
Technical Architecture
Structural Components & Precision Metallurgy
Built with high-tensile Q235B and Q355B cold-rolled steel profiles for structural integrity under demanding dynamic loads.
A high-performance carton flow rack relies on exact mechanical tolerances and material purity. Unlike low-tier modular shelving, PrimeBay's carton flow beds are integrated into heavy-duty pallet rack frames or standalone multi-tier pick modules. Upright frames are cold-roll-formed from premium structural steel with custom drop-hole patterns, allowing vertical pitch adjustments at 50mm or 75mm increments.
The core mechanism of the system is the gravity flow track array. Each track consists of continuous aluminum alloy frame channels or zinc-plated steel side rails fitted with impact-resistant engineering plastic (polypropylene/polyethylene) rollers or precision steel ball bearings. Depending on carton rigidity, tote dimensions, and total unit weights (ranging from 5 kg to over 100 kg per carton), track pitch and inclination angles are engineered between 3° and 6° (a 4.5% to 8% incline slope).
PrimeBay Technical Component Breakdown
Flow Track & Roller Wheels
High-density polyethylene (HDPE) or high-grade ABS rollers engineered for frictionless glide, low ambient operational noise, and thermal stability from cold storage (-30°C) to high-heat facilities (+50°C).
Sheet Metal Lane Dividers
Full-length adjustable steel dividers lock into track crossbeams without fasteners, preventing carton migration and maintaining pristine lane separation across multi-SKU pick faces.
Ergonomic Impact Trays
Positioned at the discharge end, heavy-gauge steel tilt trays angle cartons toward the operator at 15° to 30°, enhancing line-of-sight visibility for split-case picking and tote replenishment.
Automated Speed Controllers & Brakes
For heavy totes or long flow lanes exceeding 3 meters, integrated centrifugal speed controllers absorb excess kinetic energy to prevent high-impact carton collisions at the discharge stop.
Performance Matrix
System Comparison: Finding the Right Storage Architecture
Compare Carton Flow Racking against traditional static shelving, pick-to-light mezzanines, and automated shuttle systems to select the optimal solution for your throughput profile.
| Storage System Type | SKU Density | Pick Rate (Picks/Hr) | Stock Rotation | Footprint Utilization | Initial ROI Cycle |
|---|---|---|---|---|---|
| PrimeBay Carton Flow Rack | Very High | 400 – 750 / hr | Strict FIFO (Gravity) | 85% - 90% | 6 – 12 Months |
| Standard Static Steel Shelving | Low | 100 – 180 / hr | LIFO / Manual FIFO | 40% - 50% | Baseline |
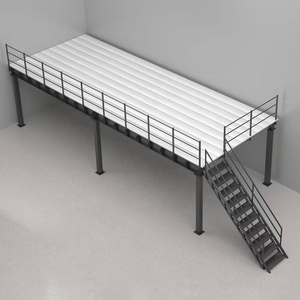
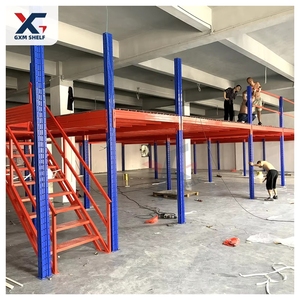
| Multi-Tier Steel Mezzanine Platform | High | 250 – 450 / hr | Manual Batching | 150% - 200% (Vertical) | 12 – 18 Months |
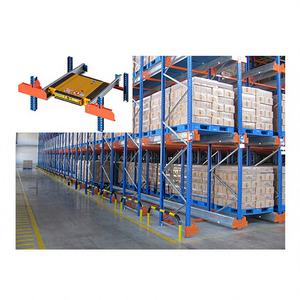
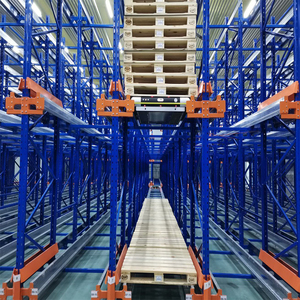
| Automated Radio Shuttle Racking | Maximum (Pallet Level) | 40 – 60 Pallets / hr | FIFO or LIFO | 90% - 95% | 18 – 24 Months |
| Mini-Load ASRS System | Maximum (Tote Level) | 600 – 1000 / hr | Automated FIFO | 95% | 36 – 48 Months |
Why Choose PrimeBay
Nanjing PrimeBay Manufacturing Advantage
20 Years of Global Export Authority, Precision Roll-Forming, and ISO-Certified Quality Assurance.
Founded in 2006, PrimeBay Heavy Duty Racking Co., Ltd. has grown into one of East China's premier racking exporters and system integrators. Located in the Guli Industry District of Nanjing, Jiangsu, our facility houses continuous cold-roll forming lines, high-precision robotic welding arms, automatic CNC punching stations, and a fully automated electrostatic powder coating line spanning over 200 meters.
We do not compromise on quality. Every structural beam, frame, and flow bed bracket is fabricated under stringent quality management systems certified to ISO 9001, ISO 14001, CE, and TUV Rheinland standards. Our internal engineering department utilizes FEM (Finite Element Method) stress analysis software to calculate exact load ratings, seismic tolerances, and beam deflection ratios (staying strictly within FEM 10.2.02 and RMI standards of L/200).
Full OEM & ODM Customization
Tailored upright profiles, custom powder-coat RAL color matching, corporate branding decals, and customized packaging solutions for international distributors.
Global Project Footprint
Trusted by warehouse equipment importers, 3PL logistics providers, and industrial engineering contractors across more than 85 countries globally.
Comprehensive Testing & Pre-Assembly
Factory trial-assemblies are performed prior to export to verify incline drop angles, roller alignment, and snap-in beam connector fitments.
Future Procurement Trends
Emerging Technologies Shaping Dynamic Warehouse Flow Systems
How IoT Integration, AMR Collaboration, and Modular Engineering Are Transforming Conventional Flow Racks.
As global supply chains shift toward omni-channel e-commerce and rapid micro-fulfillment, carton flow racking is evolving from passive mechanical hardware into intelligent, connected intralogistics nodes. Supply chain managers planning racking investments for the next decade must consider several key industry advancements:
1. Integration with Pick-to-Light (PTL) & Put-to-Light Sensors
Modern carton flow discharge channels are increasingly manufactured with pre-punched mounting rails designed for digital Pick-to-Light modules. LED displays guide operators directly to correct flow lanes and show pick quantities, boosting fulfillment speed and reducing order picking errors to near-zero rates.
2. Autonomous Mobile Robot (AMR) & AGV Docking Interfaces
The supply side of carton flow racks is being automated. Rather than relying solely on human replenishers, automated guided vehicles (AGVs) and AMRs equipped with motorized roller beds interface directly with flow rack charge lanes, creating fully automated replenishment cycles.
3. Hybrid Pick-Module Integration
Warehouse designs favor multi-tiered pick modules that combine bottom-level carton flow racks for fast-moving items with upper-level selective pallet racks for reserve stock storage. This maximizes building cube efficiency while reducing internal transport distances.
4. Eco-Friendly & Low-Temperature Polymer Formulations
With cold-chain logistics expanding rapidly for fresh foods and biological products, roller wheel polymers are formulated with specialized plasticizers that resist embrittlement and tracking degradation down to sub-zero freezer environments (-30°C).
Procurement Guide
Frequently Asked Questions (FAQ)
Everything international importers, warehouse managers, and project engineers need to know about specifying and purchasing carton flow systems.
How do I determine the correct slope/incline angle for carton flow tracks?
The standard incline ranges between 3° and 6° (roughly 3.5 to 5 inches of drop per 10 feet of lane depth). Heavier, rigid plastic totes require less tilt (3°–4°), while lighter or softer corrugated boxes may require a steeper angle (5°–6°). PrimeBay performs physical testing using your sample containers to calibrate perfect slope configurations prior to mass production.
Can PrimeBay carton flow beds be retrofitted into existing selective pallet racking?
Yes. Our universal flow track assemblies and mounting brackets are engineered to clip seamlessly into standard teardrop, structural, or European-style box beams. You do not need to replace your entire racking infrastructure; our modular flow beds transform standard selective bays into dynamic flow channels.
What certifications and structural standards do PrimeBay racking systems comply with?
PrimeBay manufacturing processes comply with ISO 9001 (Quality Management System) and ISO 14001 (Environmental Management). Our structural designs conform to European FEM 10.2.02 guidelines, EN 15512 standards, American RMI guidelines, and hold CE safety certification as verified by TUV Rheinland testing.
What is the typical production lead time and export sea-freight packaging method?
Standard manufacturing lead time is 15 to 25 calendar days following CAD drawing sign-off and deposit receipt. All steel components are bundled with corrugated corner protectors, heavy-duty steel strapping, and wrapped in protective plastic film to resist moisture during long sea transits.