Featured Pallet Storage & Conveyor Racking Equipment
Explore high-performance pallet racking, shuttle conveyors, reach trucks, and warehouse safety solutions engineered for global industrial deployment.
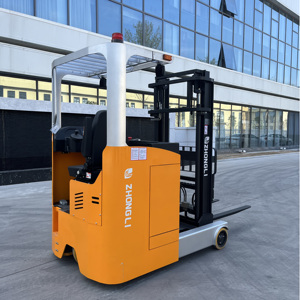
Reach Truck 8m 12m Storage Big Battery Stacker Seated Type Electric Reach Truck Mounted Forklift Stacker
Contact Us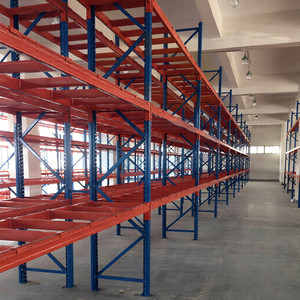
Heavy Duty Steel Pallet Storage Racks Complete Warehouse Pallet Racking Systems Solution Factory Wholesale
Contact Us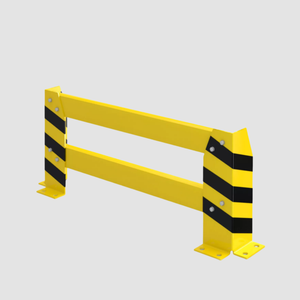
BRIO Modern Heavy Metal Steel Column Crash Safety Upright Pallet Racking Protection System Rack Supports Guard Warehouse
Contact Us
1 Ton Warehouse Storage Adjustable Pallet Racking Shelf Unit Forklift Assemble Manufacturer Steel Rack
Contact Us
Heavy Duty Pallet Storage Rack With Side Safety Mesh Warehouse Adjustable Beam Type Pallet Racking System
Contact Us
CASE CARTER OEM Powder Coating Heavy Duty Foldable Portable Stacking Steel Tire Storage Rack Palletainer
Contact Us
Industrial Logistics Warehouse Storage Rack Heavy Duty Steel Pallet System
Contact Us
CASE CARTER OEM Cargo Storage Equipment Stackable Pallet Tainer Metal Stacking Stillage Nestainer
Contact Us1. Executive Summary: Strategic Value of Pallet Conveyor Storage Systems
In modern industrial logistics, automated material handling and high-density warehouse storage systems have evolved from optional upgrades into core operational imperatives. A Pallet Conveyor Storage System seamlessly integrates heavy-duty structural racking with motorized live roller conveyors, chain transfers, gravity flow tracks, and automated radio shuttle cars. By automating horizontal transport and vertical placement, global supply chain operators achieve unprecedented throughput, zero-collision storage density, and dramatic labor expense reductions.
"Selecting China's premier pallet conveyor and heavy-duty storage racking supplier provides international buyers, 3PL logistics hubs, and EPC contractors with certified European-grade structural compliance (EN 15512, FEM, RMI) at highly competitive factory-direct pricing."
As enterprise procurement managers seek the ideal balance between capital expenditure (CAPEX) and long-term operational performance (OPEX), China's top storage manufacturing hubs—led by engineering leaders like PrimeBay Heavy Duty Racking Co., Ltd.—have emerged as premier manufacturing partners worldwide. This whitepaper analyzes system architectures, technology trends, quality validation standards, and strategic procurement frameworks for pallet conveyor and racking installations globally.
2. Engineering Authority & Manufacturing Infrastructure of PrimeBay
Founded in 2006, PrimeBay Heavy Duty Racking Co., Ltd. operates a flagship 40,000 square meter manufacturing base situated in Nanjing, Jiangsu Province, China. Backed by over two decades of specialized structural R&D, PrimeBay delivers custom warehouse racking, automated radio shuttle tracks, steel mezzanine platforms, and integrated pallet conveyor interfaces for global importers, distributors, and logistics integrators across 85+ countries.
Certified Quality Assurance
Full manufacturing compliance with CE, ISO 9001 (Quality Management), ISO 14001 (Environmental Standards), and TUV Rheinland structural safety certifications.
OEM & ODM Capability
Custom cold-rolled upright profiles, variable beam pitch sizes, specialty powder coatings, structural safety mesh, and private-label packaging for project contractors.
10-Year Structural Guarantee
All load-bearing upright frames and horizontal beams carry an industry-leading 10-year structural warranty backed by FEA stress analysis reports.
From automated high-speed cold-rolled steel forming lines to robotics welding cells and continuous electrostatic thermosetting powder coating tunnels, PrimeBay ensures tight tolerance control, dynamic impact resistance, and flawless paint adhesion for long-term corrosion prevention.
3. Technical System Architecture: Conveyor & Storage Racking Integration
A complete Pallet Conveyor Storage System relies on harmonious mechanical and electronic integration between physical racking structures and automated horizontal transfer hardware. Understanding these sub-systems allows procurement engineers to correctly specify equipment based on floor space, floor slab capacity, overhead clearance, and pallet load specs.
Key Components of Integrated Pallet Conveyor Racking Systems:
- Structural Steel Support Framework: Fabricated from high-tensile Q235B or Q355B cold-rolled steel, engineered with teardrop or box-profile uprights, dynamic diagonal bracing, and heavy-duty baseplates.
- Motorized Roller & Chain Conveyor Hubs: Positioned at loading, sorting, and retrieval bays to transfer wooden, plastic, or steel pallets (up to 1,500 kg per pallet position) into the primary storage matrix smoothly.
- Radio Shuttle & 4-Way Transfer Vehicles: Automated battery-powered shuttles running within dedicated channel tracks to pick and place pallets across deep storage lanes automatically.
- Gravity Pallet Flow Roller Tracks: Precision-angled steel roller beds featuring internal speed controllers and safety brake rollers, operating under gravity for strict First-In, First-Out (FIFO) inventory controls.
- Safety Guards & Upright Protectors: Heavy-duty crash barriers, floor-mounted column guards, and side wire mesh enclosures engineered to prevent accidental forklift impacts.
| System Type | Storage Density | Selectivity | Operation Mode | Ideal Application Context |
|---|---|---|---|---|
| Pallet Conveyor + Radio Shuttle | Very High (85%+) | Lane Selective | Automated FIFO / LIFO | Cold Storage, FMCG, Beverage & High-Throughput Distribution |
| Motorized Roller Pallet Flow | High (75-80%) | Strict FIFO | Gravity / Conveyor Driven | Perishable Goods, Pharmaceuticals, Date-Coded Materials |
| Selective Heavy-Duty Pallet Rack | Standard (45-50%) | 100% Direct Access | Manual / Reach Truck | High-SKU Manufacturing, E-commerce, General Warehousing |
| Very Narrow Aisle (VNA) Racking | High (65-70%) | 100% Direct Access | Turret Truck / Guided Forklift | High-Bay Facilities with Limited Footprint Area |
| Push Back Racking System | Medium-High (65%) | LIFO per Lane | Nested Cart Push Mechanism | Medium SKU Count, 2-to-5 Pallet Deep Storage |
4. Future Procurement & Technological Trends (2026–2035)
As global supply chain management transitions towards Smart Industry 4.0 standards, procurement intent is pivoting rapidly from static steel shelving toward intelligent, modular, and green warehouse automation solutions. Buyers seeking competitive advantages in 2026 and beyond must account for these key macro trends:
1. AI-Powered Warehouse Control Systems (WCS) & IoT Telemetry
Modern pallet conveyor systems are no longer standalone mechanical rigs. Modern installations integrate edge IoT sensor arrays, optical barcode scanners, and real-time WCS software. These systems monitor roller bearings, motor temperatures, and shuttle battery health while communicating dynamically with enterprise ERP platforms.
2. Transition to Motorized Driven Roller (MDR) Low-Voltage Technology
Energy efficiency has become a critical procurement matrix. 24V/48V DC Motorized Driven Roller (MDR) pallet conveyor lines are replacing traditional centralized AC drive motors. MDR technology provides zone-controlled zero-pressure accumulation (ZPA), running motors only when a pallet is actively moving through a specific zone. This reduces warehouse energy consumption by up to 60%.
3. High-Density Cold Chain Resilience
With global demand for frozen food and biopharmaceutical distribution soaring, automated radio shuttle racking and stainless steel/galvanized pallet conveyor lines engineered to operate down to -30°C without mechanical freeze-up are experiencing explosive procurement growth.
4. Modular "Plug-and-Play" Pre-Engineered Racking Architectures
Overseas buyers increasingly demand modular racking assemblies that arrive factory-tested with pre-drilled conveyor mounting brackets, standard bolt-together bracing, and snap-in beam connectors. This cuts on-site installation time and local technical labor expenses by up to 40%.
5. Strategic Procurement Framework: Evaluating China Suppliers
Sourcing large-scale warehouse equipment directly from Chinese factories requires rigorous vetting across engineering capability, material quality, production control, and international logistics execution. Use this step-by-step checklist when selecting a manufacturing supplier:
Steel Grade Transparency
Verify that raw materials utilize certified structural steel coils (Q235B or Q355B equivalent to ASTM A36 or SS Grade 50) accompanied by mill test certificates (MTC).
Independent Structural Verification
Ensure the supplier provides Finite Element Analysis (FEA) reports verifying frame deflection under full static and dynamic forklift impact loads.
Export Packaging & Shipping Logistics
Racking frames and long conveyor beds must be packaged with steel-strapped bundles, protective corrugated end-caps, and moisture-proof plastic wrap for container transit.
At PrimeBay Heavy Duty Racking, every system undergoes strict pre-shipment assembly validation, coating thickness testing (minimum 60-80 microns electrostatic powder coat), and dimensional checking to guarantee zero on-site assembly failures.