Featured High-Density Racking & Material Handling Equipment
Select from our precision-engineered heavy-duty storage racks, multi-way shuttles, and electric material handling equipment built for maximum space utilization and operational safety.
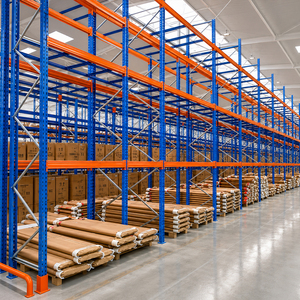
Warehouse Storage Rack System High Density Porta Pallet 1000kg Q235B Cold Rolled Steel Heavy Duty Pallet Rack Warehouse
Get Catalog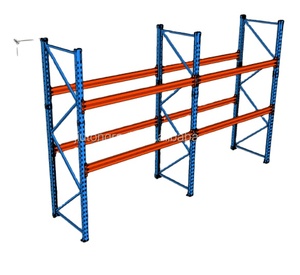
Double Deep Pallet Rack System for Reach Truck High Density Storage Solution for Warehouse
Get Catalog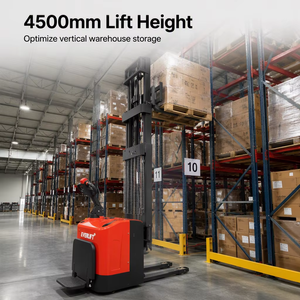
2000kgs Walkie Pallet Stacker Full Electric Advanced DC Drive System Lift Truck Featuring Core Motor Gear Bearing PLC
Get Catalog
Double Deep Pallet Racking High Capacity Storage System Suitable for Reach Truck Forklift Optimize Warehouse Space Utilization
Get Catalog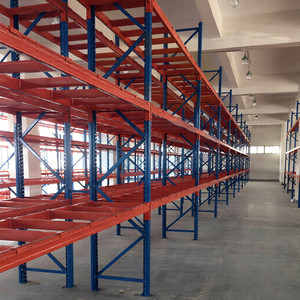
Heavy Duty Steel Pallet Storage Racks Complete Warehouse Pallet Racking Systems Solution Factory Wholesale
Get Catalog
CASE CARTER OEM Powder Coating Heavy Duty Foldable Portable Stacking Steel Tire Storage Rack Palletainer
Get Catalog
Screw Assembly Heavy Duty Pallet Rack Industrial Workshop Storage Cold Rolled Steel Shelving 2000mm Height High Load Capacity
Get Catalog
Factory Price Customized Steel Heavy Duty Warehouse Multi-level Storage Office Platform Mezzanine Floor Rack System
Get CatalogUnderstanding Multi-Way Shuttle Racking Systems: Architecture & Mechanics
In the search for maximum volumetric storage efficiency, traditional selective racking and manual drive-in systems face inherent bottlenecks: high aisle space wastage, elevated forklift collision risks, and limited throughput speed. As modern logistics centers, cold chain hubs, and 3PL facilities face rising land costs, the Multi-Way Shuttle Racking System has emerged as the global benchmark for high-density automated material handling.
Unlike conventional 2-way (radio) shuttle systems that move strictly in linear forward-and-backward vectors along single lanes, a 4-Way Multi-Shuttle System operates dynamically across both longitudinal aisles and transverse cross-tracks. By eliminating the necessity for vertical lifters to manually relocate shuttles between channels, multi-way shuttles autonomously switch directions using integrated hydraulic or servo-driven lifting mechanisms, offering unprecedented flexibility in multi-deep pallet storage environments.
High Yield Strength Steel Profiles
Manufactured using premium Q235B and Q355B cold-rolled steel profiles. Uprights and continuous guide rails undergo automated multi-pass roll forming to ensure dimensional tolerances within ±0.5mm, maintaining absolute alignment for automated shuttle wheel travel.
Smart Fleet Dispatching & WCS
Integrated with Warehouse Control Systems (WCS) and Warehouse Management Systems (WMS) via 5G or Wi-Fi mesh protocols. Intelligent algorithms dynamic-route multiple shuttles across racking layers without path conflicts or bottlenecking.
LiFePO4 Power & Fast Charging
Equipped with ultra-reliable Lithium Iron Phosphate (LiFePO4) power cells or supercapacitors. Automatic online charging stations embedded directly in rack rails deliver 8+ hours of continuous operational cycle from a 30-minute rapid charge.
Future Product Development Trends in Multi-Way Shuttle Systems
As automated storage and retrieval systems (ASRS) rapidly evolve, top Chinese racking manufacturers like PrimeBay Heavy Duty Racking Co., Ltd. are pushing engineering boundaries to deliver next-generation storage solutions. Understanding these technological vectors enables enterprise buyers to make future-proof infrastructure investments.
1. AI-Driven 3D Fleet Optimization & Dynamic Task Allocation
Future multi-way shuttle systems are transitioning from static rule-based PLC routines to AI-powered predictive dispatching. By analyzing historical pick frequencies, seasonal SKU velocity, and real-time order surges, intelligent WCS software dynamically relocates high-turnover pallets to lower levels and aisle intersections, reducing average pallet cycle times by up to 35%.
2. Extreme Cold Chain Adaptation (-30°C Optimization)
With frozen food logistics and pharmaceutical cold chains expanding worldwide, multi-way shuttles are engineered with anti-condensation heated electronic enclosures, low-temperature synthetic lubricants, and cold-resistant polymer drive wheels. This allows uninterrupted performance inside deep-freeze warehouses (-25°C to -30°C) without thermal degradation or battery drain.
3. Ultra-Slim Chassis Engineering & Maximum Vertical Density
Next-gen multi-shuttle vehicles utilize high-torque brushless servo motors integrated directly within wheel hubs. By reducing shuttle height profiles to under 125mm, racking clear clearances per level are reduced, enabling warehouses to squeeze an extra racking tier within standard ceiling heights—maximizing volumetric capacity by an additional 12% to 15%.
4. Modular Hybrid ASRS Integration
Rather than isolating shuttle racking from other automated systems, modern developments fuse 4-way multi-shuttles with Vertical Reciprocating Conveyors (VRC lifters), Autonomous Mobile Robots (AMRs), and AGV forklift fleets. This creates an end-to-end automated material handling matrix from receiving docks to high-bay rack storage and outbound dispatch lanes.
Strategic Global Procurement Trends for Industrial Racking
Sourcing heavy-duty storage racking and automated shuttle systems from leading Chinese manufacturers has evolved from simple unit-price comparisons to strategic long-term risk management and total cost of ownership (TCO) evaluation.
Direct Factory Customization (OEM/ODM)
Global importers and project contractors increasingly bypass middle-man trading distributors to work directly with qualified OEM/ODM factories in China. Direct structural customization allows tailormade upright beam profiles, specialized powder coating formulations (such as anti-microbial or high-durability epoxy), and custom load-bearing baseplates tailored to local seismic zones.
Rigorous Compliance & Structural Audit
International procurement heads now require comprehensive structural testing reports prior to order placement. Tier-1 Chinese suppliers provide verified Finite Element Analysis (FEA) structural simulations, mill test certificates for steel raw materials, and international safety compliance approvals, including CE mark, ISO 9001, ISO 14001, and TUV certificates.
Phased Expansion & Scalable CAPEX
Rather than over-committing upfront capital to rigid full-scale ASRS stacker crane setups, modern procurement favors modular Multi-Way Shuttle systems. Warehouses can install the complete high-density steel racking matrix upfront while deploying only the initial fleet of shuttles needed for present throughput—adding shuttle units seamlessly as order volumes grow.
Industrial Storage System Performance Matrix
Compare key operational parameters across standard selective pallet racking, drive-in systems, 2-way shuttle racks, and advanced 4-way multi-shuttle systems to select the optimal solution for your warehouse facility.
| Racking Architecture | Space Utilization | Pallet Selectivity | Throughput Speed | Forklift Risk | Ideal Application |
|---|---|---|---|---|---|
| Selective Pallet Rack | 40% - 50% | 100% Direct Access | Moderate (Manual) | High Aisle Travel | High-SKU, low-volume distribution |
| Drive-In Pallet System | 65% - 75% | Low (LIFO only) | Slow (Deep Entry) | Severe Frame Collision Risk | Homogeneous bulk goods, low turnover |
| 2-Way Radio Shuttle | 75% - 85% | Moderate (Lane FIFO/LIFO) | Fast (Linear Shuttle) | Low (Aisle Boundary Only) | Cold storage, food & beverage, FMCG |
| 4-Way Multi-Way Shuttle | 85% - 95% | High (Automated 3D Pick) | Ultra-Fast (Multi-Shuttle Fleet) | Zero (Fully Automated ASRS) | High-density automated high-bay fulfillment |
PrimeBay Engineering Strength by the Numbers
Delivering world-class storage solutions backed by advanced structural engineering, certified manufacturing quality, and two decades of global project execution.
Your Trusted Warehouse Racking Manufacturer in China
Established in 2006, PrimeBay Heavy Duty Racking Co., Ltd. is a leading manufacturer of engineered warehouse racking systems operating from our state-of-the-art 40,000 m² production complex in Nanjing, Jiangsu, China. With over two decades of technical dedication, we engineer, manufacture, and supply complete storage systems to importers, distributors, 3PL providers, and industrial clients across 85+ countries worldwide.
In-House Manufacturing Control
Every beam, upright profile, shuttle guide rail, and mezzanine deck is manufactured inside our own factory—from raw steel cold-roll forming to robotic welding and automated electrostatic powder coating. This ensures complete quality control over surface adhesion, coating thickness (60-80 microns), and structural tolerances.
International Certification & 10-Yr Warranty
Our management system and manufactured racking lines strictly comply with international quality benchmarks. PrimeBay holds official certifications for CE, ISO 9001 (Quality Management), ISO 14001 (Environmental Management), and TUV safety standard compliance. All installed systems carry a full 10-year structural warranty.
Full CAD Engineering & OEM Support
Our team of over 300 skilled staff and experienced structural engineers provides complete project lifecycle support. We transform raw building CAD drawings and pallet data into optimized 3D layout designs, FEA load calculation sheets, and detailed installation schematics tailored specifically to your site conditions.
Frequently Asked Questions (FAQ)
Clear engineering and commercial answers to common questions asked by industrial buyers and project contractors.
What is the structural difference between a 2-way radio shuttle and a 4-way multi-way shuttle?
A 2-way radio shuttle moves strictly along a single straight channel (forward and backward). To change lanes or racking levels, a forklift or stacker crane must manually lift the shuttle vehicle. A 4-way multi-way shuttle features dual-wheel drive assemblies that rotate 90 degrees, allowing it to travel longitudinally down storage lanes AND laterally across transfer aisles autonomously without manual forklift relocation.
What warehouse specifications are required for PrimeBay engineers to design a custom racking layout?
To prepare an accurate CAD design and quotation, we require: (1) Warehouse floor plan showing building dimensions, clear height under trusses, column grids, and door locations; (2) Pallet dimensions (Length x Width x Height including cargo); (3) Maximum weight per pallet (e.g., 1000kg); (4) Operating ambient temperature range; and (5) Target hourly throughput (pallets/hour in and out).
Which quality and safety certifications do PrimeBay racking systems carry?
PrimeBay manufacturing processes and finished products are fully certified to CE standards, ISO 9001 (Quality Assurance), ISO 14001 (Environmental Systems), and TUV structural safety testing. Complete documentation, raw material mill certificates, and finite element analysis (FEA) reports are available upon project request.
Can your multi-way shuttle racking systems operate inside cold storage environments?
Yes. PrimeBay offers specialized cold-chain multi-way shuttle systems designed to operate reliably in temperatures down to -30°C. These systems utilize low-temperature synthetic lubricants, anti-condensation circuit board heaters, thermal-isolated sensor housing, and specialized low-temperature LiFePO4 battery cells or supercapacitors.
Does PrimeBay provide OEM and ODM manufacturing services for overseas racking brands?
Yes, we provide extensive OEM and ODM manufacturing services for racking distributors, system integrators, and logistics equipment brands worldwide. We offer custom upright rolling profiles, tailor-made beam connectors, specialized RAL color powder coating, private-label brand packaging, and customized assembly manuals.
What is the standard warranty and after-sales support policy on PrimeBay racking infrastructure?
All PrimeBay heavy-duty steel racking structures carry a comprehensive 10-year product warranty against manufacturing defects when loaded according to engineered design specifications. We provide complete 3D installation drawings, step-by-step assembly videos, and remote or on-site engineering support during project installation.
Optimize Your Warehouse Storage Capacity Today
Send your warehouse drawings, pallet dimensions, and storage requirements directly to our engineering team. We will deliver a customized racking layout, load calculation, and factory-direct quotation within 24 hours.
Get Catalog