Top Counterbalance Forklift Racking Systems
Engineered to withstand heavy dynamic load stress, high aisle turning torques, and deep warehouse stacking requirements.
High Quality Portable Collapsible Steel Selective Pallet Rack with Corrosion Protection 1-5 Ton Capacity
Send an Inquiry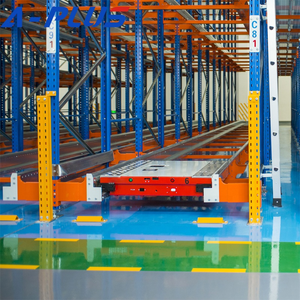
Warehouse Storage Automated Pallet Runner Shuttle Racking System for Counterbalance Drop-off
Send an Inquiry
Wholesale Price 5-Layer Multi-Level Steel Adjustable Heavy Duty Pallet Racking for Counterbalance Warehouses
Send an Inquiry
Electric Pallet Stacker & Counterbalance Truck Heavy High Racking Integrated System
Send an Inquiry
Pallet Shuttle Rack Deep Lane Storage System Optimized for Counterbalance Loading Bays
Send an Inquiry
Heavy Duty Pallet Storage Rack With Side Safety Mesh for Wide Aisle Counterbalance Operations
Send an Inquiry
2000kg Industrial Walkie & Counterbalance Pallet Stacker Racking Infrastructure
Send an Inquiry
Factory Outlet Industrial Heavy-Duty Multi-Level Pallet Racking System for Heavy Counterbalance Lift Trucks
Send an InquiryOptimizing Warehouse Racking Architecture for Counterbalance Forklifts
A comprehensive engineering guide for warehouse directors, 3PL logistics managers, and supply chain procurement officers sourcing heavy-duty racking systems from premier Chinese factories.
1. Understanding Counterbalance Forklift Kinematics and Racking Interactivity
Counterbalance forklifts—whether electric 3-wheel, 4-wheel, or internal combustion (LPG/Diesel) units—are the backbone of material handling across global manufacturing plants and distribution hubs. However, unlike reach trucks, turret trucks (VNA), or articulated forklifts, counterbalanced lift trucks require significantly wider operating aisles (typically ranging from 3.4 to 4.2 meters) and possess heavy outrigger-free front wheel loadings that exert strong dynamic forces on warehouse floor slabs and lower rack levels.
When engineering pallet racking for counterbalance trucks, top Chinese OEM factories like PrimeBay Heavy Duty Racking Co., Ltd. do not simply sell static steel components. We calculate the exact turning radius ($Ast$), overall length of the chassis ($l_2$), load distance ($x$), and total weight distribution ($Q + G$). Our structural engineers design custom upright profiles, heavy-gauge beam connector claws, and reinforced footplates that withstand accidental forklift mast swipes and dynamic stopping impact forces.
Aisle Width Optimization ($Ast$)
We engineer standard selective and high-density racking layouts that maximize pallet positions while giving counterbalance operators 300mm+ of safety buffer beyond the theoretical minimum turning radius.
Structural Impact Armor
Heavy-duty counterbalanced trucks weigh 3 to 6 tons unloaded. We integrate 5mm to 10mm thick cold-formed steel upright guards, wrap-around corner bumpers, and tubular row protectors anchored with M16 chemical bolts.
High-Grade Q355B Steel
Utilizing high-tensile cold-rolled steel coils, our roll-formed upright columns (80/90/100/120/140mm) achieve superior yield strength under heavy structural eccentric compression loads.
2. Racking System Comparison Matrix for Counterbalance Operation
Choosing the right structural racking configuration depends on your stock-keeping unit (SKU) diversity, inventory turnover rate (FIFO vs. LIFO), and warehouse clear ceiling height. Below is an engineering evaluation matrix derived from real project implementation data across 85+ export markets:
| Racking System Type | Counterbalance Aisle Width ($Ast$) | Storage Density Rating | Pallet Selectivity | Impact Protection Needs | Best Industry Application |
|---|---|---|---|---|---|
| Selective Pallet Racking | 3.4m - 3.8m | Standard (40-50%) | 100% Direct Access | Standard Column Guards | High-SKU 3PL, FMCG, General Manufacturing |
| Radio Shuttle Racking | 3.2m - 3.5m (Outer Bay Only) | Ultra-High (80-85%) | Per Lane (FIFO/LIFO) | Heavy Guide Rails at Entry | Cold Storage, Food & Beverage, Bulk Staging |
| Push-Back Rack (Nested Carts) | 3.4m - 3.7m | High (65-75%) | 2 to 6 Pallets Deep / Lane | Front Push-back Rail Bumper | Medium SKU Count, Seasonal Inventory |
| Drive-In Racking System | Truck Drives Inside Rail | High (70-80%) | Strict LIFO / Block Storage | Full Frame Guarding & Ground Rails | Homogeneous Raw Material, Long-term Storage |
| Double-Deep Pallet Rack | 3.6m - 4.0m (Pantry Reach) | Medium-High (60%) | 50% Direct Access | Heavy Duty Base Plates | High-volume Storage with Pantograph Forklifts |
3. Future Trends in Counterbalance Forklift Racking Procurement (2025–2030)
As global supply chains shift toward higher automation, greener manufacturing, and dynamic warehouse management systems (WMS), the procurement of counterbalance forklift racking from China is undergoing four major technological shifts:
A. Autonomous Counterbalance AGV/AMR Integration: Modern distribution centers are transitioning from manually operated counterbalanced trucks to Autonomous Guided Vehicles (AGVs) and Autonomous Mobile Robots (AMRs). Chinese racking manufacturers are now engineering millimetric-precision beam level alignment, laser-reflective targets on rack frames, and integrated floor sensor plates to ensure seamless AGV fork insertion without human margin of error.
B. Ultra-High-Yield Micro-Alloyed Steels: Environmental regulations and rising global freight rates push buyers toward lighter yet stronger structural profiles. Advanced Chinese factories utilize micro-alloyed steels (containing Trace Titanium/Niobium) that increase column buckling resistance by 25% while reducing overall steel shipping weight—translating directly into lower freight cost per pallet position.
C. Intelligent IoT Collision and Structural Strain Sensors: Leading-edge installations now feature smart piezoelectric strain sensors embedded inside critical upright columns and aisle entry barriers. These sensors transmit real-time telemetry to facility managers when a counterbalance forklift strikes a rack frame, alerting maintenance teams to potential structural overload or fatigue before catastrophic rack collapse occurs.
D. Automated Eco-Friendly Powder Coating & Galvanization: Sustainable procurement policies require strict VOC-free finishing process compliance. Premier factories operate fully automated 5-stage pre-treatment coating lines using epoxy-polyester powder formulations that provide 500+ hours of salt spray corrosion resistance—vital for cold storage and humid coastal warehouse environments.
Why Top Global Buyers Choose PrimeBay Racking
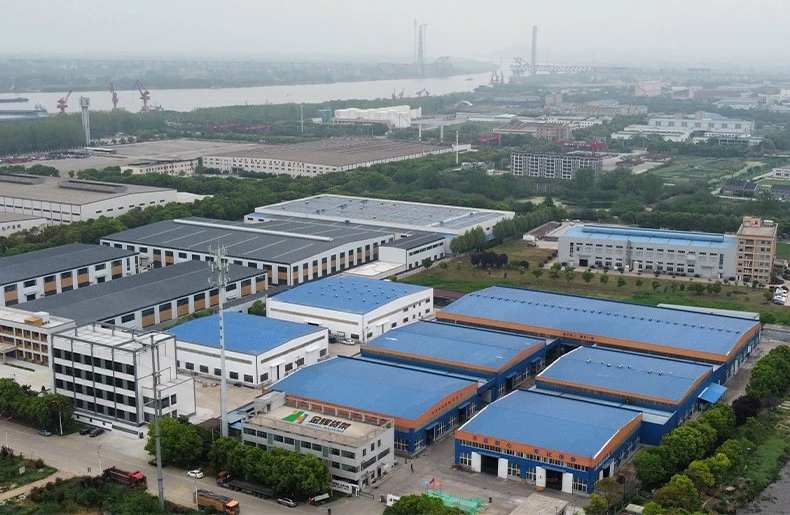
Founded in 2006, PrimeBay Heavy Duty Racking Co., Ltd. operates a modern 40,000 m² manufacturing plant in Nanjing, Jiangsu, China. We specialize in structural steel warehouse equipment exported to over 85 countries worldwide.
- 20+ Years Sourcing Authority: Trusted by multinational 3PLs, project contractors, and OEM racking distributors.
- Certified Structural Integrity: Fully compliant with CE, ISO 9001, ISO 14001, and TUV quality management standards.
- Full Finite Element Analysis (FEA): Every custom design is computer-tested for seismic loads, beam deflection ($L/200$), and wind shear.
- 10-Year Warranty Assurance: Guaranteed long-term structural durability under designed load signage specifications.
Frequently Asked Questions by International Buyers
Clear, direct answers regarding customized manufacturing, engineering validation, freight logistics, and factory direct guarantees.
How do I calculate the required aisle width for my counterbalance forklift?
Aisle width ($Ast$) is calculated as: Turning Radius ($Wa$) + Load Distance ($x$) + Pallet Length ($l$) + Safety Clearance ($a$, minimum 200mm). For standard 2.5-ton counterbalance trucks, typical aisles range from 3,500mm to 3,800mm. Send us your forklift data sheet and our CAD team will plot the precise aisle layout for free.
Can your factory manufacture custom upright profiles and OEM colors?
Yes. PrimeBay offers full OEM and ODM services. We roll-form custom upright profiles (80, 90, 100, 120, 140 series), fabricate specialized beam connectors, and supply electrostatic powder coatings matched to any RAL color code to align with your brand identity or client requirements.
What international structural standards do your racking designs comply with?
Our heavy-duty racking systems are engineered according to FEM 10.2.02 (European Racking Federation), EN 15512, RMI (Rack Manufacturers Institute), and ANSI standards. All raw steel is certified with mill test reports (MTR) for yield stress, tensile strength, and elongation.
How are racking components packed to prevent damage during ocean transit?
Upright frames and beams are bundled with plastic film wrap, heavy steel strapping, and wooden block supports. Small components, box beams, and accessories are stored in reinforced steel wooden crates to prevent scratching, bending, or moisture degradation during long ocean ocean freight shipping.
What protection options exist for lower uprights against forklift collision?
We supply heavy-gauge steel frame protectors, independent anchor-mounted column guards, polymer flexible barriers, and integrated cast-iron corner boots designed to absorb direct kinetic energy from counterbalanced lift trucks without deforming main upright columns.
What is your standard production lead time for full container loads (FCL)?
Our standard manufacturing lead time is 14 to 21 days for 1 to 3 40ft High Cube containers. For large-scale project orders exceeding 10+ containers, we schedule phased production deliveries to match your warehouse installation timeline.
Need a Customized Racking Layout for Your Counterbalance Fleet?
Send us your warehouse CAD drawing, ceiling clear height, pallet dimensions, and forklift specs. Our senior structural engineers will return a complete layout design, load calculation, and factory quote within 24 hours.
Send an Inquiry