High Bay Industrial Racking Portfolio
Explore our export-grade pallet racks, stackers, mezzanines, and automated shuttle storage units
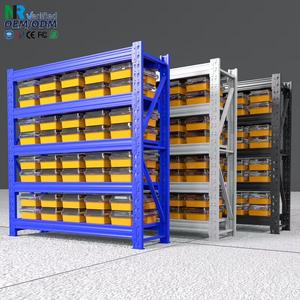
Garage Storage Factory Steel Metal Van Rack System Heavy Duty Shelving Single Deep Industrial Pallet Rack Shelving
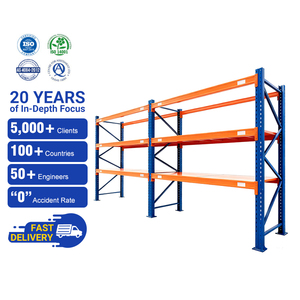
Customized Heavy Duty Industrial Storage Shelves System Metal Rack Stacking Units Warehouse Steel Industrial Pallet Racking
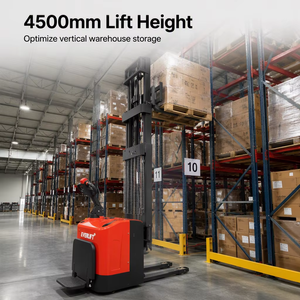
2000kgs Walkie Pallet Stacker Full Electric Advanced DC Drive System Lift Truck Featuring Core Motor Gear Bearing PLC
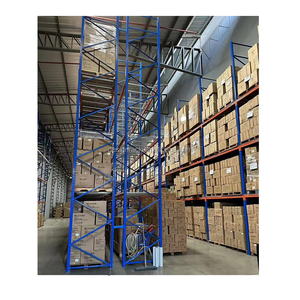
Logistics Center Pallet Rack Warehouse Rack Manufacturer Q235B Steel Heavy Duty Storage Rack Custom Design ISO Certified System
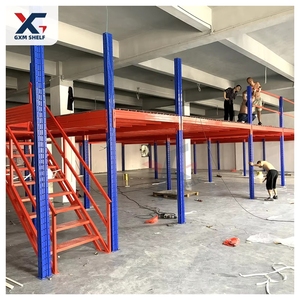
Multi Tier Steel Grating Floor Industrial Mezzanine Platform H Steel Mezzanine Rack System Warehouse Mezzanine Floor System
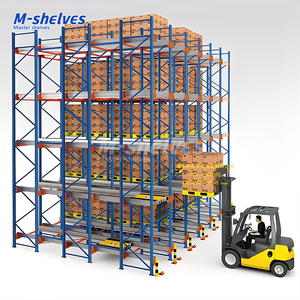
Innovative Auto Shuttle Racking System for Intelligent Cold Storage Steel Pallet Racks Automatic Shuttle Shelving
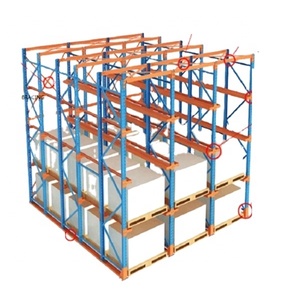
Industrial Steel Products VNA Very Narrow Aisle Selective Pallet Racks Steel Shelves Rack
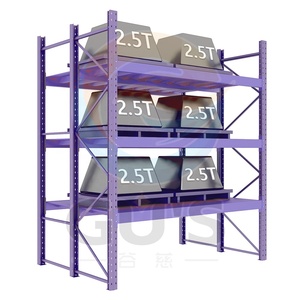
Factory Outlet Industrial Heavy-Duty Multi-Level Pallet Racking System Steel Metal Warehouse Rack with High Storage Capacity
Structural Integrity & Architectural Specifications of CE Certified High Bay Pallet Racking
In modern supply chain architecture, vertical cube utilization has evolved from an operational option into a financial imperative. High bay pallet racking systems—defined as structural steel storage platforms extending from 8 meters to over 40 meters in clear height—demand rigorous mechanical engineering, precise metallurgical selection, and strict compliance with global safety standards. As a premier CE-certified high bay pallet racking manufacturer and direct global exporter, PrimeBay Heavy Duty Racking Co., Ltd. delivers engineered racking infrastructure designed to withstand complex static, dynamic, and seismic loads.
Every high bay racking solution engineered within our 40,000 m² manufacturing plant in Nanjing utilizes certified Q235B and Q355B structural grade cold-rolled steel. Our structural calculations adhere to European standard EN 15512 (Steel static storage systems - Adjustable pallet racking systems - Principles for structural design) and FEM 10.2.02 guidelines. By incorporating Finite Element Analysis (FEA) into the preliminary design phase, our engineering team ensures optimized upright profile geometries, beam profile section moduli, and sway bracing configurations that guarantee maximum structural stability under full payload capacities up to 4,500 kg per beam level.
Key Compliance & Integrity Standard: EN 15512:2020
European norm EN 15512 requires rigorous limit state structural calculations accounting for global frame imperfections, beam-to-upright connection stiffness (Kd curves), floor slab elasticity, and secondary bending moments (P-Delta effect). PrimeBay racking structures undergo physical testing for beam end-connector teardrop lock shear, baseplate anchor tension, and cold-formed column compression buckling to ensure compliance with European Machinery Directive 2006/42/EC and CE marking standards.
High Bay Storage Systems Performance Matrix
Selecting the optimal high bay racking configuration requires evaluating throughput requirements against capital expenditure (CAPEX), spatial efficiency, and material handling equipment (MHE) compatibility.
| Racking System Type | Max Operational Height | Pallet Selectivity | Volumetric Efficiency | MHE Interface | Ideal Industry Application |
|---|---|---|---|---|---|
| Selective High Bay Racks | Up to 12 Meters | 100% Direct Access | 40% – 50% | Reach Trucks / Counterbalance | High-SKU Retail Distribution & 3PL Logistics |
| VNA (Very Narrow Aisle) Racks | Up to 18 Meters | 100% Direct Access | 65% – 75% | VNA Turret Trucks / Wire-Guided AGVs | Pharmaceuticals, Spare Parts & FMCG Hubs |
| Radio Shuttle High Bay System | Up to 25 Meters | LIFO / FIFO Lane-Based | 80% – 90% | Automated Radio Shuttle + Forklift | Cold Storage, Food & Beverage Mass Palletizing |
| Four-Way Shuttle High Bay ASRS | Up to 40 Meters | Fully Automated Matrix | 85% – 95% | 4-Way Shuttle + Vertical Lift Reciprocator | Automated Cold Chains & Smart Factories |
| Multi-Tier Mezzanine Platform Racks | Up to 14 Meters (Multi-Level) | Manual / Conveyor Access | 200% – 300% Floor Area | VNA Stacker / Goods Lifts / Elevators | E-commerce Order Picking & Apparel Warehousing |
Engineering Innovation & Manufacturing Capabilities
Cold-Formed Profile Precision
Continuous 22-stage automated roll-forming lines craft column profiles with up to 13 bending ribs, maximizing moment of inertia ($I_x, I_y$) and resistance to torsional buckling.
Electrostatic Powder Coating
Thermosetting epoxy-polyester powder coating cured at 200°C creates an 80–110 μm thick anti-corrosion barrier passing 1000-hour salt spray testing (ISO 9227 compliant).
Seismic Engineering & FEA
Engineered using finite element modeling to withstand seismic spectral accelerations up to Zone 4 (USGS/RMI compliant), preventing dynamic structural collapse.
Future Procurement Trends in High Bay Pallet Racking (2025–2030)
As global supply chains face volatile labor availability, rising land costs, and net-zero sustainability mandates, industrial racking procurement is undergoing a fundamental shift. Procurement managers, logistics engineers, and warehouse developers must align their structural investments with long-term technological and economic trends.
1. Convergence of High Bay Racking with Automated Shuttle & ASRS Infrastructure
Traditional static racking is increasingly giving way to hybrid automated systems. Future high bay projects are prioritizing Pallet Shuttle Integration and Four-Way Matrix Systems. Rather than dedicating up to 60% of warehouse floor space to operator forklift aisles, automated high bay structures utilize internal robotic shuttles running on embedded precision rails. This transition increases pallet density by 80% while reducing energy expenditure per pallet position—a critical factor for temperature-controlled facilities.
2. Cold Storage Energy Density & Thermal Optimization
With the rapid expansion of global cold chain logistics for frozen foods and biopharmaceuticals, high bay racking must perform flawlessly under extreme temperature environments down to -30°C. Future procurement favors cold-resistant micro-alloyed steels (such as Q355ND grade steel with low-temperature impact toughness guaranteed down to -40°C) and specialized low-temperature powder coatings that prevent micro-fracturing and paint delamination under thermal contraction stress.
3. Standardized Modular Prefabrication & Fast-Track Global Deployment
Global EPC contractors and logistics REITs require rapid commissioning timelines. Standardized cold-formed components—featuring self-locking teardrop or beam-to-frame connector locks with safety locking pins—allow rapid boltless assembly without on-site field welding. Modern high bay racking procurement demands off-site pre-engineered components packed into seaworthy containerized modules with step-by-step CAD elevation guides for zero-error installation by local crews.
4. Carbon Footprint Transparency & Green Steel Sourcing
In compliance with European Carbon Border Adjustment Mechanism (CBAM) regulations and corporate ESG mandates, tier-1 racking manufacturers must supply verified Environmental Product Declarations (EPDs). Procurement contracts increasingly stipulate the use of steel produced via Electric Arc Furnace (EAF) powered by renewable energy, reducing embedded carbon emissions per structural tonne by up to 45%.
Why Direct Importers & Contractors Choose PrimeBay Heavy Duty Racking
As a direct factory manufacturer located in Nanjing, China, PrimeBay Heavy Duty Racking Co., Ltd. controls the complete supply chain from raw coil slitting, automatic stamping, continuous roll-forming, robotic welding, and shot blasting to automated powder coating and customized export packaging.
Full OEM & ODM Customization
We manufacture custom upright profile widths (80mm to 140mm), column gauge thicknesses (1.5mm to 3.0mm), custom powder coating RAL colors, and branded packaging for regional racking distributors and systems integrators.
CE & TUV Certified Production
Our plant strictly complies with ISO 9001 (Quality Management) and ISO 14001 (Environmental Management). Product load limits are independently certified by TUV Rheinland and carrying full CE certificate documentation.
Comprehensive Engineering Support
Our 30+ engineering design team provides complete DWG/CAD warehouse layout drawings, structural deflection calculations, floor anchor load reaction schedules, and structural load signage with every quote.
Frequently Asked Questions (High Bay Pallet Racking Procurement)
Detailed technical and commercial answers to common engineering questions raised by international buyers, facility managers, and logistics contractors.
Ready to Optimize Your High Bay Storage Infrastructure?
Contact our senior engineering team today to receive CAD layout design drawings, structural calculations, and direct factory pricing within 24 hours.
Get Catalog