Featured Industrial Pallet Racking & Storage Systems
Explore our core CE-certified structural steel pallet racking systems engineered for maximum space utilization, heavy load dynamics, and seamless automation integration.
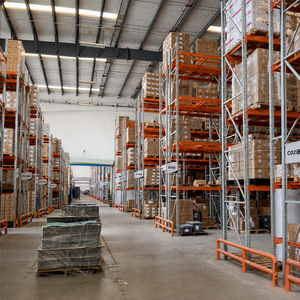
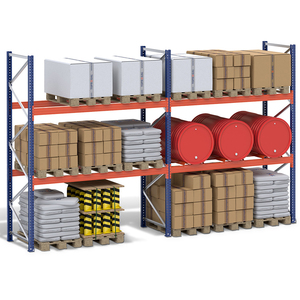
Engineering Excellence & Manufacturing Capability
PrimeBay Heavy Duty Racking Co., Ltd. (Established 2006) — China's Premier CE-Certified Pallet Storage System Manufacturer.
20+ Years Expertise
Founded in 2006, our engineering teams have pioneered high-density static and automated pallet racking systems, deploying custom storage projects across more than 85 countries worldwide.
Rigorous Certifications
Fully compliant with international structural integrity standards. Production facilities operating under CE, ISO 9001, ISO 14001, and verified by TUV Rheinland safety audits.
40,000 m² Advanced Plant
Located in Nanjing, Jiangsu, our state-of-the-art facility integrates automated continuous cold-roll forming, robotic laser cutting, continuous powder coating, and FEA testing laboratories.
System Architecture: Automated vs. Semi-Automated Pallet Storage
A structural engineering comparison designed to help supply chain directors evaluate volumetric efficiency, throughput speed, and total cost of ownership (TCO).
1. Radio Shuttle & 4-Way Intelligent Pallet Shuttle Systems
Automated shuttle racking systems represent the pinnacle of high-density storage technology. By employing autonomous battery-powered shuttles running on specialized guide rails beneath pallet positions, warehouse operators eliminate forklift access aisles entirely within the main rack matrix.
Our CE-certified 4-Way Shuttle Racking utilizes intelligent swarm control software, enabling shuttles to move laterally and longitudinally across deep-lane structures. This increases overall volumetric cube utilization by up to 85% compared to traditional selective racking while dramatically reducing operational cycle times and forklift maintenance overhead.
2. Automated Storage and Retrieval Systems (ASRS)
ASRS combines structural cold-rolled high-bay racking with automated stacker cranes (SRMs) or shuttle lifts capable of vertical execution reaching heights upwards of 40 meters. Integrated with warehouse control systems (WCS) and enterprise WMS, ASRS delivers 24/7 continuous operation with zero manual handling errors, ideal for high-throughput fulfillment hubs and cold storage environments operating at -25°C.
3. Dynamic Gravity Pallet Flow & Heavy-Duty Push-Back Racks
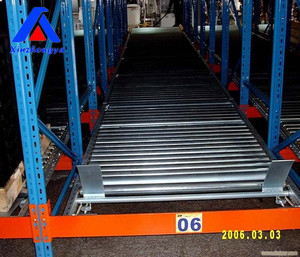
For operations requiring strictly enforced First-In, First-Out (FIFO) stock rotation—such as perishable food processing and pharmaceutical distribution—Gravity Pallet Flow Racking employs inclined roller tracks with speed-braking rollers and safety separators. Alternatively, Push-Back Racks offer high-density Last-In, First-Out (LIFO) storage utilizing nested carts on inclined rails, providing rapid access for 2-to-5-deep pallet configurations without forcing trucks inside rack lanes.
Engineering Selection & Performance Matrix
| Storage System Type | Volumetric Density | Pallet Access / Selectivity | Stock Rotation Logic | Max Load Capacity / Pallet | Automation Readiness |
|---|---|---|---|---|---|
| 4-Way Automated Shuttle | Maximum (85%+) | Lane-Based Automated | FIFO or LIFO Dynamic | 1,500 kg | Fully Automated (WCS/WMS) |
| 2-Way Radio Shuttle Rack | Very High (75-80%) | Deep-Lane Batch Access | FIFO or LIFO | 2,000 kg | Semi-Automated (RF Remote) |
| High-Bay ASRS Crane System | Maximum (Vertical) | 100% Direct Computer Control | Strict FIFO Software Controlled | 3,000 kg | Fully Automated Stacker Crane |
| Pallet Gravity Flow Rack | High (65-75%) | Dedicated Entry/Exit Lanes | Strict Mechanical FIFO | 1,200 kg | Passive Gravity Dynamic |
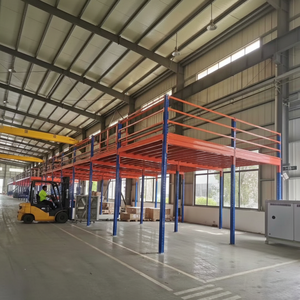
| Multi-Tier Mezzanine Platform | Medium (Multi-Floor) | 100% Manual / Conveyor Access | Flexible / Selective | 1,000 kg / m² (Deck Load) | Conveyor & Goods Lift Ready |
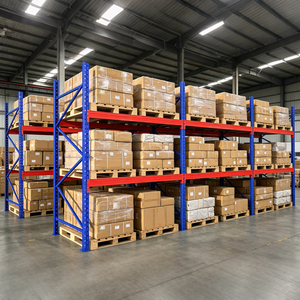
| Heavy Duty Selective Rack | Standard (40-50%) | 100% Immediate Direct Access | Any Rotation Strategy | 5,000 kg / Beam Level | Forklift / VNA Manual Operator |
Future Procurement Trends in Automated Pallet Storage (2025–2030)
Strategic foresights for industrial buyers, procurement managers, and logistics consultants preparing for next-generation automated warehousing.
1. Convergence of AGV/AMR with Shuttle Platforms
Procurement teams are shifting away from isolated storage equipment toward end-to-end autonomous ecosystems. Modern shuttle installations are designed with dock-to-rack integration where Autonomous Mobile Robots (AMRs) transfer pallets directly from unloading bays to shuttle elevators without human touch points.
2. Sub-Zero Cold Chain Energy Efficiency
With global cold chain operational costs soaring, high-density shuttle racking installed in cold storage facilities (-25°C to -30°C) reduces refrigerated room cubic volume requirements by up to 60%. Smaller thermal envelopes significantly decrease kilowatt-hour energy consumption, providing a compelling payback period (ROI) within 18 to 24 months.
3. Modular Structural Steel & ESG Standards
Enterprise procurement mandates increasingly focus on carbon footprint and steel traceability. PrimeBay utilizes high-tensile cold-rolled steel profiles (Q235B and Q355B grades) optimized via Finite Element Analysis (FEA) to reduce structural steel deadweight while guaranteeing safety factors exceeding EN 15512 standards.
4. Cloud WCS APIs & Real-Time Telemetry
Future automated racking solutions require onboard IoT sensors monitoring vibration, battery health, thermal fluctuation, and rack structural stress. PrimeBay automated shuttle platforms natively communicate with cloud-based WMS/WCS software over industrial Wi-Fi or 5G private networks for real-time predictive maintenance.
Automated Storage Industry Evolution & Structural Safety Standards
How rigorous European & Global structural certifications protect multi-million dollar logistics investments.
CE Certification & EN 15512 Compliance
Structural pallet racking is classified as industrial load-bearing steelwork. CE certification guarantees that PrimeBay racking systems meet rigorous European structural engineering codes (EN 15512, EN 15620, FEM 10.2.02). This covers global load factors, lateral displacement limits, frame stability calculations, and beam-to-upright connector safety lock mechanics.
Seismic Design & Dynamic Load Resiliency
Modern warehouse sites in seismic zones require dynamic calculation models. PrimeBay engineers design customized heavy-duty rack structures equipped with floor anchor baseplates, back bracing, and top tie-beams engineered to absorb lateral seismic forces up to Zone 4 spectrum levels without structural collapse.
Anti-Corrosion Surface Finishing
Corrosive industrial environments—such as chemical storage, fertilizer hubs, and coastal port warehouses—demand superior surface protection. PrimeBay implements automated multi-stage pre-treatment wash cycles followed by electrostatic epoxy-polyester powder coating (60-80μm thickness) or hot-dip galvanizing for ultimate rust protection.
Procurement & Technical FAQ
In-depth answers to critical technical, structural, and international export questions raised by global supply chain buyers.
1. What specific parameters are verified for CE certification in automated pallet storage systems?
CE certification for racking systems requires compliance with European Standard EN 15512: Steel static storage systems - Adjustable pallet racking systems - Principles for structural design. This ensures rigorous verification of material mechanical properties (yield strength, tensile resistance), finite element analysis (FEA) modeling under maximum static and dynamic loads, structural safety factors for frame buckling, connection stiffness tests between beam hooks and upright perforations, and compliance with strict dimensional tolerances to ensure safe automated shuttle travel.
2. How does Radio Shuttle Racking compare against Traditional Drive-In Racking regarding ROI?
While Drive-In racking has a lower upfront component cost, it forces forklift operators to drive physically inside the narrow steel structure, leading to high collision damage, slow pallet handling speeds, and higher safety risks. Radio Shuttle Racking moves pallets automatically inside deep channels via remote control or WCS. This eliminates rack damage by keeping forklifts outside the matrix, reduces pallet handling cycles by 40-50%, increases floor storage density, and typically delivers a complete return on investment (ROI) within 12 to 18 months through labor and maintenance savings.
3. What building ceiling height and floor slab requirements are required for automated shuttle storage?
Automated shuttle systems can be customized for building heights ranging from 4 meters up to 25 meters. Standard concrete floor slab requirements stipulate a minimum concrete grade of C25/C30 with a slab thickness of 150mm to 250mm, capable of bearing point load reactions generated by concentrated upright loads. The floor flatness must adhere to DIN 18202 or VDMA guidelines (e.g., FM2 or superflat classifications for narrow aisle systems) to ensure smooth shuttle travel and rack alignment.
4. Can PrimeBay customize pallet racking systems for sub-zero cold storage operations?
Yes. PrimeBay specializes in engineered sub-zero cold storage racking systems operating at temperatures as low as -30°C. For low-temperature environments, we utilize specialized steel grades (such as Q355D/E with proven low-temperature impact toughness to prevent cold embrittlement), specialized sub-zero powder coatings, and cold-rated lithium-ion battery packs equipped with internal heating elements for continuous shuttle operation in freezer warehouses.
5. What is the typical project workflow from initial CAD drawing to final installation support?
Our turnkey engineering process follows four structured phases:
Phase 1 (Data & Requirements): We review your warehouse CAD drawing, pallet dimensions, unit load weight, forklift specifications, and required hourly pallet throughput.
Phase 2 (Engineering & Simulation): Our structural engineers prepare a comprehensive 2D/3D layout, FEA structural calculation report, and bill of materials (BOM).
Phase 3 (Precision Manufacturing): Production at our 40,000m² factory under ISO 9001 control with strict raw material testing and automated powder coating.
Phase 4 (Global Export & Commissioning): Secure sea-freight packing, supply of detailed assembly drawings, installation manuals, video guides, or on-site engineering supervision.
6. What structural safety features are built into PrimeBay Heavy-Duty Pallet Racks?
Every PrimeBay system incorporates multi-layered safety hardware: heavy-gauge steel upright protectors and row end guardrails to absorb forklift impacts, spring-loaded safety locks on every beam connector to prevent accidental dislodgement during loading, mesh decking or pallet support bars for un-palletized loads, frame back-bracing systems, and certified capacity warning signage mounted prominently on every rack row.
7. Does PrimeBay provide OEM & ODM services for industrial distributors and contractors?
Yes. As a direct manufacturer, we provide full OEM and ODM services for global warehouse equipment distributors, rack brand owners, and EPC engineering contractors. This includes custom upright profile roll-forming, specialized beam connectors matching existing installations, custom RAL color powder coating, private label branding, custom packaging, and direct container drop-shipping.
8. How does PrimeBay guarantee load-bearing capacity ratings over a 10-year period?
Every load rating provided by PrimeBay is backed by physical laboratory destruct-testing and FEA structural calculation software compliant with international standards (EN 15512, RMI, FEM). We issue a formal 10-Year Structural Warranty with certified load charts stamped by structural engineers, ensuring that when operated within designated load limits, structural integrity remains uncompromised.
Accelerate Your Warehouse Capacity & Automation Today
Send your warehouse floor plan, ceiling clearance, and pallet load specifications to PrimeBay's structural engineering team. Receive a free CAD layout, load calculation, and factory-direct quotation within 24 hours.